Positive pressure dilute phase pneumatic conveying systems represent a sophisticated method for transporting dry bulk materials through a pipeline network. These systems leverage compressed air to suspend and move material particles, offering a flexible and efficient solution for industries requiring reliable material handling. Common applications include the food, pharmaceutical, chemical, and mineral processing sectors, where maintaining product purity and minimizing contamination are critical. The technology’s ability to handle a wide range of materials, from fine powders to granules, and transport them over long distances makes it a preferred choice for many industrial operations.
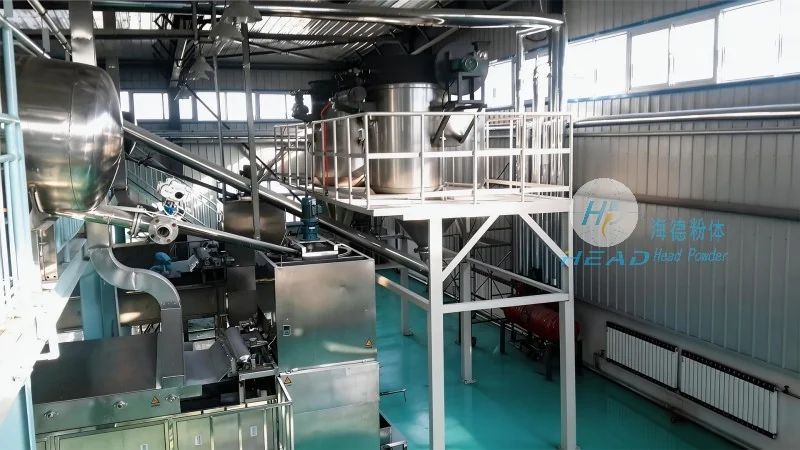
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a prominent manufacturer and supplier of pneumatic conveying equipment. The company is dedicated to delivering high-quality, customized solutions for material transport challenges. With a strong commitment to innovation and customer satisfaction, HeadPowder has built a reputation for excellence in the industry. The company’s expertise lies in designing and manufacturing positive pressure dilute phase systems that meet the specific requirements of clients, ensuring optimal performance and durability.
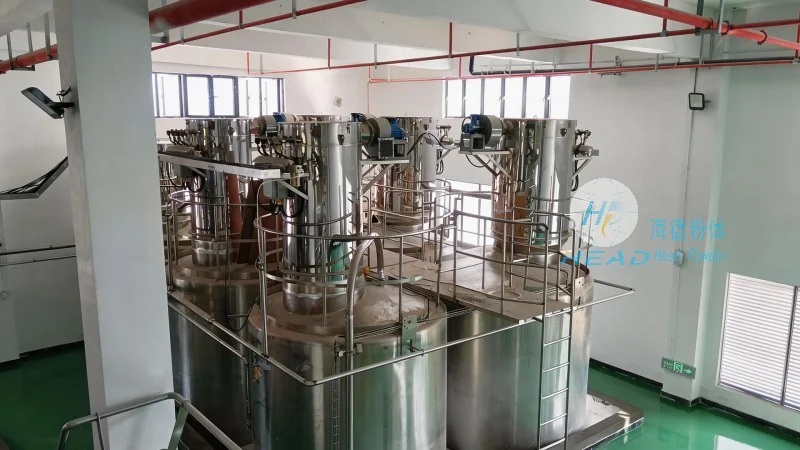
Structural Principles of Positive Pressure Dilute Phase Systems
The fundamental components of a positive pressure dilute phase pneumatic conveying system include a blower or compressor, a material hopper, a feeder, a pipeline network, and a receiver. The blower generates the necessary air pressure and volume to create a positive pressure environment within the pipeline, which propels the material particles suspended in the air stream. The hopper serves as the storage vessel for the bulk material, while the feeder (often a rotary valve or screw feeder) controls the flow rate of material into the system, preventing overloading and ensuring consistent transport. The pipeline system, typically made of stainless steel or other corrosion-resistant materials, connects the hopper to the receiver, with appropriate fittings and valves to regulate the direction and pressure of the air and material flow. The receiver collects the conveyed material and may incorporate a dust collection system to maintain environmental compliance and product cleanliness.
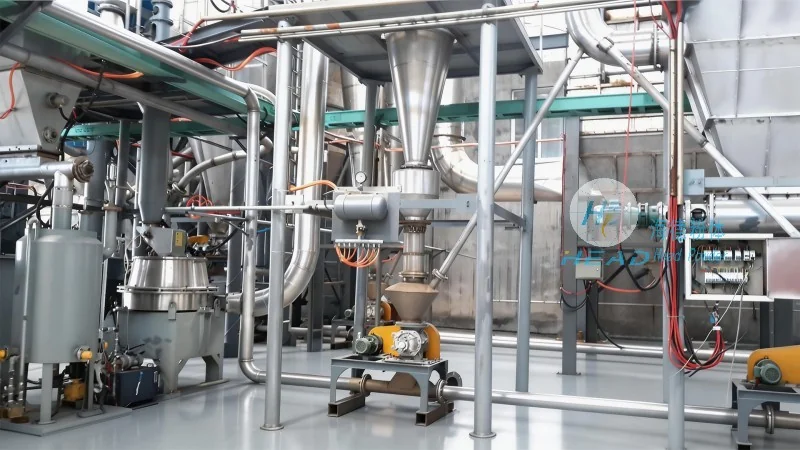
Key Advantages of Positive Pressure Dilute Phase Conveying
Positive pressure dilute phase systems offer several advantages over traditional material handling methods. These include the ability to transport materials over long distances with minimal energy consumption, reduced product degradation due to gentle handling, and enhanced safety by eliminating the need for manual handling. Additionally, the system’s flexibility allows for easy integration into existing production lines and the ability to handle a variety of materials without the need for extensive modifications. The positive pressure design also ensures that air and material are continuously moving, preventing material buildup and reducing the risk of clogging in the pipeline.
Application Examples and Industries
Positive pressure dilute phase pneumatic conveying systems are widely used across various industries. In the food industry, they are employed for transporting ingredients like flour, sugar, and spices, ensuring hygienic and contamination-free handling. The pharmaceutical sector utilizes these systems for conveying active pharmaceutical ingredients (APIs) and other sensitive materials, maintaining strict quality control standards. In the chemical industry, the technology is used for transporting powders such as pigments, catalysts, and reagents, where precise control over material flow is essential. The mineral processing industry also benefits from these systems for handling raw materials like ores and minerals, enabling efficient and cost-effective transport from processing plants to storage or further processing facilities.
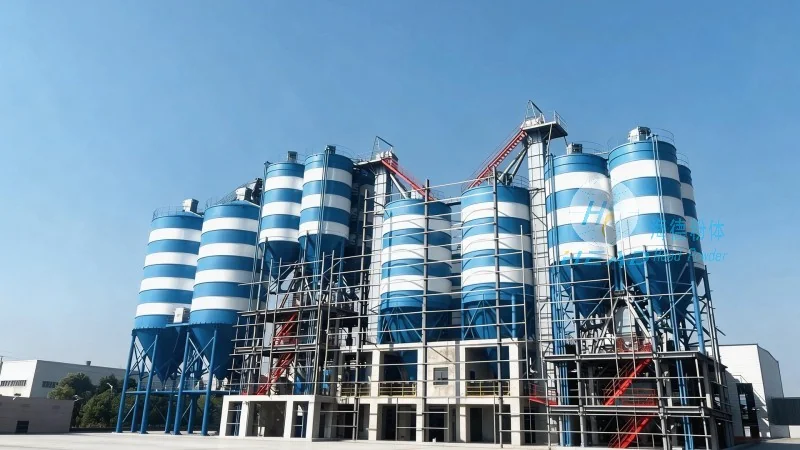
Conclusion
Positive pressure dilute phase pneumatic conveying systems are a reliable and efficient solution for material handling in modern industrial applications. With their ability to maintain product integrity, minimize contamination, and offer flexible operation, these systems provide significant benefits to industries that rely on bulk material transport. Shandong HeadPowder Engineering Co., Ltd. continues to lead in the development and manufacturing of such systems, ensuring that clients receive high-quality equipment tailored to their specific needs. By leveraging advanced technology and a commitment to quality, HeadPowder remains a trusted partner in the material handling industry.




