Continuous quantitative pneumatic conveying equipment is a specialized industrial device designed for the efficient and precise transport of bulk materials over long distances. This equipment is widely used in various industries, including food processing, pharmaceuticals, chemicals, and mining, where the need for accurate material handling and minimal product contamination is critical. The system operates by using a combination of air pressure and mechanical components to move powders or granules from a source to a destination, ensuring consistent flow rates and maintaining product integrity throughout the process.
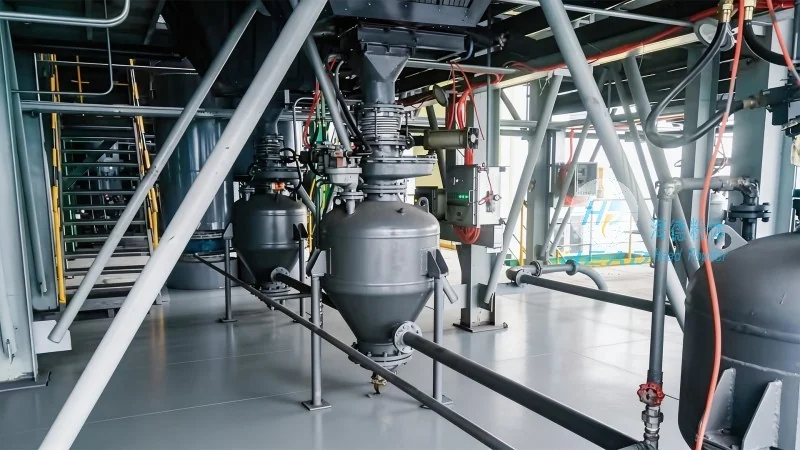
Overview of Continuous Quantitative Pneumatic Conveying Systems
At the core of continuous quantitative pneumatic conveying is the ability to deliver a precise, controlled volume of material. This is achieved through a series of integrated components that work in harmony to ensure reliable operation. The system typically includes a feeding unit, a conveying pipeline, a separation system, and a discharge mechanism. Each component is engineered to optimize performance, minimizing downtime and maximizing efficiency.
Structural Components and Working Principles
The structural design of continuous quantitative pneumatic conveying equipment is tailored to handle different material characteristics and operational requirements. The feeding unit, often equipped with a rotary valve or screw feeder, ensures a steady and controlled supply of material into the conveying pipeline. The pipeline itself is usually made of stainless steel or other corrosion-resistant materials, designed to withstand the pressures and temperatures associated with the conveying process. The conveying mechanism relies on compressed air, which is introduced into the pipeline to create a flow that propels the material forward. The air velocity and pressure are carefully regulated to maintain a consistent material concentration, preventing clogging and ensuring smooth transport.
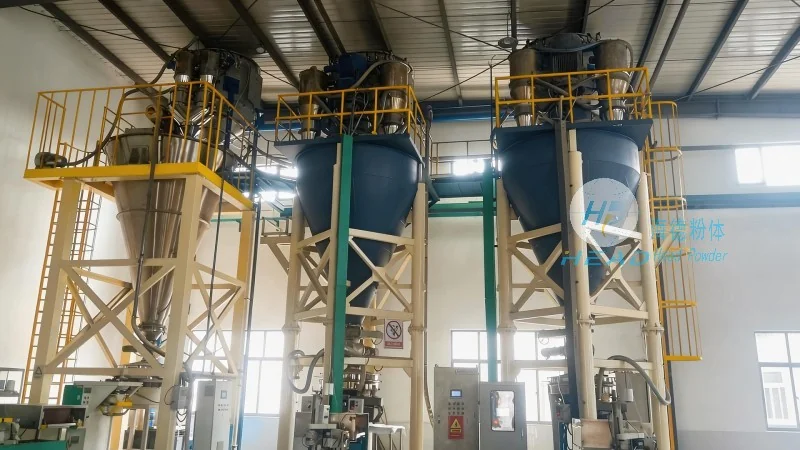
Key Features and Advantages
Continuous quantitative pneumatic conveying systems offer several advantages over traditional bulk handling methods. One of the primary benefits is the ability to handle a wide range of materials, from fine powders to coarse granules, without the need for additional processing steps. The system is also highly flexible, allowing for changes in material type or flow rate without significant modifications. Additionally, the enclosed design minimizes dust emissions and product contamination, making it suitable for applications where hygiene and environmental compliance are paramount. The quantitative nature of the system ensures accurate inventory management and reduces waste, contributing to cost savings and improved operational efficiency.
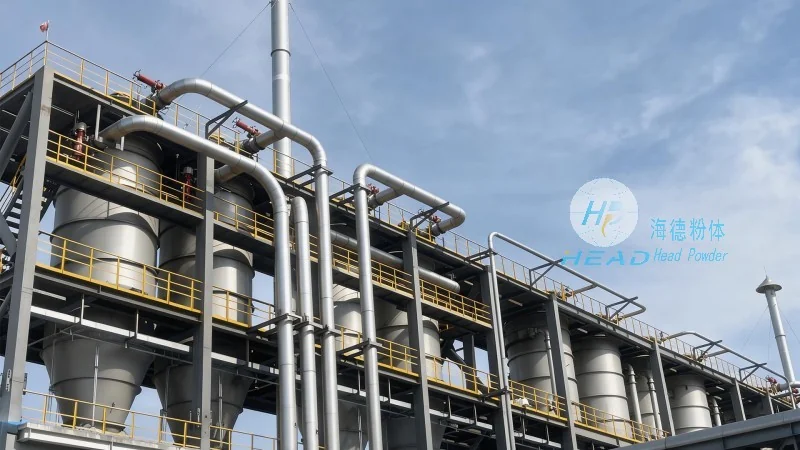
Application Scenarios
Continuous quantitative pneumatic conveying equipment is employed in diverse industrial settings. In the food industry, it is used to transport ingredients such as flour, sugar, and spices from storage to production lines, maintaining product freshness and preventing cross-contamination. In the pharmaceutical sector, the system is critical for handling active pharmaceutical ingredients (APIs) and excipients, where precision and sterility are non-negotiable. The chemical industry utilizes these systems for transporting powders like catalysts, pigments, and specialty chemicals, ensuring consistent quality and reducing handling errors. In mining and mineral processing, the equipment is used to move raw materials from processing plants to storage facilities, optimizing material flow and reducing labor costs.
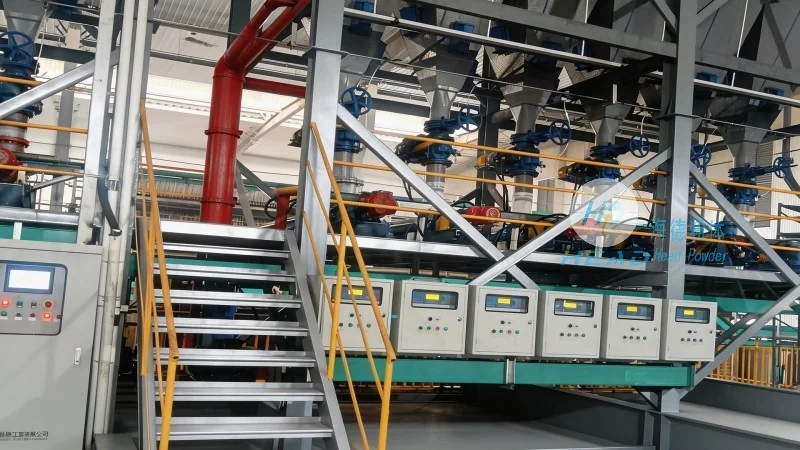
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer of pneumatic conveying systems and related industrial equipment. With a strong focus on innovation and quality, the company has established itself as a trusted partner for businesses seeking reliable and efficient material handling solutions. Headpowder's products are designed to meet the specific needs of various industries, combining advanced technology with robust construction to deliver long-lasting performance. The company's commitment to customer satisfaction and technical excellence has earned it a reputation for delivering high-quality equipment that meets international standards.
Location and Contact Information
Headpowder is headquartered in Shandong, China, a region known for its robust industrial infrastructure and manufacturing capabilities. The company's facilities are equipped with state-of-the-art production lines and testing equipment, ensuring that each product meets the highest standards of quality and reliability. By leveraging local expertise and resources, headpowder is able to provide competitive pricing and efficient delivery times, making it an attractive choice for businesses worldwide.




