Multi-hopper pneumatic conveying systems are advanced industrial equipment designed to efficiently transport bulk materials over long distances or within complex processing facilities. These systems are widely used in various industries, including chemical, food, pharmaceutical, and mining, due to their ability to handle a wide range of materials with minimal product degradation. The core of such systems lies in the multi-hopper design, which allows for the sequential or simultaneous feeding of different materials, enhancing operational flexibility and throughput.
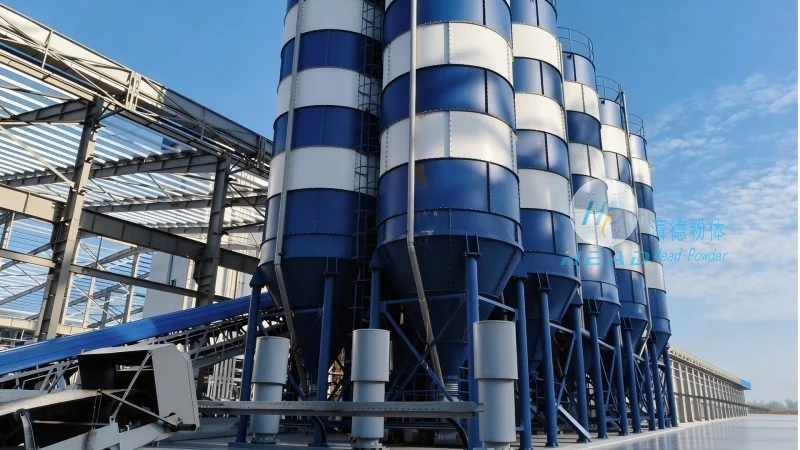
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, manufacturing, and supply of high-quality multi-hopper pneumatic conveying systems. With a strong commitment to engineering excellence and customer satisfaction, the company has established itself as a trusted partner in the industry. The company’s facilities are strategically located in Shandong, providing a robust operational base for research, development, and production.
Key Components and Structural Design
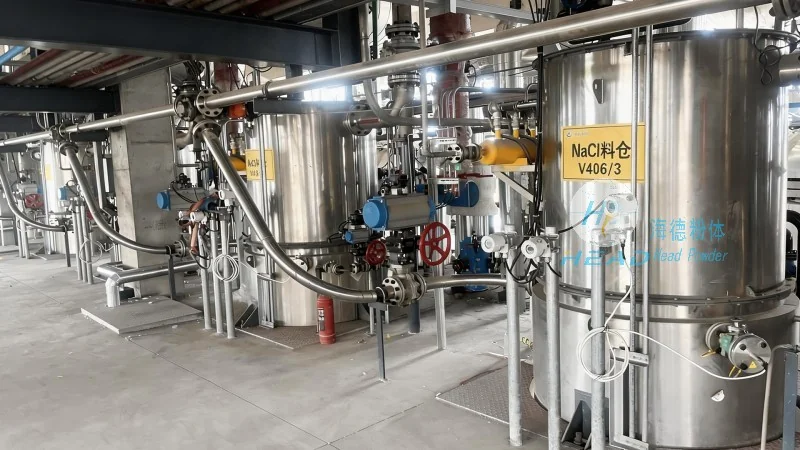
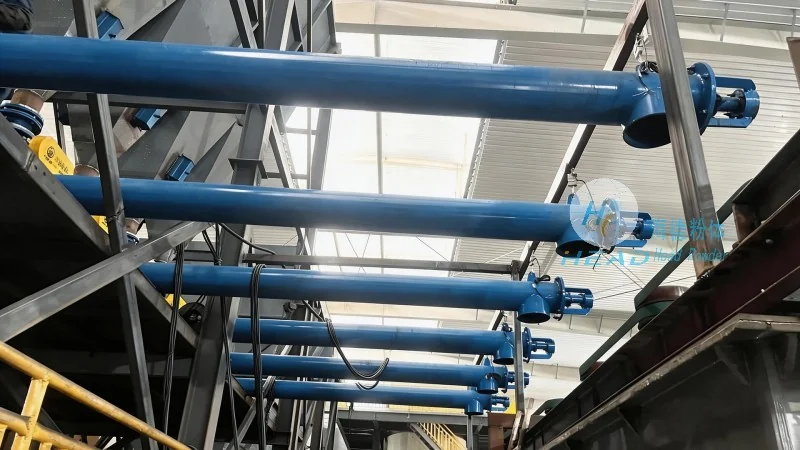
The multi-hopper pneumatic conveying system typically consists of several critical components that work in harmony to ensure smooth material handling. The primary components include the hoppers, which serve as storage and feeding units; the conveying lines, which transport the material through a pressurized or vacuum environment; and the control system, which regulates the flow and pressure to maintain optimal operation. Each hopper is equipped with a feeding mechanism, such as a rotary valve or a slide gate, that controls the discharge of material into the conveying line.
The structural design of these systems is engineered to withstand the pressures and stresses associated with pneumatic conveying. The hoppers are usually made from durable materials like stainless steel or carbon steel, ensuring resistance to corrosion and wear. The conveying lines are often constructed from flexible or rigid tubing, depending on the application, and are fitted with appropriate fittings and valves to manage the flow of air and material. The control system, which may include sensors, controllers, and actuators, provides real-time monitoring and adjustment of the system parameters, ensuring consistent performance and preventing operational issues.
Working Principle of the System
The operation of a multi-hopper pneumatic conveying system is based on the principles of pneumatic transport, where materials are moved by the force of compressed air or vacuum. The process begins with the material being loaded into the hoppers. Each hopper is then sequentially or simultaneously activated, allowing the material to be discharged into the conveying line. The air, either supplied by a blower or generated by a vacuum pump, is introduced into the line, creating a flow that propels the material forward. The speed and pressure of the air are carefully controlled to ensure that the material is conveyed efficiently without causing excessive wear or degradation.
During the conveying process, the material is suspended in the air stream and transported through the system. The design of the conveying lines, including bends and transitions, is optimized to minimize pressure loss and maintain the material's integrity. The system may also include features such as cyclones or filters to separate the material from the air at the discharge end, ensuring that the material is delivered to the target location in a clean and controlled manner. The control system continuously monitors the pressure, flow rate, and material level, adjusting the air supply and feeding rates as needed to maintain stable operation and maximize throughput.
Advantages and Applications
Multi-hopper pneumatic conveying systems offer several advantages over traditional material handling methods. These include the ability to transport materials over long distances, the reduction of product contamination due to enclosed systems, and the flexibility to handle multiple materials simultaneously. The systems are also energy-efficient and can be integrated with existing processing lines, making them a cost-effective solution for many industrial applications.
HeadPowder’s multi-hopper pneumatic conveying systems are suitable for a wide range of applications. In the chemical industry, they are used to transport powders and granules, such as chemicals, pigments, and additives. In the food industry, they handle ingredients like flour, sugar, and spices, ensuring that the products remain fresh and uncontaminated. The pharmaceutical industry also benefits from these systems, as they can transport active pharmaceutical ingredients (APIs) and other sensitive materials with precision and care. Additionally, in the mining sector, they are used to transport minerals and ores from storage facilities to processing plants, improving operational efficiency and safety.
Conclusion
Multi-hopper pneumatic conveying systems represent a sophisticated solution for bulk material handling, combining advanced engineering with practical design. HeadPowder, with its expertise and commitment to quality, provides reliable and efficient systems that meet the diverse needs of modern industries. By understanding the structure and working principles of these systems, users can make informed decisions about their material handling requirements and leverage the benefits of pneumatic transport for enhanced productivity and operational efficiency.




