High-pressure bin pumps are a critical component in modern material handling systems, designed to efficiently transport bulk materials from storage silos or hoppers to processing units or other destinations. These robust systems are widely used across various industries, including chemical, pharmaceutical, food processing, and mining, due to their ability to handle a wide range of materials with high efficiency and reliability. Understanding the functionality and design principles of high-pressure bin pumps is essential for optimizing material flow and operational performance in industrial settings.
What is a High-Pressure Bin Pump?
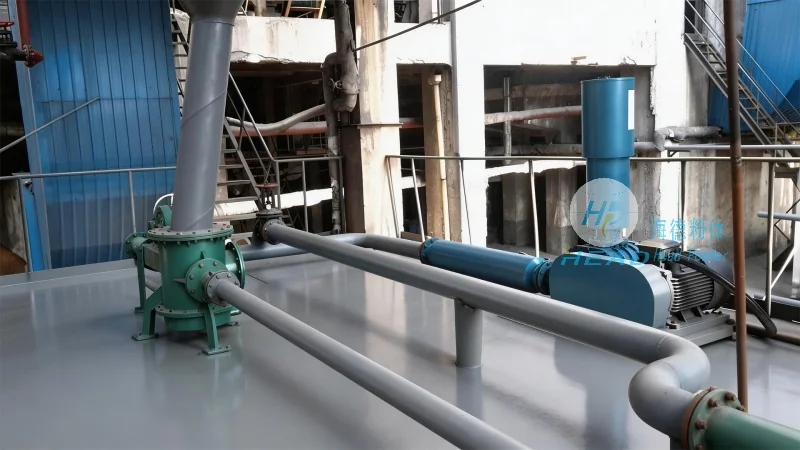
A high-pressure bin pump, also known as a pressure bin or a pneumatic conveying system, is a type of equipment that uses compressed air or other gases to transport bulk materials through a pipeline. Unlike traditional gravity-fed systems, high-pressure bin pumps can move materials over long distances and vertical heights, making them suitable for complex material handling applications. The core components of a high-pressure bin pump typically include a hopper, a rotary valve (or feeder), a pressure vessel, and a pipeline system. The hopper stores the material, while the rotary valve controls the flow rate. The pressure vessel, often equipped with a diaphragm or piston, generates the necessary pressure to push the material through the pipeline. The pipeline system delivers the material to the destination, such as a mixer, reactor, or storage tank.
Key Design Principles of High-Pressure Bin Pumps
The design of high-pressure bin pumps is centered around several key principles to ensure optimal performance and material handling capabilities. First, the system must maintain consistent pressure to ensure smooth material flow. This is achieved through the use of a pressure vessel that can handle high pressures, typically ranging from 10 to 100 bar, depending on the application. The pressure vessel is designed to withstand the forces exerted by the material and the compressed air, ensuring safety and reliability. Second, the material feed mechanism is critical. Rotary valves, such as star valves or rotary air locks, are commonly used to control the flow rate and prevent material from backflowing into the hopper. These valves are designed to handle abrasive or sticky materials without clogging, maintaining consistent performance. Third, the pipeline design is crucial for minimizing pressure loss and ensuring efficient material transport. The pipeline is typically made of corrosion-resistant materials, such as stainless steel or polyethylene, to accommodate different materials and operating conditions. The pipeline diameter and length are carefully calculated to maintain the required pressure and flow rate. Fourth, the system must incorporate safety features to prevent accidents and ensure compliance with industrial standards. This includes pressure relief valves, emergency shut-off valves, and monitoring systems to detect leaks or pressure fluctuations. Additionally, the design considers the material's properties, such as particle size, density, and moisture content, to optimize the conveying process and prevent material degradation.
Applications and Benefits of High-Pressure Bin Pumps
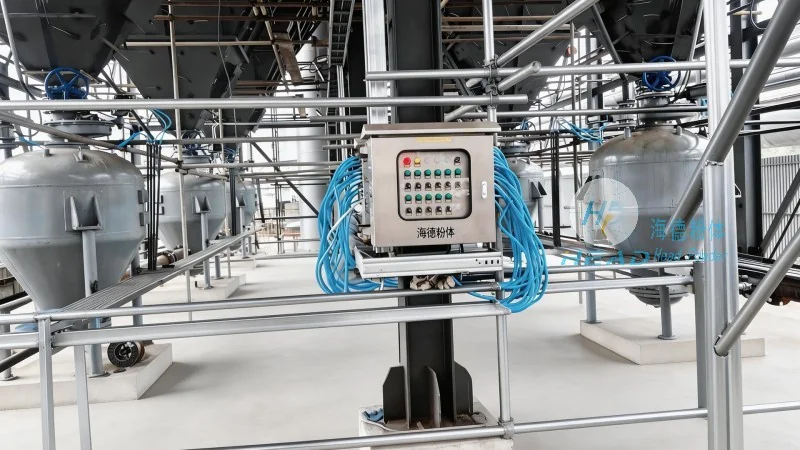
High-pressure bin pumps are widely used in various industrial applications due to their versatility and efficiency. In the chemical industry, they are used to transport powders and granules from storage silos to reactors or mixing units, ensuring a continuous and controlled supply of raw materials. In the pharmaceutical industry, these systems are employed to handle sensitive materials, such as active pharmaceutical ingredients (APIs), with minimal contamination and product degradation. The food processing industry utilizes high-pressure bin pumps to transport ingredients like flour, sugar, and spices, maintaining hygiene and preventing cross-contamination. In the mining sector, they are used to transport bulk materials like ore and coal from mines to processing plants, enabling efficient material handling over long distances. The benefits of high-pressure bin pumps include high conveying rates, minimal material degradation, low maintenance requirements, and the ability to handle abrasive or sticky materials. These advantages make them a preferred choice for industries where material flow efficiency and product quality are critical.
Company Introduction: Shandong HeadPowder Engineering Co., Ltd.
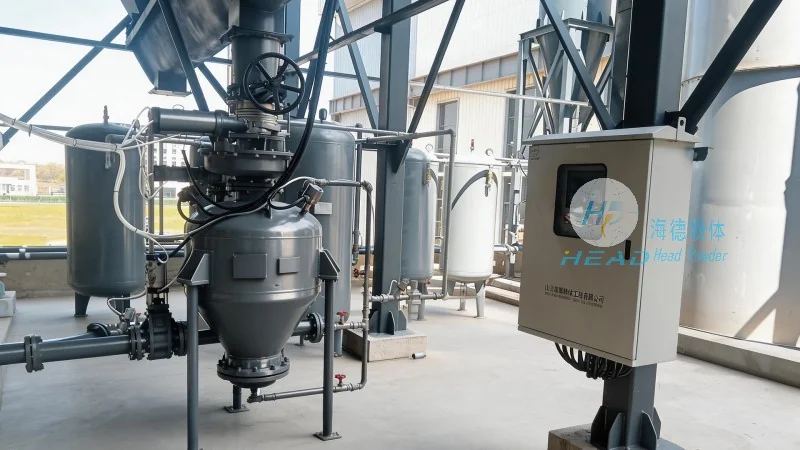
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of high-pressure bin pump material handling equipment. With a strong commitment to innovation and quality, HeadPowder has established itself as a trusted partner in the industry, providing reliable and efficient solutions for material handling challenges. The company specializes in designing and manufacturing custom high-pressure bin pumps tailored to meet the specific needs of various industries. HeadPowder's products are known for their durability, performance, and adherence to international standards, ensuring long-term operational reliability and customer satisfaction. The company's team of experienced engineers and technicians work closely with clients to understand their material handling requirements and develop optimal solutions. HeadPowder's high-pressure bin pumps are designed to handle a wide range of materials, including powders, granules, and bulk solids, with consistent performance and minimal maintenance. The company's focus on customer service and technical support ensures that clients receive comprehensive assistance throughout the product lifecycle, from installation to maintenance and troubleshooting. HeadPowder's dedication to quality and innovation has earned it a reputation as a leading provider of high-pressure bin pump material handling equipment in China and globally.
Conclusion
In conclusion, high-pressure bin pumps are essential equipment for efficient material handling in various industrial applications. Their design principles, including consistent pressure maintenance, effective material feed control, optimized pipeline design, and safety features, ensure reliable and efficient material transport. The applications of these systems span multiple industries, offering significant benefits such as high conveying rates, minimal material degradation, and low maintenance requirements. Shandong HeadPowder Engineering Co., Ltd. is a trusted provider of high-quality high-pressure bin pump systems, offering custom solutions tailored to meet the specific needs of clients. By understanding the functionality and design of high-pressure bin pumps, industries can optimize their material handling processes, improve operational efficiency, and enhance product quality. The continued innovation and quality focus of companies like HeadPowder ensure that high-pressure bin pumps remain a vital component in modern industrial material handling systems.




