Cement raw material powder conveying lines are essential industrial systems designed to transport bulk materials such as limestone, clay, and iron ore in the cement production process. These systems are critical for ensuring efficient material handling, minimizing dust emissions, and maintaining consistent quality in the raw material preparation stage. The design of such lines involves a combination of mechanical components, control systems, and engineering principles tailored to the specific characteristics of the materials being handled.
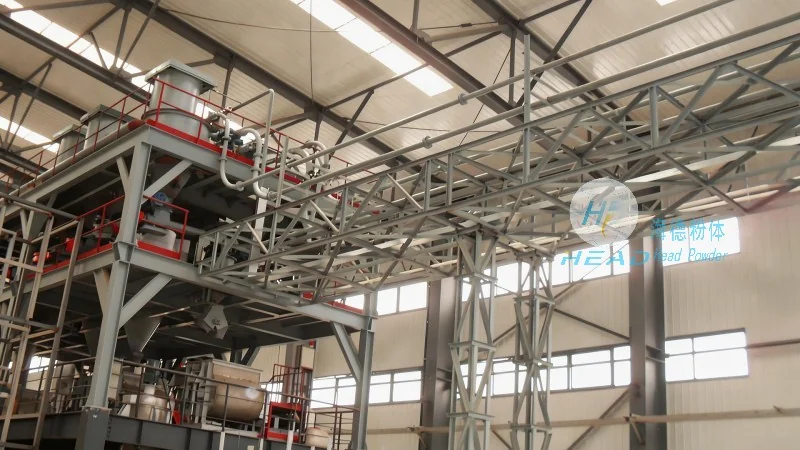
Understanding the Core Components of a Cement Raw Material Powder Conveying Line
A typical cement raw material powder conveying line consists of several key components that work in tandem to achieve reliable and efficient material transport. The primary components include feeders, conveyors (such as screw conveyors, pneumatic conveyors, or bucket elevators), dust collection systems, and control panels. Each component plays a crucial role in the overall functionality of the system. For instance, feeders are responsible for uniformly feeding the raw materials into the conveyor, while conveyors transport the material to the next processing stage. Dust collection systems are integrated to capture and filter airborne particles, ensuring compliance with environmental regulations and maintaining a safe working environment.
The Working Principle of Cement Raw Material Powder Conveying Lines
The operation of a cement raw material powder conveying line is based on the principles of material flow and air movement. In pneumatic conveying systems, for example, raw materials are mixed with air and transported through pipelines under pressure or vacuum. This method is particularly effective for handling fine powders and minimizing material degradation. Mechanical conveyors, on the other hand, rely on mechanical forces like rotation or vibration to move materials. The choice of conveying method depends on factors such as material properties, distance to be covered, and the required flow rate. Regardless of the specific technology used, the goal is to achieve a continuous, stable, and low-dust material transport process.
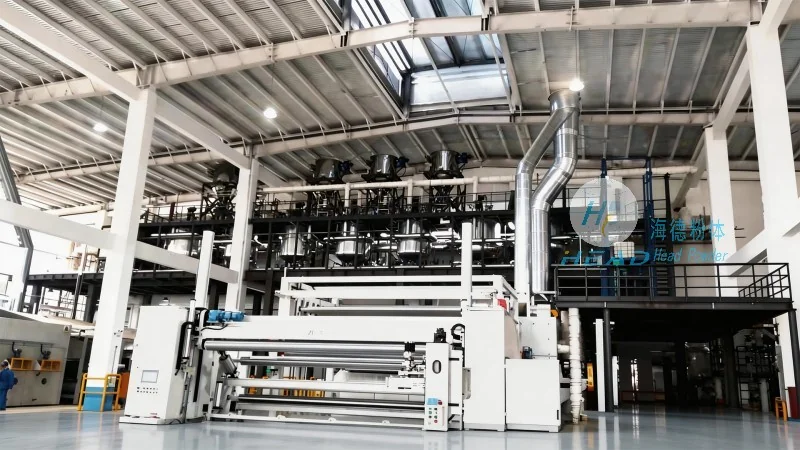
Design Principles and Considerations for Cement Raw Material Powder Conveying Lines
The design of a cement raw material powder conveying line involves careful consideration of several factors to ensure optimal performance and longevity. Key design principles include material compatibility, system efficiency, and environmental impact. Material compatibility is crucial because the components must withstand the corrosive and abrasive nature of cement raw materials. Engineers from Shandong HeadPowder Engineering Co., Ltd. (headpowder) employ advanced materials and coatings to protect equipment from wear and corrosion. System efficiency is another critical factor, as energy consumption and operational costs are significant considerations in industrial applications. The design process involves optimizing conveyor speed, pressure, and airflow to minimize energy use while maintaining the required material throughput. Additionally, environmental considerations are addressed through the integration of dust collection systems and air filtration technologies, ensuring that emissions are minimized and compliance with local regulations is maintained.
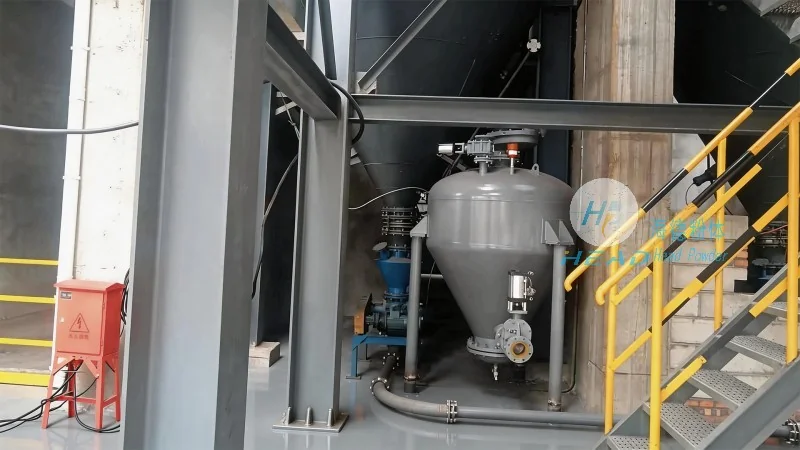
Applications and Benefits of Cement Raw Material Powder Conveying Lines
Cement raw material powder conveying lines are widely used in the cement industry for the transport of raw materials from storage silos to grinding mills. These systems offer several benefits, including improved material handling efficiency, reduced labor costs, and enhanced safety. By automating the material transport process, these systems minimize the risk of human error and exposure to hazardous materials. Furthermore, the integration of advanced control systems allows for real-time monitoring and adjustment of the conveying process, ensuring consistent material quality and flow rates. The use of such systems also contributes to overall plant productivity and operational reliability, making them a vital component of modern cement production facilities.
Conclusion: The Role of HeadPowder in Cement Raw Material Conveying Solutions
As a leading provider of engineering solutions for the cement industry, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality cement raw material powder conveying lines. With a focus on innovation and customer-centric design, headpowder ensures that their systems meet the specific needs of each client while adhering to industry standards and environmental regulations. The company's expertise in material handling and conveyor technology enables them to deliver reliable, efficient, and cost-effective solutions that enhance the performance of cement production plants. By leveraging advanced engineering principles and state-of-the-art technology, headpowder continues to play a crucial role in advancing the cement industry's operational efficiency and sustainability.




