An intelligent bag-opening pneumatic conveying system represents a sophisticated solution in material handling, designed to streamline the process of transferring bulk materials from sealed bags into processing or storage facilities. This technology integrates advanced automation and control mechanisms to enhance efficiency, reduce labor costs, and improve safety in industrial operations. The system is particularly valuable in industries such as food, pharmaceuticals, chemicals, and bulk commodities, where handling powders and granules requires precision and hygiene.
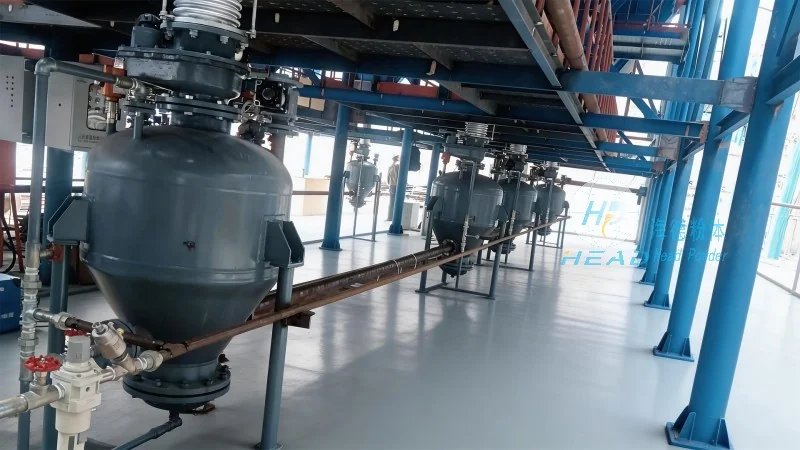
Working Principle of the System
The core operation of an intelligent bag-opening pneumatic conveying system involves several key steps. Initially, the sealed bag is positioned under a specialized opening mechanism, which may include a cutting or tearing device to access the contents without compromising the integrity of the material inside. Once the bag is opened, the material is drawn into the system through a vacuum or pressure-based pneumatic conveying line. The system uses a combination of air flow and possibly a conveying medium (like air or a carrier gas) to transport the material from the bag to the desired destination, such as a silo, hopper, or processing unit. Advanced control systems monitor the flow rate, pressure, and other parameters to ensure consistent and reliable material transfer. The process is typically automated, with sensors and feedback loops adjusting the operation in real-time to maintain optimal performance.
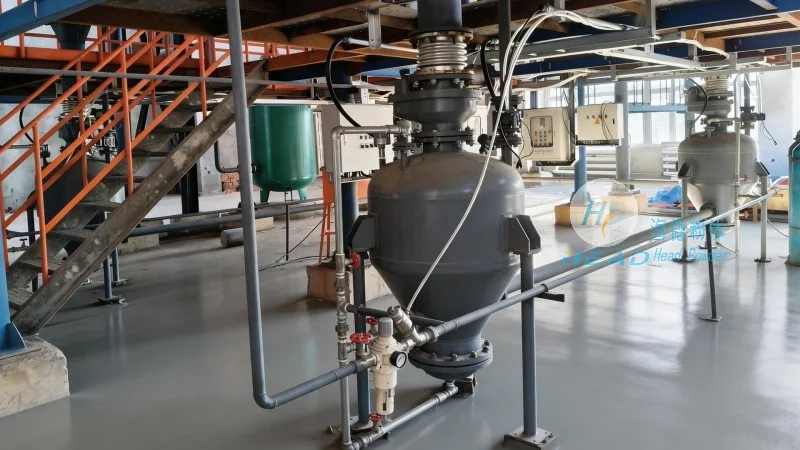
Key Features and Advantages
Several distinctive features define the intelligent bag-opening pneumatic conveying system, contributing to its effectiveness in various industrial applications. One of the primary advantages is the ability to handle a wide range of materials, including fine powders, granules, and even sensitive products that require dust-free or sterile handling. The system’s design minimizes material loss and contamination, as the bag is opened directly above the conveying line, preventing spillage and ensuring that the material remains contained. Additionally, the automated operation reduces the need for manual intervention, lowering labor costs and minimizing the risk of human error. The system also offers flexibility in terms of layout and integration with existing facilities, as it can be customized to fit different plant configurations. Another key feature is the integration of safety features, such as pressure relief valves and emergency stop mechanisms, to protect operators and equipment from potential hazards. The system’s efficiency is further enhanced by its ability to handle multiple bags simultaneously, increasing throughput and productivity.
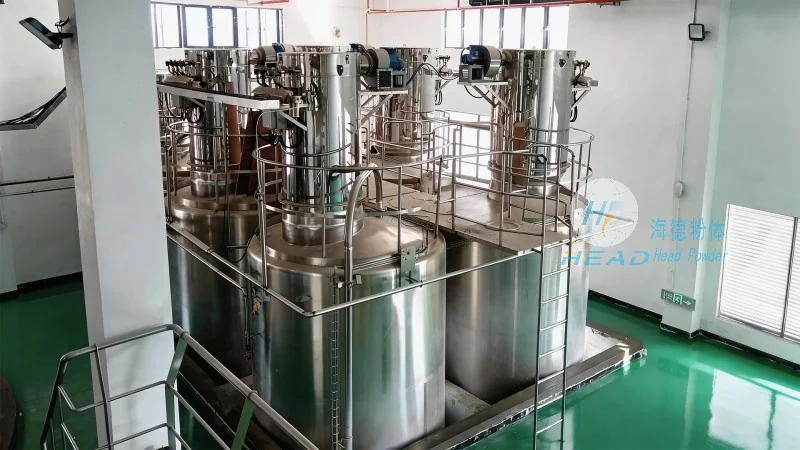
Company Information: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of advanced material handling solutions, including intelligent bag-opening pneumatic conveying systems. With a strong commitment to innovation and quality, the company has established itself as a trusted partner in the industry, providing customized solutions tailored to the specific needs of clients. HeadPowder’s products are designed to meet stringent industry standards, ensuring reliability, durability, and performance in demanding environments. The company’s headquarters is located in Shandong, China, where it maintains state-of-the-art manufacturing facilities and a dedicated team of engineers and technicians. HeadPowder’s expertise in pneumatic conveying technology and automation has enabled it to deliver solutions that enhance operational efficiency and reduce costs for its clients across various sectors.




