Efficient and reliable powder handling and transport systems are critical in the fine chemical industry, where precise control over material flow is essential for maintaining product quality and operational efficiency. For companies operating in this sector, understanding the underlying mechanisms and advantages of such systems is paramount to optimizing production processes and ensuring safety standards are met.
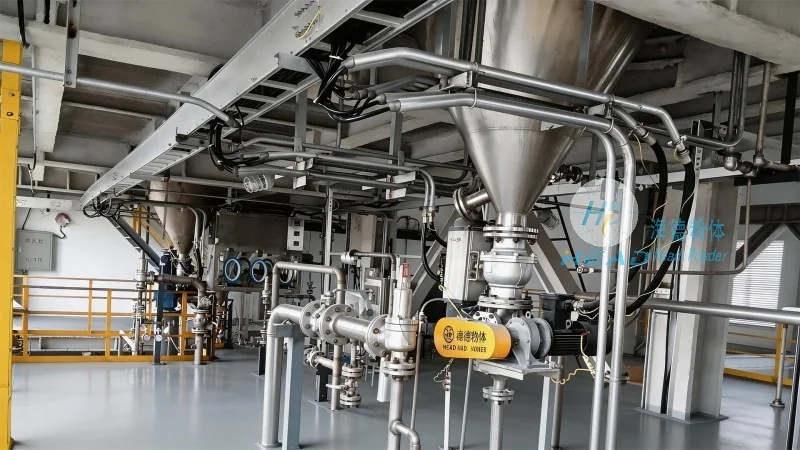
Working Principles of Fine Chemical Powder Handling Systems
The core of fine chemical powder handling systems lies in their ability to transport powders from one location to another with minimal degradation or loss. These systems typically incorporate several key components, including feeders, conveyors, and control mechanisms, all working in tandem to ensure smooth material movement. The working principle involves the controlled feeding of powder into a conveyor, which then transports it through a pipeline or open path to the destination. Advanced systems may utilize pneumatic or mechanical methods, depending on the properties of the powder and the required transport distance. For example, pneumatic conveying uses compressed air to move powders, while mechanical conveyors rely on belts, screws, or buckets. The selection of the appropriate method depends on factors such as powder density, moisture content, and particle size, ensuring optimal performance and minimal material degradation.
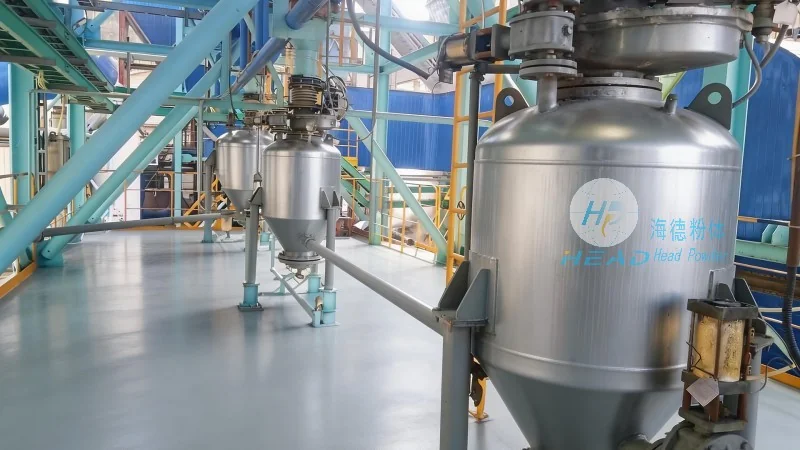
Key Characteristics of Fine Chemical Powder Transport Solutions
When evaluating fine chemical powder transport solutions, several characteristics stand out as critical for successful implementation. First, efficiency is a primary consideration, as the system must minimize downtime and maximize throughput. This is achieved through robust design and reliable components that can handle the specific demands of fine chemicals. Second, safety is paramount, given the potential hazards associated with powders, such as dust explosions or inhalation risks. Modern systems incorporate features like explosion-proof designs, dust collection systems, and enclosed conveyors to mitigate these risks. Third, precision is essential for maintaining product quality, as even minor variations in flow rate or particle distribution can impact the final product. Advanced control systems, including sensors and automation, help achieve precise control over the transport process. Additionally, versatility is a key characteristic, as these systems must be adaptable to different powder types and production requirements. This flexibility allows companies to scale operations or adjust to changing production needs without significant modifications to the transport infrastructure.
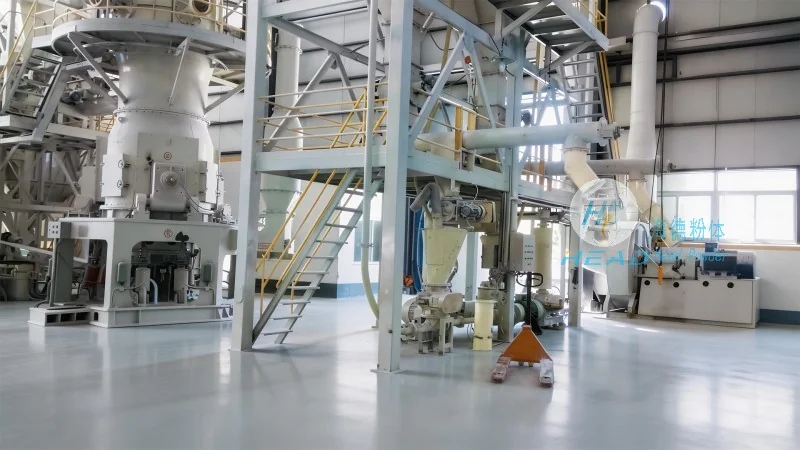
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading provider of specialized powder handling solutions, is dedicated to delivering innovative and reliable systems for the fine chemical industry. With a focus on engineering excellence and customer-centric design, the company has established itself as a trusted partner for businesses seeking to enhance their powder transport capabilities. HeadPowder’s expertise lies in the development of customized systems that address the unique challenges of fine chemicals, ensuring optimal performance and safety. The company’s commitment to quality and innovation has earned it a reputation for delivering solutions that meet the highest industry standards. Based in Shandong, China, HeadPowder leverages its local presence and technical capabilities to serve clients both domestically and internationally, providing comprehensive support from system design to installation and maintenance. By combining advanced technology with practical application, HeadPowder helps fine chemical manufacturers improve operational efficiency, reduce costs, and enhance product quality.




