Introduction to the Equipment and Structural Principles of the Camellia Seed Pneumatic Conveying Sys
Release time:2026-09-22 02:01:42
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
HeadPowder, a leading manufacturer in the field of industrial processing equipment, specializes in the design and production of advanced pneumatic conveying systems tailored for various agricultural and food processing applications. This document provides an overview of the camellia seed pneumatic conveying system, detailing its key components, operational principles, and technical advantages.
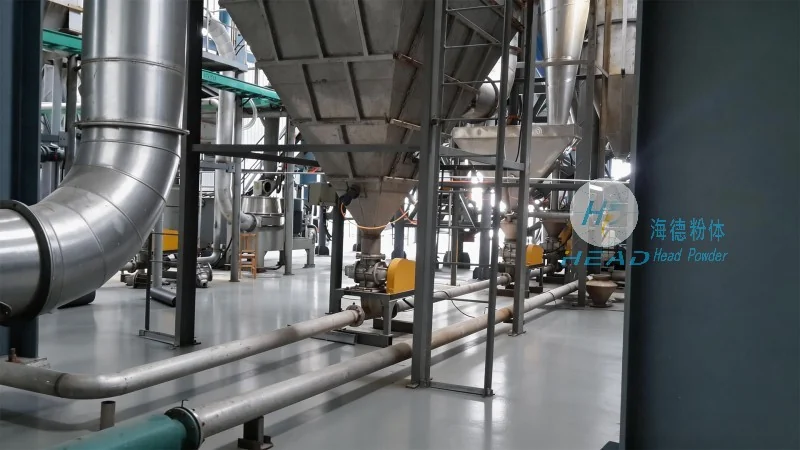
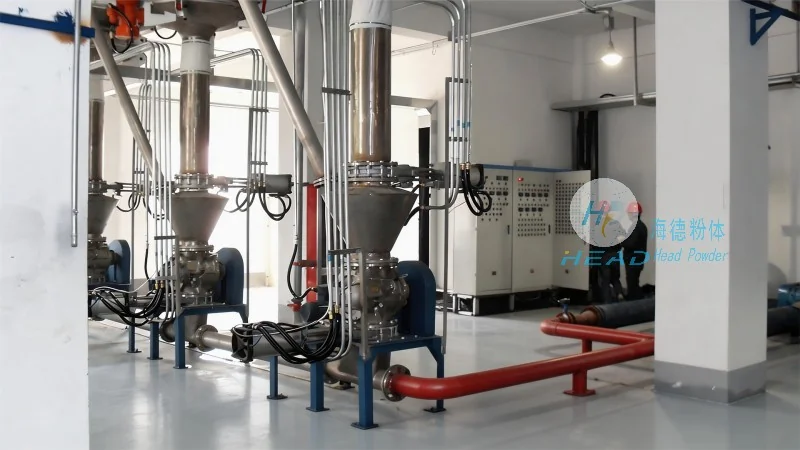
Overview of the Camellia Seed Pneumatic Conveying System
The camellia seed pneumatic conveying system is engineered to efficiently transport camellia seeds from storage silos or processing areas to subsequent processing units such as oil extraction or packaging facilities. Developed by Shandong HeadPowder Engineering Co., Ltd., this system integrates high-efficiency air handling units, flexible hose or pipe networks, and specialized conveying nozzles to ensure reliable and low-maintenance operation. The system is particularly suited for applications requiring gentle handling of seeds to preserve their quality and integrity during transport.
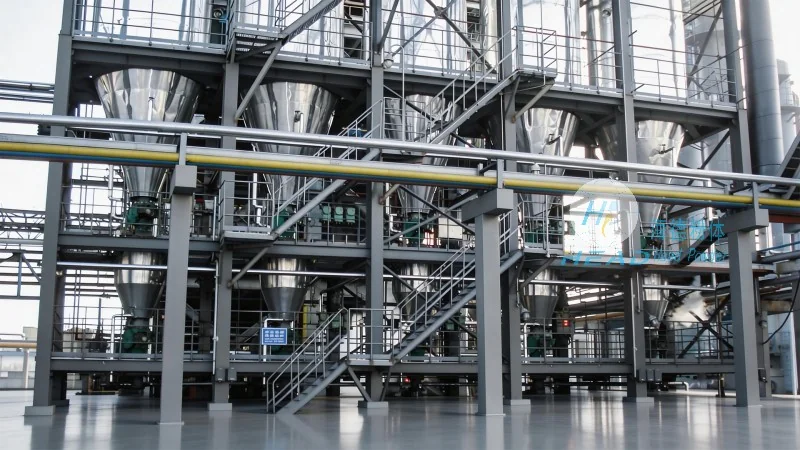
Structural Components and Working Principle
The system comprises several core components that work in tandem to achieve effective material transport. The primary components include an air compressor or blower, a hopper or feed hopper for seed loading, a conveying line (typically made of stainless steel or flexible PVC), and a receiver or discharge hopper at the destination. The working principle is based on the use of compressed air to create a low-pressure or high-pressure air stream that draws the camellia seeds into the conveying line through a feeding mechanism. The air and seed mixture travels through the pipeline, with the air providing the necessary force to move the seeds while minimizing product damage. The system may also incorporate features such as air filtration, moisture control, and pressure regulation to optimize performance and maintain product quality.
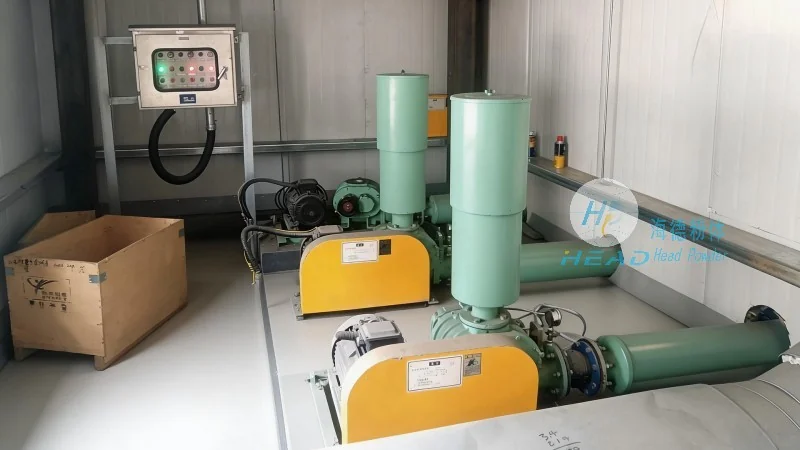
Technical Specifications and Application Advantages
HeadPowder's camellia seed pneumatic conveying system is designed to meet the specific demands of modern seed processing operations. Key technical specifications include adjustable conveying capacities ranging from 1 to 50 tons per hour, depending on the system configuration and seed characteristics. The system operates with minimal product loss, typically maintaining a recovery rate of over 99%, which is crucial for maximizing yield in oil extraction processes. Additionally, the use of stainless steel components ensures compliance with food safety standards and facilitates easy cleaning and maintenance. The system's modular design allows for flexible installation in existing processing facilities, reducing downtime and installation costs. Its energy-efficient operation, with optimized air consumption and reduced mechanical wear, contributes to lower operational costs over the system's lifespan. The system's ability to handle a wide range of seed sizes and moisture contents without clogging or blockages makes it a versatile solution for various camellia seed processing applications.




