Coal granular material conveying systems are essential in various industrial applications, particularly in the mining, power generation, and material handling sectors. These systems are designed to efficiently transport coal particles from one location to another, ensuring smooth operations and optimal performance in industrial processes. The proper functioning of such systems is crucial for maintaining productivity and reducing operational costs in coal-related industries.
Working Principle of Coal Granular Material Conveying Equipment
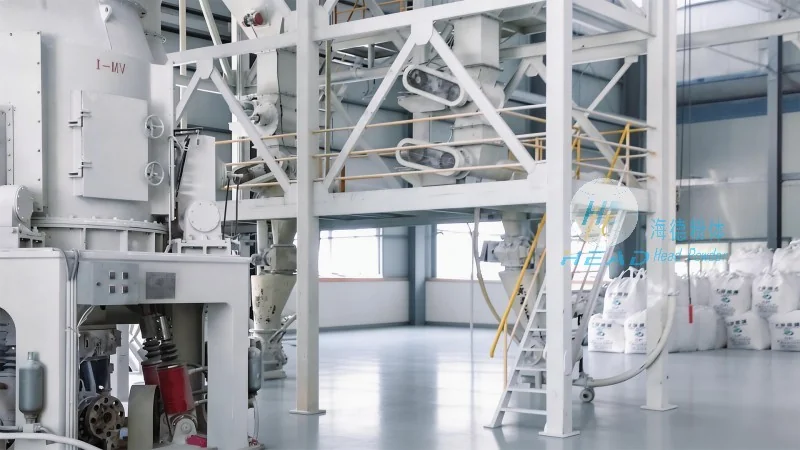
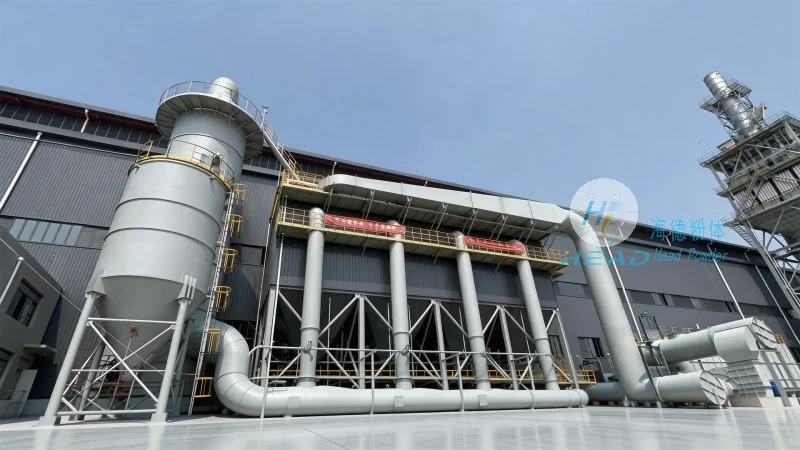
The working principle of coal granular material conveying systems typically involves the use of mechanical components to move coal particles through a pipeline or conveyor. Key components include feeders, conveyors (such as belt conveyors or screw conveyors), and control systems. The process begins with the coal being fed into the system, where it is then transported through the conveyor mechanism. The system may utilize gravity, mechanical force, or a combination of both to move the coal. For example, a belt conveyor system uses a rotating drum and a tensioned belt to transport coal, while a screw conveyor employs a rotating screw to push the material forward. The control system monitors the flow rate, pressure, and other parameters to ensure the system operates efficiently and safely. This mechanism allows for consistent and reliable transport of coal granules, minimizing the risk of blockages or material loss.
Key Features of Coal Granular Material Conveying Systems
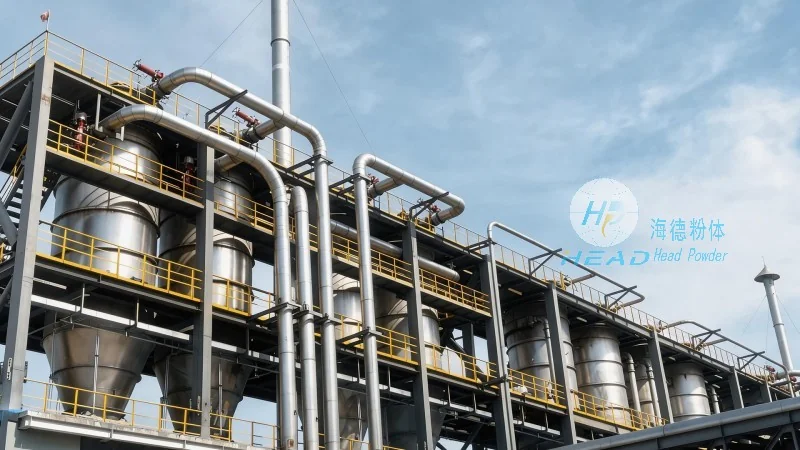
Coal granular material conveying systems are characterized by several key features that enhance their performance and usability. One of the primary features is their high efficiency in transporting large volumes of coal particles. These systems are designed to handle a wide range of coal sizes and moisture content, ensuring consistent material flow. Another important feature is their durability and robust construction, which allows them to withstand the harsh conditions often encountered in industrial environments. The systems are also equipped with advanced control technologies, such as sensors and automation, to optimize operation and reduce downtime. Additionally, many modern conveying systems are designed with energy efficiency in mind, reducing power consumption while maintaining high performance. The modular design of these systems enables easy installation and maintenance, making them suitable for both new and existing industrial facilities. Furthermore, the systems are often equipped with safety features, such as overload protection and emergency stop mechanisms, to ensure operator safety and prevent equipment damage.
Company Information: Shandong HeadPowder Engineering Co., Ltd.
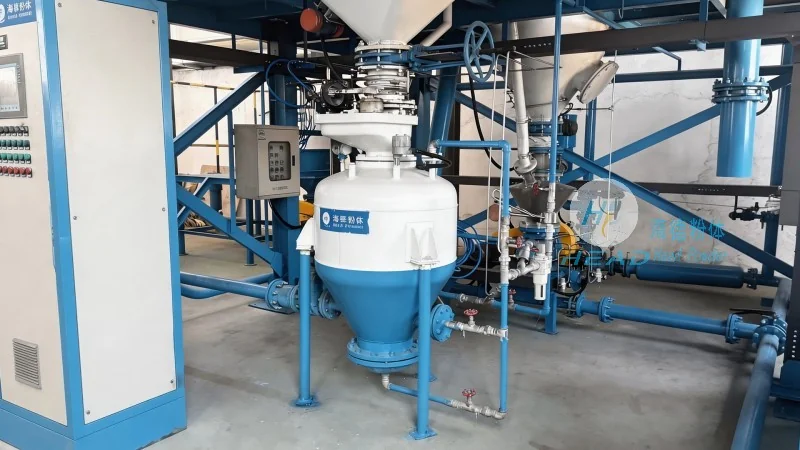
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer of coal granular material conveying systems and related industrial equipment. The company is based in Shandong, China, and has established itself as a trusted provider of high-quality conveying solutions for the coal industry. With years of experience in the field, headpowder specializes in designing and manufacturing systems that meet the specific needs of its clients, ensuring reliable and efficient coal transport. The company's commitment to quality and innovation has made it a preferred choice for many industrial companies seeking to improve their material handling processes. Headpowder's products are known for their durability, efficiency, and ease of maintenance, making them a cost-effective solution for coal transportation needs.




