Working Principle and Features of Air-Pneumatic Conveying Equipment for Sand and Soil Materials
Release time:2026-09-18 12:01:28
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced air-pneumatic conveying systems tailored for handling sand and soil materials. This equipment is engineered to efficiently transport bulk materials through a pneumatic system, offering a reliable solution for various industrial applications.
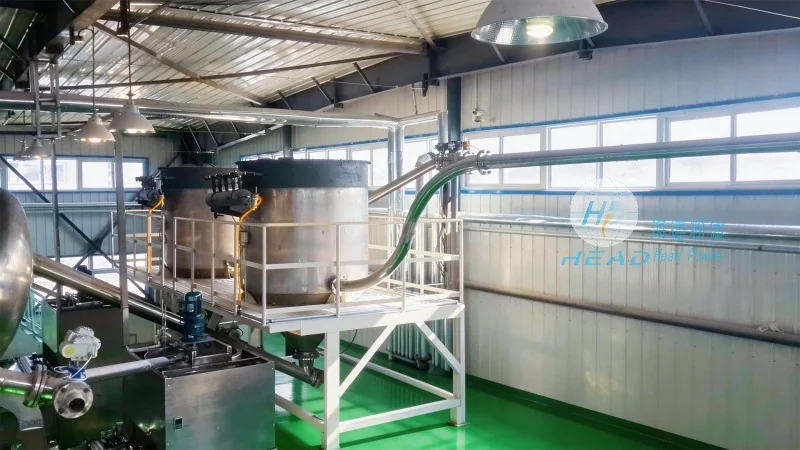
Working Principle of Air-Pneumatic Conveying Equipment
The air-pneumatic conveying system operates by utilizing compressed air to move sand and soil materials through a pipeline. The process typically involves a hopper where the material is loaded, followed by the introduction of air into the system. As air flows through the pipeline, it creates a low-pressure zone that draws the material particles along with it. The equipment may include components such as a blower, cyclone separator, and a discharge outlet to control the flow and separation of the material. This method ensures a continuous and controlled transfer of sand and soil, minimizing material degradation and loss.
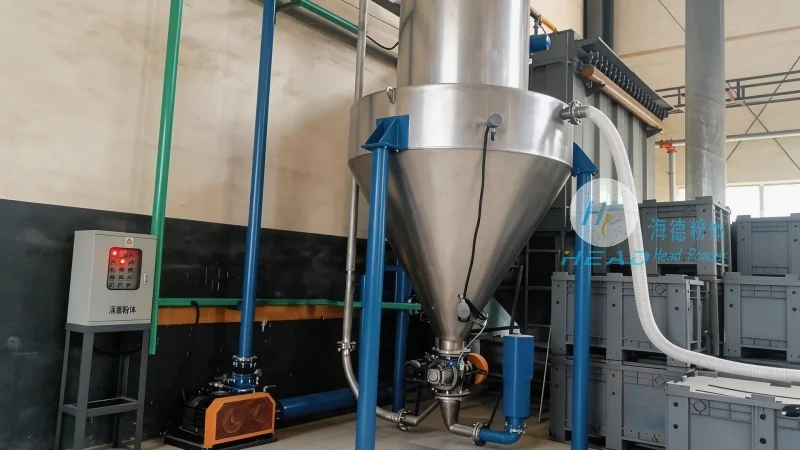
Key Features of Air-Pneumatic Conveying Equipment
HeadPowder's air-pneumatic conveying equipment for sand and soil materials is characterized by several notable features that enhance performance and efficiency. Firstly, the system offers a high degree of flexibility in material handling, allowing for the transport of various types of sand and soil with different particle sizes and moisture content. Secondly, it provides a dust-free operation, which is crucial for maintaining a clean working environment and complying with industrial safety standards. Thirdly, the equipment is designed for low maintenance, with robust components that can withstand the abrasive nature of sand and soil, reducing downtime and operational costs. Additionally, the system can be customized to meet specific application requirements, ensuring optimal performance in different industrial settings.
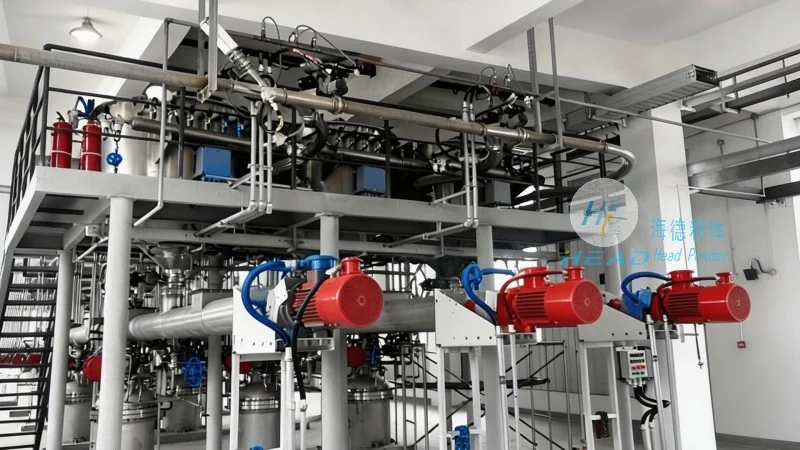
Benefits of Using Air-Pneumatic Conveying Equipment
The adoption of air-pneumatic conveying equipment for sand and soil materials brings numerous benefits to industrial operations. One of the primary advantages is the ability to transport materials over long distances without the need for mechanical components like belts or chains, which can be prone to wear and tear. This reduces the risk of material contamination and ensures a cleaner transfer process. Another benefit is the energy efficiency of the system, as compressed air can be used to move materials with minimal energy consumption compared to traditional conveyor systems. Furthermore, the system allows for easy integration with other industrial processes, such as material mixing or processing, enhancing overall operational efficiency. The reliability of the equipment also contributes to improved productivity, as it minimizes material loss and ensures consistent delivery of sand and soil to the intended destination.




