HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for handling soda ash materials. This article explores the fundamental working principle and key features of such equipment, providing insights into its operational efficiency and industrial applications.
Understanding the Working Principle of Soda Ash Pneumatic Conveyors
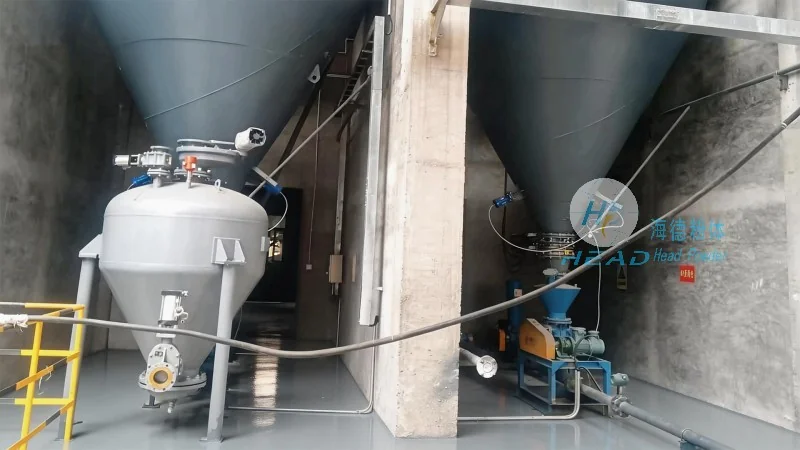
The core mechanism of a soda ash material pneumatic conveying system revolves around the use of air or gas to transport bulk materials through a pipeline network. The process typically begins with the material being fed into a hopper or feeder, where it is then introduced into the conveying line. A fan or blower generates the necessary airflow, creating a pressure differential that propels the material forward. This method, known as pneumatic conveying, eliminates the need for mechanical components like belts or buckets, reducing maintenance requirements and enhancing safety in material handling operations.
There are two primary types of pneumatic conveying systems: dilute-phase and dense-phase. Dilute-phase systems use high-velocity air to move materials in a dispersed state, suitable for short-distance and low-volume applications. In contrast, dense-phase systems employ lower velocities and higher pressure to transport materials in a more concentrated form, ideal for longer distances and higher material loads. For soda ash, which is often handled in bulk, dense-phase conveying is frequently preferred due to its ability to maintain material integrity and prevent degradation during transport.
Key Features of Soda Ash Pneumatic Conveying Equipment
HeadPowder's pneumatic conveying equipment for soda ash is engineered with several distinctive features that enhance performance and reliability. One notable characteristic is the robust material handling capability, designed to accommodate the abrasive and corrosive nature of soda ash. The equipment incorporates wear-resistant components, such as stainless steel or special alloys, to minimize wear and extend service life. Additionally, the system is equipped with advanced control mechanisms that allow for precise regulation of airflow and pressure, ensuring consistent material flow and preventing blockages or system failures.
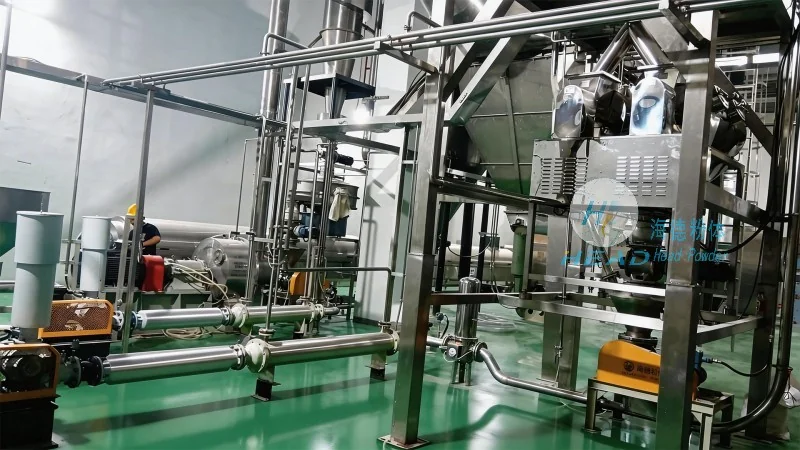
Another critical feature is the integration of dust control measures. Soda ash is a fine powder that can generate significant dust during handling, posing health and safety risks. The conveying system incorporates sealed hopper designs and air filtration systems to contain dust, maintaining a clean and safe working environment. This not only protects personnel but also complies with environmental regulations, making the equipment suitable for various industrial settings.
The equipment also offers flexibility in system configuration, allowing for customization based on specific operational needs. Whether for short or long-distance transport, or for handling varying material volumes, the system can be adjusted to meet the requirements of different production processes. This adaptability makes it a versatile solution for industries such as chemical manufacturing, food processing, and pharmaceuticals, where soda ash is commonly used as a raw material.
Operational Advantages and Applications
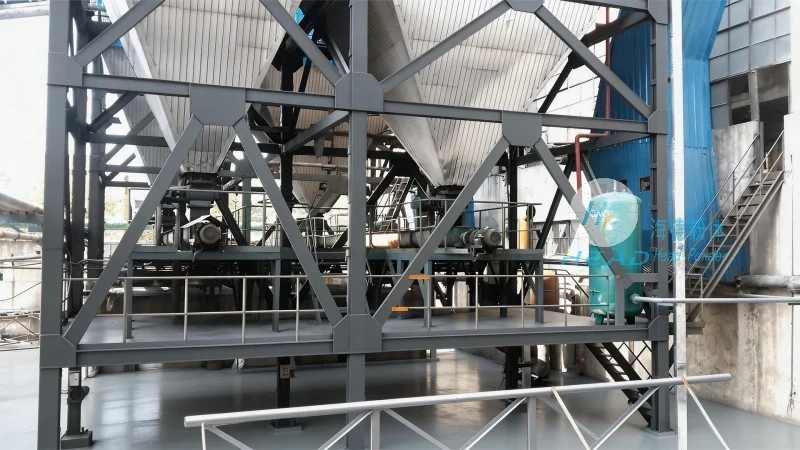
Implementing a soda ash pneumatic conveying system offers several operational advantages. The primary benefit is the reduction in labor costs, as the system automates the material transport process, minimizing the need for manual handling. This not only improves efficiency but also enhances workplace safety by eliminating the risks associated with manual material handling. Additionally, the system reduces material loss and contamination, ensuring that the soda ash remains in its original state throughout the transport process.
From a production perspective, the equipment enhances process reliability by providing consistent material flow, which is crucial for maintaining stable production rates. The ability to handle large volumes of soda ash in a continuous manner supports high-throughput operations, making it suitable for large-scale industrial applications. Furthermore, the system's compact design allows for easy integration into existing production lines, minimizing downtime during installation and operation.
In summary, the working principle and features of soda ash material pneumatic conveying equipment, as exemplified by HeadPowder's solutions, represent a sophisticated approach to bulk material handling. By leveraging pneumatic technology, these systems offer efficient, safe, and reliable transport of soda ash, contributing to improved operational performance and cost-effectiveness in various industrial sectors.




