For industries dealing with calcined sand materials, efficient and reliable material handling is crucial. A pneumatic conveyor system, specifically designed for calcined sand, offers a solution that combines performance with operational flexibility. This article explores the working principle and key features of such a system, highlighting how it addresses the unique challenges associated with transporting calcined sand efficiently.
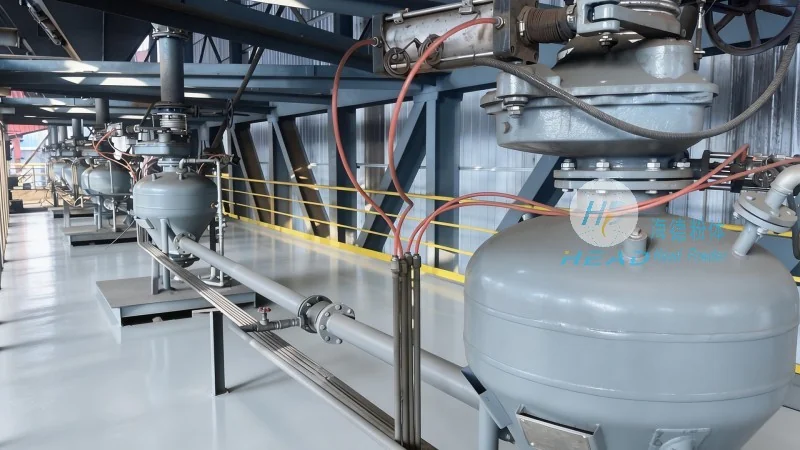
The Working Principle of a Pneumatic Conveyor for Calcined Sand
The core of a pneumatic conveyor for calcined sand is its ability to transport bulk materials through a pipeline using air pressure. The system operates by creating a pressure differential between the inlet and outlet of the conveyor. At the material loading point, the calcined sand is introduced into the pipeline, and a fan or blower generates a flow of air that propels the material forward. The air flow can be either positive pressure (where air pushes the material) or negative pressure (where air pulls the material, also known as a vacuum system). The design of the conveyor, including the type of fan, pipeline diameter, and material feed mechanism, is tailored to handle the specific properties of calcined sand, such as its density, particle size, and flow characteristics.
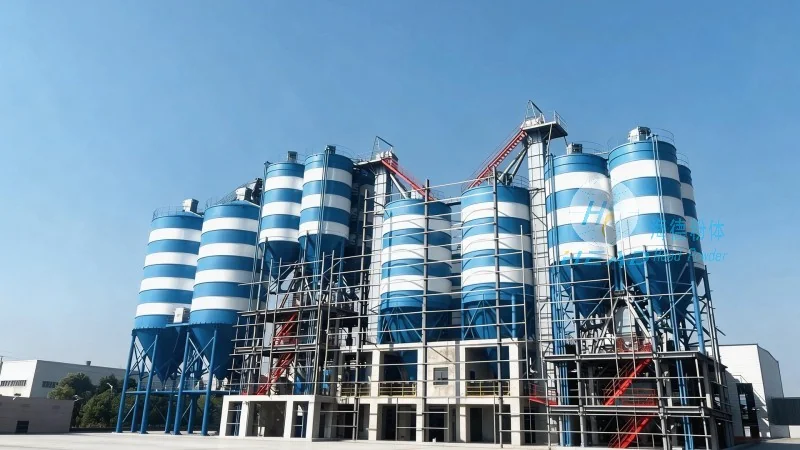
Key Features of the Pneumatic Conveyor System
Several features make a pneumatic conveyor for calcined sand an effective choice for material handling. First, it provides a dust-free and enclosed transport environment, which is essential for maintaining material quality and ensuring a safe working environment. The system minimizes material degradation and contamination, which is critical for calcined sand used in various industrial applications. Second, the conveyor offers high flexibility in terms of layout, as it can be installed in various configurations, including vertical, horizontal, or a combination of both, to suit the plant layout. This adaptability allows for efficient use of space and integration with existing production lines. Third, the system is energy-efficient compared to traditional methods like belt conveyors or bucket elevators, as it uses air pressure to move the material, reducing mechanical wear and maintenance costs. Additionally, the conveyor can handle a wide range of material flow rates, from low to high, making it suitable for both small-scale and large-scale operations. The material handling capacity can be adjusted by modifying the air flow rate and the design of the feed hopper.
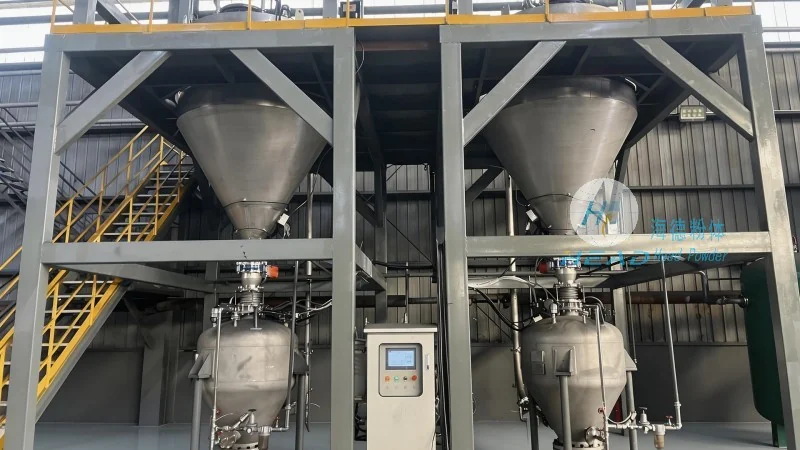
Company Information: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field of material handling equipment, specializes in designing and manufacturing pneumatic conveyors tailored to the needs of various industries. With a focus on quality and innovation, the company has developed advanced systems that meet the stringent requirements of calcined sand transportation. HeadPowder's products are engineered to ensure durability, reliability, and optimal performance, providing customers with a cost-effective solution for their material handling challenges. The company's headquarters is located in Shandong, China, where it has established a strong presence in the industry with a commitment to customer satisfaction and technological advancement.




