Phosphate fertilizer is a critical component in modern agricultural practices, and the efficient handling of phosphate powder is essential for maintaining productivity and sustainability in the fertilizer industry. Pneumatic conveying systems have emerged as a reliable solution for transporting phosphate powder, offering advantages such as low maintenance, minimal product contamination, and the ability to handle bulk materials over long distances. This article explores the fundamental principles of phosphate powder pneumatic conveying systems and highlights the key working scene characteristics that make them suitable for various industrial applications, with a focus on solutions provided by Shandong HeadPowder Engineering Co., Ltd.
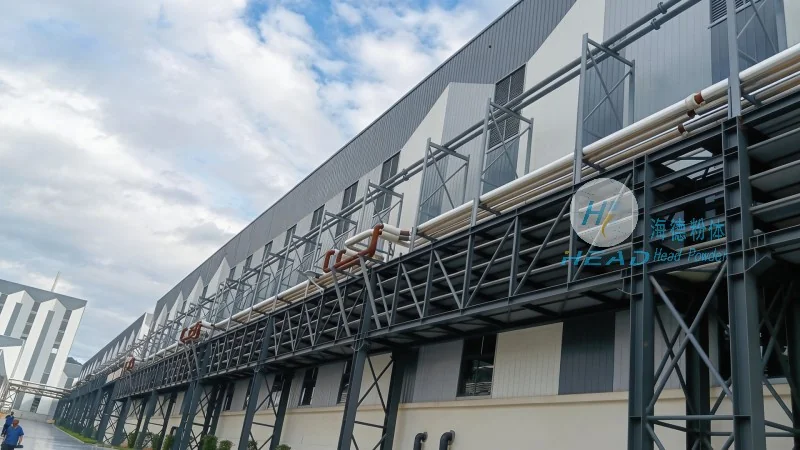
Introduction to Phosphate Powder Pneumatic Conveying Systems
Phosphate powder, derived from phosphate rock processing, is a fine, dry material that requires specialized handling to prevent caking, segregation, and loss. Traditional methods like bucket elevators or belt conveyors may not be suitable due to the abrasive nature of phosphate powder and the need for dust control. Pneumatic conveying systems, which use air or gas to transport bulk materials, provide an effective alternative. These systems are designed to move phosphate powder from storage silos, processing units, or packaging areas to various destinations, such as blending facilities, storage tanks, or shipping containers. The systems are engineered to maintain product integrity while ensuring efficient material flow, making them a preferred choice in phosphate processing operations.
Core Principles of Pneumatic Conveying
The operation of a phosphate powder pneumatic conveying system is based on the principle of fluidization and suspension. The system typically consists of a blower or compressor that generates airflow, a hopper or feeder to introduce the phosphate powder, and a pipeline network to transport the material. The powder is suspended in the air stream and carried through the pipeline, where it is deposited at the discharge point. The key parameters that influence the system's performance include air velocity, pressure, and the material's properties, such as particle size, density, and moisture content. Proper design ensures that the air velocity is sufficient to keep the powder in suspension without causing excessive wear on the system components. The system's efficiency is directly related to how well these parameters are optimized for the specific characteristics of the phosphate powder being handled.
Working Scene Characteristics
The suitability of phosphate powder pneumatic conveying systems is determined by several working scene characteristics that align with the operational needs of the fertilizer industry. These characteristics include:
1. Material Handling Efficiency: Pneumatic conveying systems can handle large volumes of phosphate powder quickly and continuously, reducing labor costs and improving throughput. The ability to transport material over long distances without intermediate handling points enhances operational efficiency, especially in large-scale phosphate processing plants.
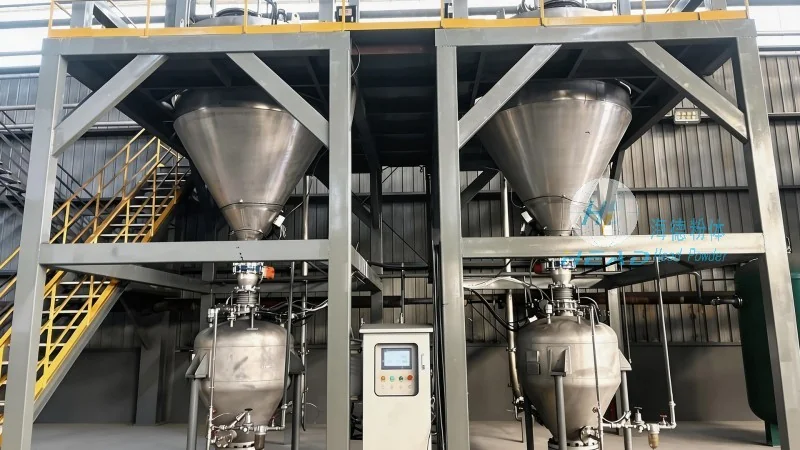
2. Dust Control and Environmental Compliance: Unlike mechanical conveyors, pneumatic systems are enclosed, which minimizes dust emissions and ensures compliance with environmental regulations. This is particularly important in phosphate processing plants where dust can be a health and safety hazard, and where strict emission standards must be met.
3. Product Integrity Preservation: The enclosed nature of pneumatic conveying prevents contamination from external sources and reduces the risk of product degradation due to exposure to air or moisture. This is crucial for maintaining the quality of phosphate fertilizer, which is sensitive to changes in moisture and particle size that could affect its performance in agricultural applications.
4. Space Optimization: Pneumatic systems can be installed in tight spaces or vertically, making them suitable for facilities with limited floor area. The flexibility in pipeline routing allows for integration with existing infrastructure without major structural modifications, reducing installation time and costs.
Application Scenarios
Phosphate powder pneumatic conveying systems are widely used in various industrial settings, including:
1. Phosphate Rock Processing Plants: In these facilities, the system transports raw phosphate rock to grinding mills and then moves the ground phosphate powder to storage silos or packaging lines. The high capacity and dust control features make it ideal for handling the large volumes of material processed in these plants, ensuring smooth and continuous operation.
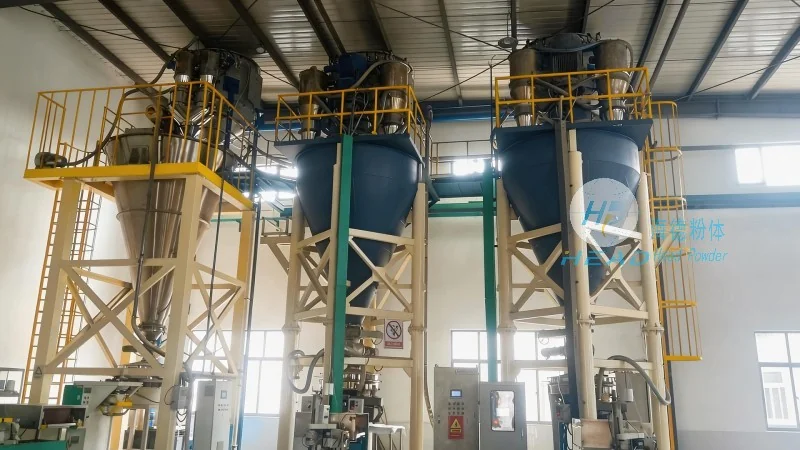
2. Fertilizer Blending and Packaging Facilities: After processing, phosphate powder is often blended with other nutrients to create customized fertilizer products. Pneumatic conveying systems efficiently transport the blended powder to packaging machines, ensuring consistent product quality and reducing downtime by minimizing material handling errors.
3. Storage and Distribution Centers: In storage facilities, the system moves phosphate powder from bulk storage tanks to loading areas for transportation to farms or other end-users. The ability to handle long-distance transport and maintain product integrity is essential for efficient distribution, particularly in regions with extensive agricultural operations.
Advantages and Considerations
While pneumatic conveying systems offer significant benefits, there are considerations to keep in mind when implementing such a system for phosphate powder. The main advantages include low maintenance costs, high material throughput, and the ability to handle abrasive materials without excessive wear. However, the system's performance is highly dependent on the proper selection of air velocity and pressure, which must be optimized based on the specific properties of the phosphate powder being transported. Additionally, the initial investment for a pneumatic conveying system can be higher than for mechanical alternatives, though the long-term operational savings often justify the cost. Proper system design and regular maintenance are critical to ensuring reliable performance and maximizing the lifespan of the equipment.
Conclusion
Phosphate powder pneumatic conveying systems are a proven technology for efficiently handling phosphate fertilizer in various industrial applications. By understanding the core principles and working scene characteristics, industries can leverage these systems to improve operational efficiency, maintain product quality, and comply with environmental regulations. As the demand for phosphate fertilizer continues to grow, the adoption of advanced pneumatic conveying solutions will play a crucial role in meeting the needs of modern agriculture and sustainable resource management. Shandong HeadPowder Engineering Co., Ltd. remains committed to providing innovative and reliable pneumatic conveying solutions tailored to the unique requirements of the phosphate industry, helping clients achieve their operational and sustainability goals.




