HeadPowder, a leading provider in the field of material handling solutions, specializes in the design and implementation of advanced pneumatic conveying systems tailored for silica fume. This article delves into the fundamental principles behind these systems and highlights the key characteristics of their operational environments.
Understanding the Core Principle of Silica Fume Pneumatic Conveying
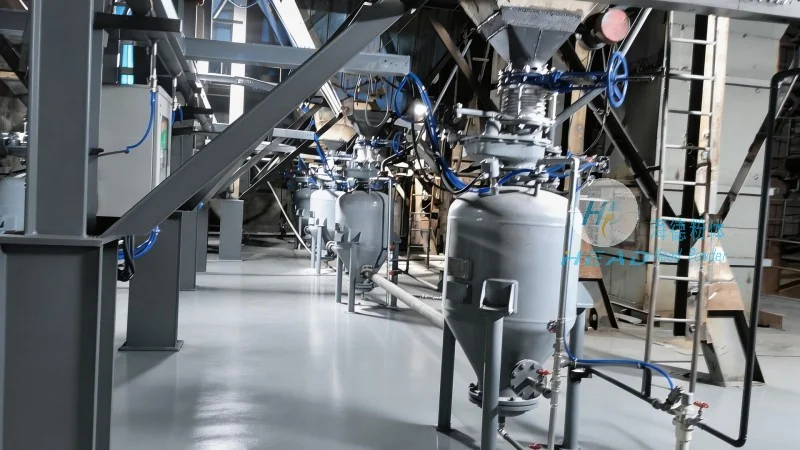
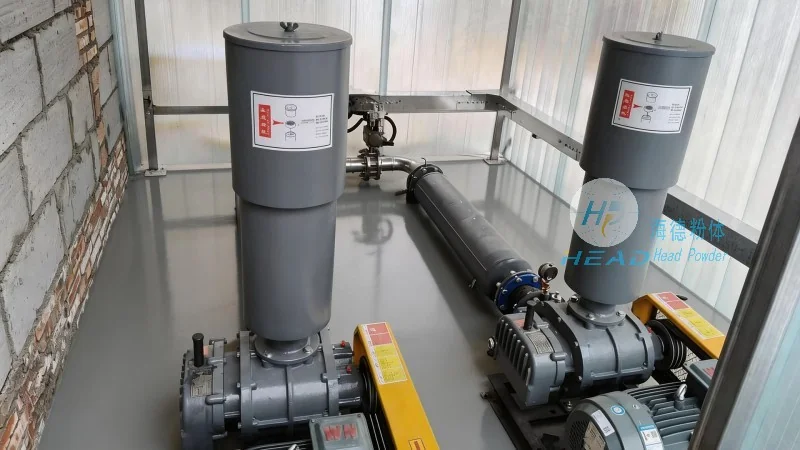
The pneumatic conveying system for silica fume operates on the principle of transporting bulk materials through a pipeline using a gas stream, typically air or other suitable gases. This method eliminates the need for mechanical components like belts or buckets, offering a more efficient and cost-effective solution for handling fine powders. The system typically consists of a material feed hopper, a conveying pipeline, a gas source (such as a blower or compressor), and a discharge unit. The process begins when the silica fume is introduced into the hopper, where it is then drawn into the pipeline by the moving gas stream. The gas velocity is carefully controlled to ensure that the powder particles are entrained and transported without clogging or degradation. This method is particularly effective for handling materials with high moisture content or those that are prone to agglomeration, as the air stream helps to maintain particle separation and prevent blockages.
Key Working Scene Characteristics of Silica Fume Pneumatic Conveying Systems
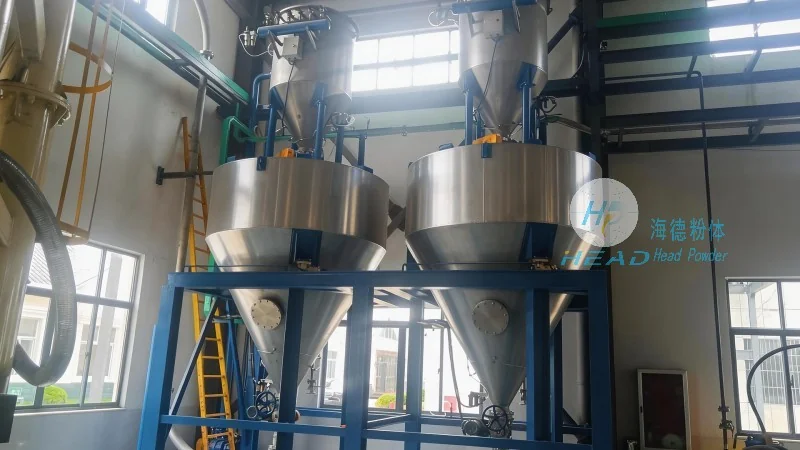
The operational characteristics of silica fume pneumatic conveying systems are closely tied to the specific industrial applications they serve. These systems are commonly employed in environments where precise material control and minimal contamination are critical. For instance, in the production of concrete additives, the system must maintain a consistent flow rate and particle size distribution to ensure uniform mixing with other cementitious materials. The working scene often involves high-volume material handling, requiring robust system designs capable of handling large quantities of silica fume without loss or degradation. Additionally, the systems are designed to operate in environments with varying ambient conditions, such as temperature and humidity fluctuations, which can impact the material's properties and the system's performance. The discharge mechanisms are engineered to prevent material buildup and ensure smooth transfer to the next processing stage, whether it be storage, mixing, or further processing.
Application Scenarios and Operational Efficiency
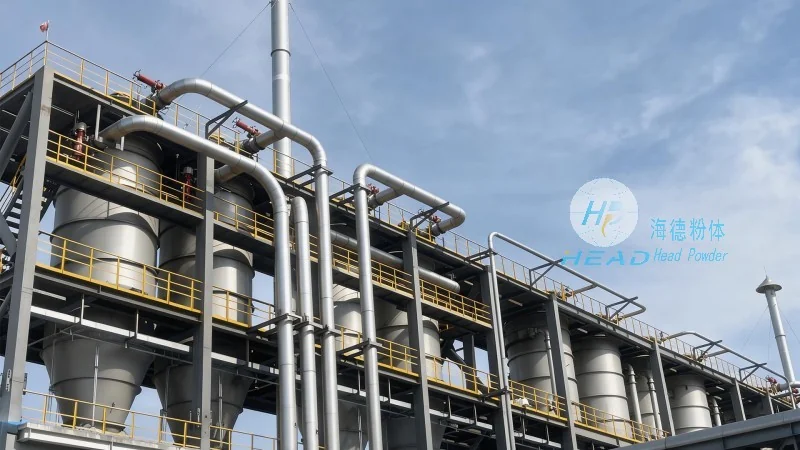
HeadPowder's pneumatic conveying systems for silica fume are widely utilized in various industrial settings, including cement plants, concrete manufacturing facilities, and chemical processing plants. In cement production, the system is used to transport silica fume from storage silos to the mixing units, where it is incorporated into the cement matrix to enhance the final product's properties. The efficiency of these systems is evident in their ability to handle large volumes of fine powder with minimal downtime, reducing the risk of material loss and improving overall production throughput. The working scene in such applications often involves continuous operation, with the system designed to operate 24/7 to meet the demands of high-production environments. The systems are also adaptable to different scales, from small-scale laboratory applications to large-scale industrial operations, making them versatile solutions for various silica fume handling needs.
Technical Advantages and System Integration
The choice of a pneumatic conveying system for silica fume is driven by several technical advantages that address the unique challenges of handling this material. Unlike mechanical conveying methods, pneumatic systems offer better control over particle flow, reducing the risk of segregation and ensuring consistent material quality. The absence of moving parts also minimizes maintenance requirements and extends the system's operational lifespan. Furthermore, the system's ability to handle materials with high moisture content or those that are prone to clumping makes it an ideal solution for silica fume, which can be sensitive to environmental conditions. HeadPowder's systems are designed with integration in mind, allowing seamless connection to existing production lines and storage facilities. The company's expertise in customizing systems to meet specific operational requirements ensures that clients receive tailored solutions that optimize performance and efficiency. The working scene characteristics, such as the need for precise material control and minimal contamination, are addressed through advanced control systems and material handling technologies, providing a reliable and efficient solution for silica fume transportation.
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted name in the design and implementation of pneumatic conveying systems for silica fume. The company's commitment to innovation and quality ensures that its systems meet the highest standards of performance and reliability. By understanding the core principles and working scene characteristics of these systems, industries can leverage advanced material handling solutions to enhance their operational efficiency and product quality. The company's expertise in customizing systems to specific applications, combined with its focus on operational efficiency and minimal maintenance, makes it a preferred choice for businesses seeking reliable and effective silica fume transportation solutions.




