Ammonia fertilizer, as a vital component in modern agricultural practices, demands efficient and reliable transportation solutions to ensure timely delivery and optimal application. The ammonia fertilizer pneumatic conveying system, engineered by Shandong HeadPowder Engineering Co., Ltd. (referred to as HeadPowder), is a specialized equipment designed to meet the high-performance requirements of ammonia fertilizer handling and transportation. This article will explore the principles of the system and the characteristics of its working scenes, offering a comprehensive overview of this advanced technology.
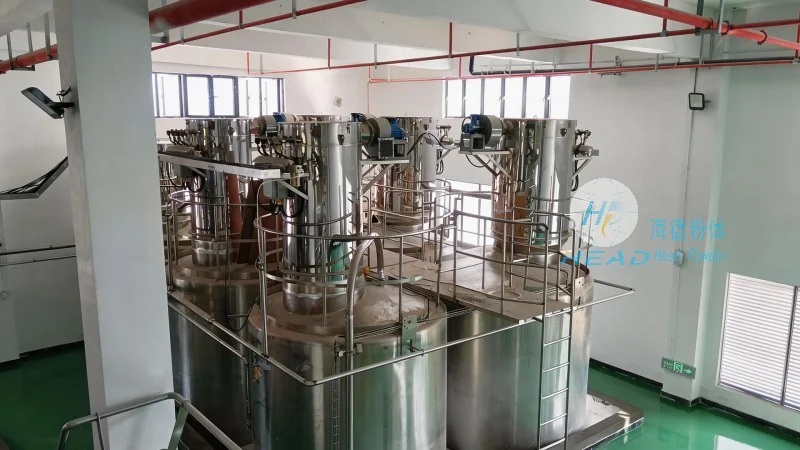
Company Overview and Core Technology
HeadPowder, headquartered in Shandong, China, is a leading manufacturer in the pneumatic conveying systems industry. With decades of experience and continuous innovation, the company has established itself as a trusted provider of ammonia fertilizer handling solutions. The ammonia fertilizer pneumatic conveying system is a product of HeadPowder's core technology, integrating advanced engineering design and robust manufacturing capabilities to deliver high-performance and reliable performance. The system is engineered to handle the unique properties of ammonia fertilizer, such as its high moisture content, corrosive nature, and the need for precise control during transportation.
The Working Principle of the Ammonia Fertilizer Pneumatic Conveying System
The ammonia fertilizer pneumatic conveying system operates based on the principle of pneumatic transport, which utilizes air or gas to move bulk materials through a pipeline. The system typically comprises several key components: a feeder, a conveying line, a separator, and a discharge device. The feeder, often a rotary valve or screw feeder, feeds ammonia fertilizer into the conveying line at a controlled rate. The conveying line, constructed from corrosion-resistant materials like stainless steel or specialized alloys, transports fertilizer particles along with the air flow. The separator, equipped with a cyclone or bag filter, separates fertilizer from the air stream at the end of the line, ensuring clean discharge without contamination. The discharge device then collects the fertilizer for further processing or application.
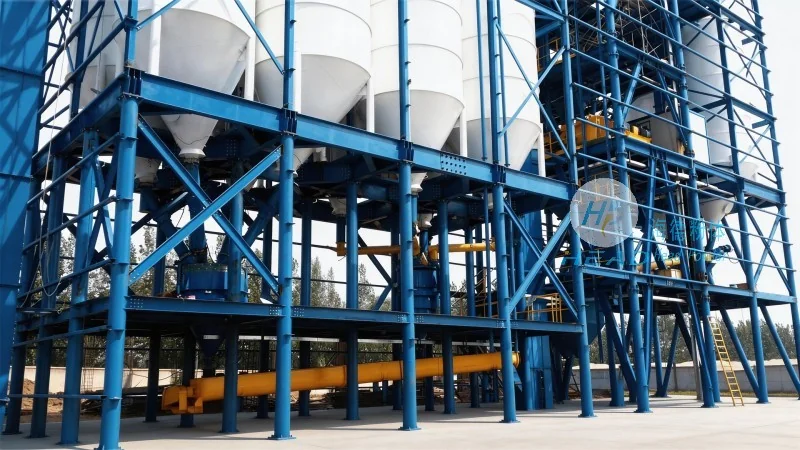
Key Components and Their Functions
Each component of the ammonia fertilizer pneumatic conveying system plays a critical role in ensuring efficient and safe operation. The feeder ensures consistent and controlled flow of ammonia fertilizer into the system. The conveying line, optimized for diameter and length, minimizes pressure drop and maximizes conveying efficiency. The separator effectively removes fertilizer particles from the air, preventing dust and moisture from entering downstream equipment. The discharge device, such as a rotary valve or gate valve, controls fertilizer release, enabling precise dosing and preventing blockages.
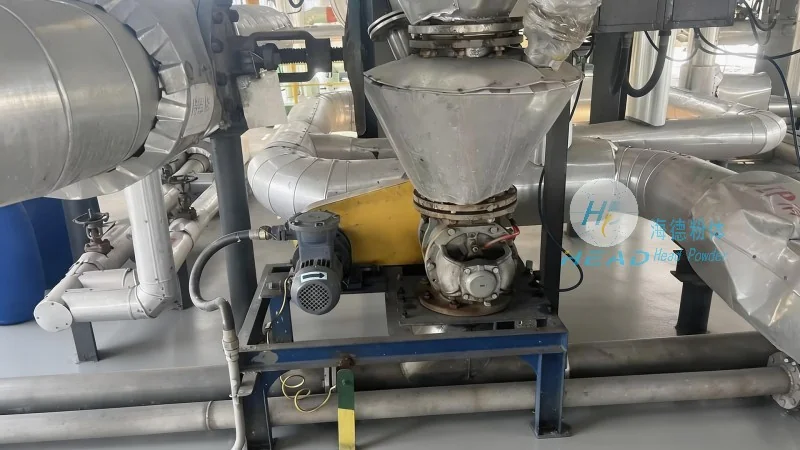
Working Scene Characteristics of the System
The ammonia fertilizer pneumatic conveying system is widely applied in various working scenes, including fertilizer production plants, storage facilities, and distribution centers. In fertilizer production plants, the system transports raw materials like urea or ammonium nitrate from storage silos to the production line. In storage facilities, it moves ammonia fertilizer from bulk tanks to loading trucks or storage silos. In distribution centers, the system transfers fertilizer from the production site to end-users, ensuring timely and efficient delivery. The system's adaptability to diverse working scenes makes it a versatile solution for ammonia fertilizer handling, catering to the agricultural industry's varied needs.
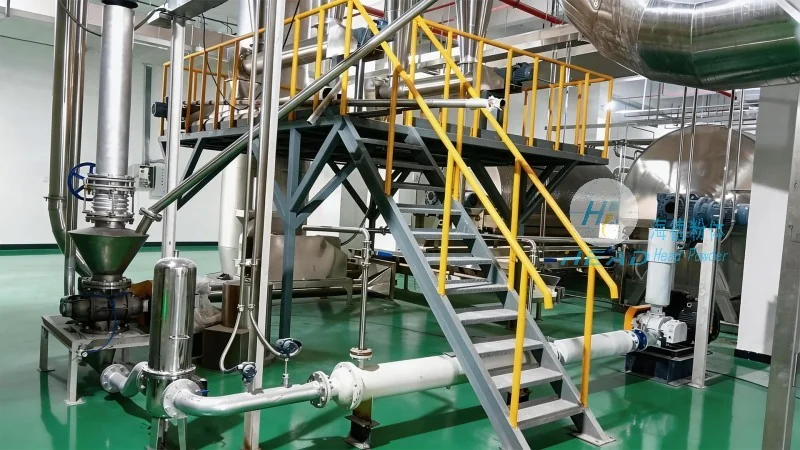
Advantages and Applications
The ammonia fertilizer pneumatic conveying system offers advantages over traditional methods like belt conveyors or bucket elevators, including high conveying efficiency, low maintenance costs, and the ability to handle corrosive, moisture-rich materials. It is particularly suitable for applications where hygiene and product purity are critical, such as high-quality ammonia fertilizer production. The system's compact design and easy installation make it ideal for space-constrained environments, like small-scale fertilizer production facilities or storage areas.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. (HeadPowder) has developed an advanced ammonia fertilizer pneumatic conveying system that combines efficient technology with robust design. The system operates based on pneumatic transport principles and is equipped with key components ensuring reliable and safe operation. With its wide range of working scene applications and numerous advantages, the system is a valuable asset for the agricultural industry, providing efficient and reliable transportation of ammonia fertilizer. HeadPowder's commitment to quality and innovation ensures the system meets the highest performance and reliability standards, making it a trusted choice for ammonia fertilizer handling and transportation.




