Welcome to Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer specializing in advanced material handling solutions. Our focus is on providing efficient and reliable bin pump systems that cater to diverse industrial applications. This article delves into the fundamental principles of bin pump technology and explores the key characteristics of its operational environments.
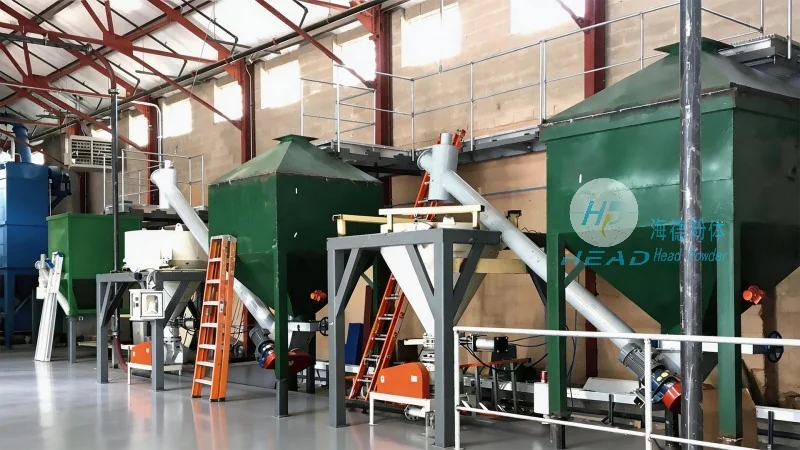
Understanding the Core Principle of Bin Pump Material Handling
At the heart of bin pump material handling equipment lies a sophisticated mechanism designed to transport bulk materials with precision and efficiency. The bin pump, also known as a pressure-type feeder, operates by creating a pressure differential within a hopper or storage bin. This differential forces the material to flow into a delivery pipe under controlled pressure. The system typically includes a hopper, a plunger or piston mechanism, and a valve assembly that regulates the material discharge. As the plunger moves, it compresses the material, generating the necessary pressure to push the material through the pipeline. This method ensures consistent flow rates and minimizes material degradation, making it ideal for handling a wide range of bulk materials such as powders, granules, and fine particles.
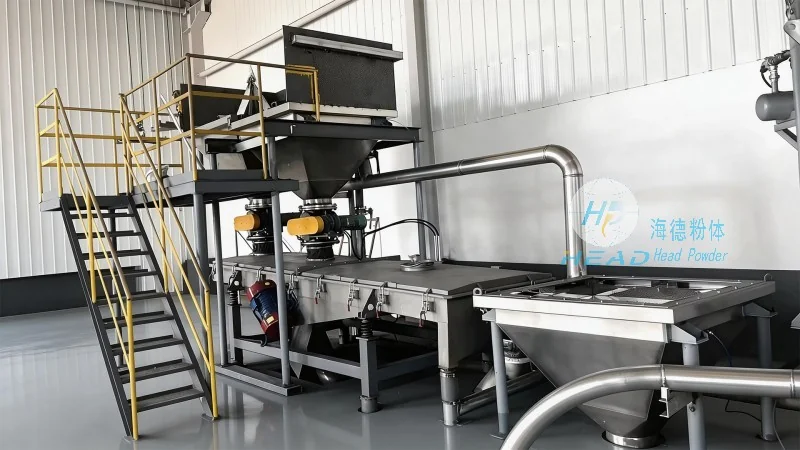
Key Working Scene Characteristics of Bin Pump Systems
The operational characteristics of bin pump systems are tailored to meet the demands of various industrial settings. These systems are commonly employed in scenarios where precise material control is critical, such as in pharmaceutical manufacturing, food processing, and chemical processing industries. The bin pump's ability to handle fine powders without clogging or segregation is a significant advantage in these environments. Additionally, the system's compact design allows for integration into existing production lines, reducing space requirements and enhancing overall workflow efficiency. In applications like cement and mineral processing, the bin pump's high-pressure capabilities enable the transport of abrasive materials over long distances with minimal wear on components. The adaptability of bin pump technology also makes it suitable for use in hazardous environments, where explosion-proof designs and sealed systems are essential for safety compliance.
Applications and Benefits in Industrial Settings
Bin pump material handling equipment is widely utilized across multiple sectors due to its versatility and efficiency. In the chemical industry, for instance, the system is used to transport reactive powders and granules, ensuring that the material is handled in a controlled manner to prevent contamination or accidents. The food processing sector benefits from the bin pump's ability to maintain sanitary conditions, as the system can be designed with stainless steel components and sealed mechanisms to meet regulatory standards. Similarly, in the pharmaceutical industry, the precision and cleanliness of bin pump systems are crucial for handling active ingredients and ensuring product quality. The benefits of using bin pump technology extend beyond material transport; it also contributes to improved production throughput by reducing downtime associated with material handling and enhancing the overall reliability of the process.
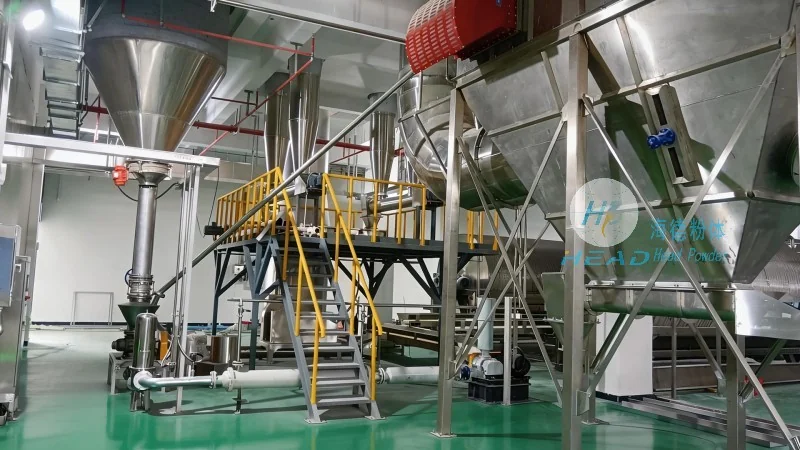
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a reputable enterprise based in China, dedicated to innovation and excellence in material handling solutions. With a strong commitment to quality and customer satisfaction, the company has established itself as a trusted provider of bin pump systems and related equipment. Our team of experienced engineers and technicians continuously researches and develops advanced technologies to meet the evolving needs of the industrial sector. The company's facilities are equipped with state-of-the-art manufacturing and testing equipment, ensuring that every product meets the highest standards of performance and durability. HeadPowder's dedication to sustainability and environmental responsibility is reflected in the design of its bin pump systems, which are engineered to minimize energy consumption and reduce waste during material handling operations. By partnering with HeadPowder, industries can enhance their operational efficiency while adhering to industry best practices and regulatory requirements.




