HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced material handling systems. This article focuses on the automatic powder bulk bag unloading and material conveying line, an essential solution for industries dealing with bulk powders, such as food, pharmaceuticals, chemicals, and construction materials. The system integrates efficient bulk bag opening, material transfer, and conveying processes to enhance operational efficiency and safety.
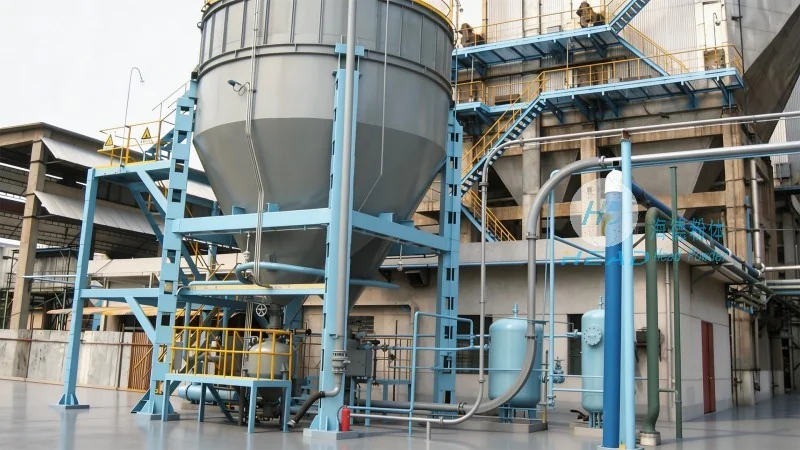
Core Principle of the System
The automatic powder bulk bag unloading and material conveying line operates on a principle of integrated automation, combining mechanical, pneumatic, and control technologies to streamline the entire material handling process. At its core, the system is designed to handle bulk bags (also known as FIBCs or flexible intermediate bulk containers) with precision, ensuring minimal material loss and maximum throughput. The process typically begins with the placement of a bulk bag onto a designated loading platform. The system then uses a combination of lifting mechanisms and pneumatic valves to open the bag, allowing the powder to flow into a hopper or storage vessel. Simultaneously, the conveying section of the line, which may include screw conveyors, belt conveyors, or pneumatic ducts, transports the material to the desired destination, such as a silo, storage tank, or processing unit. The control system, often equipped with sensors and programmable logic controllers (PLCs), monitors the entire operation, adjusting parameters like flow rate and speed to maintain optimal performance. This integrated approach minimizes manual intervention, reduces labor costs, and enhances overall operational efficiency.
Working Scene Characteristics and Application Scenarios
The automatic powder bulk bag unloading and material conveying line is particularly suited for industrial environments where handling large volumes of powders is critical. Its working scene characteristics include high throughput, low maintenance requirements, and robust design to withstand harsh conditions. The system is commonly used in the following scenarios:
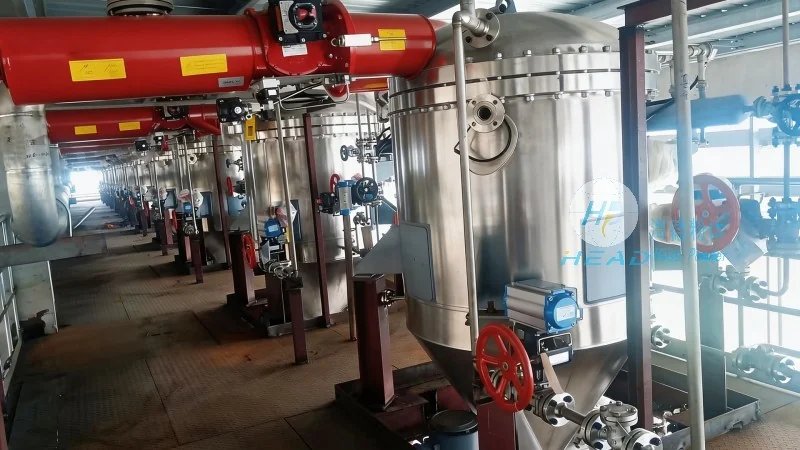
1. Food and Beverage Industry: For handling ingredients like flour, sugar, and spices, where hygiene and contamination control are paramount. The system’s enclosed design and easy cleaning features make it ideal for food-grade applications.
2. Pharmaceutical Industry: In pharmaceutical manufacturing, where precision and cleanliness are essential. The system’s ability to handle sensitive powders without cross-contamination ensures compliance with regulatory standards.
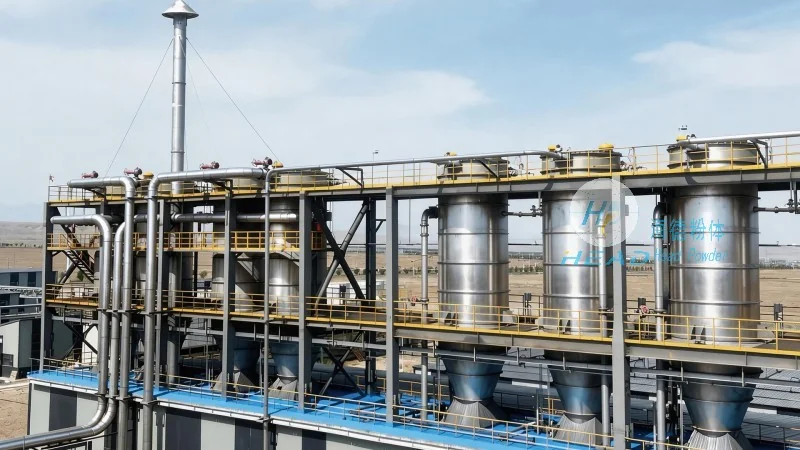
3. Chemical Industry: For transporting bulk chemicals, including powders used in manufacturing, where safety and material integrity are critical. The system’s robust construction and explosion-proof options make it suitable for hazardous environments.
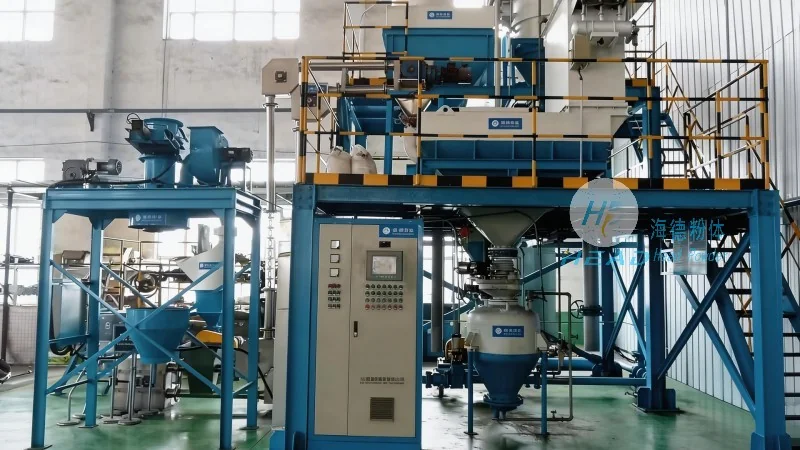
4. Construction Materials Industry: For handling raw materials like cement, sand, and gravel, where high capacity and durability are required. The system’s ability to handle abrasive materials without wear and tear extends its operational life.
Company Information and Professional Support
Shandong HeadPowder Engineering Co., Ltd., the manufacturer of this advanced system, is committed to providing high-quality engineering solutions tailored to the specific needs of each client. With a team of experienced engineers and technicians, the company offers comprehensive support, including system design, installation, and maintenance services. HeadPowder’s expertise in material handling technology ensures that clients receive a reliable and efficient solution that meets their operational requirements. The company’s facilities in Shandong, China, are equipped with state-of-the-art equipment and quality control measures, ensuring that every product meets the highest standards of performance and safety. By choosing HeadPowder, industries can enhance their material handling processes, reduce operational costs, and improve overall productivity.




