Automatic weighing powder pneumatic conveying machines represent a sophisticated solution in material handling, particularly for industries dealing with bulk powders. These systems integrate precise weighing mechanisms with pneumatic transport technology to ensure accurate and efficient material transfer. The core principle revolves around the use of air as the conveying medium, which propels powder particles through a network of pipes and components. The automatic weighing feature allows for real-time measurement of the material being transported, enabling precise control over dosing and inventory management.
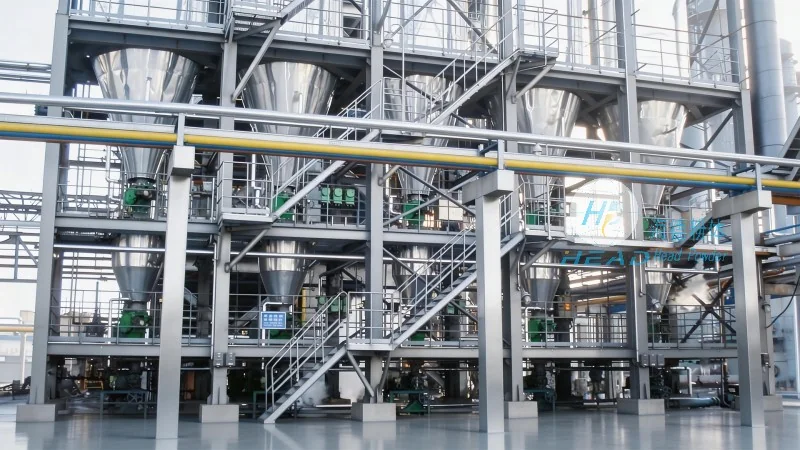
Core Working Principle of the System
The operation of an automatic weighing powder pneumatic conveying machine begins with the feeding of the powder into the system. A hopper or feeder supplies the material, which is then introduced into a pressure or vacuum system depending on the specific application. The machine uses either positive pressure (air is blown into the system) or negative pressure (air is drawn out) to move the powder. The weighing unit, typically a load cell or a scale integrated into the conveyor line, continuously monitors the mass of the material being conveyed. This data is processed by a control system that adjusts the air flow rate or the feeding speed to maintain the desired weight per batch. The system can handle various powder types, including fine powders, granules, and even bulk materials, adapting to different particle sizes and flow characteristics.
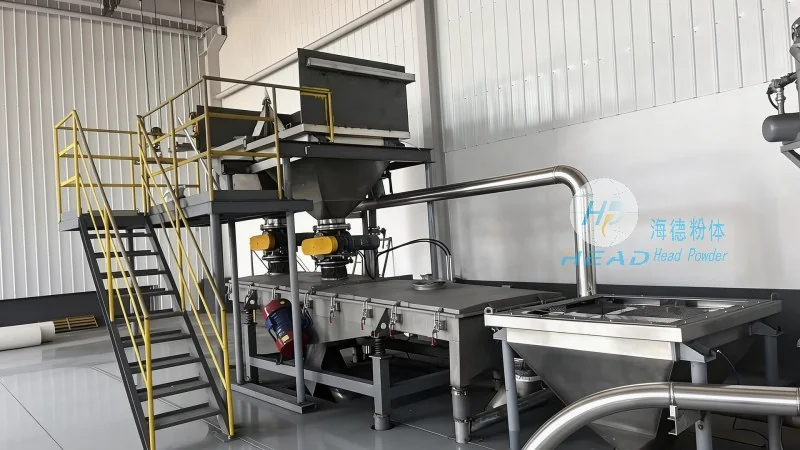
Key Components and Their Functions
Several critical components work in tandem to ensure the efficient operation of the automatic weighing powder pneumatic conveying machine. The feeding hopper is designed to store and meter the powder at a controlled rate. It often includes a rotary valve or a screw feeder to regulate the flow into the conveying line. The conveying line itself consists of stainless steel or other corrosion-resistant materials to accommodate different powder properties. The air compressor or vacuum pump provides the necessary pressure or suction to move the powder. The weighing scale, usually a load cell, is strategically placed in the line to capture the weight of the material as it passes. The control panel or PLC (Programmable Logic Controller) processes the weight data and adjusts the system parameters in real-time. Additionally, filters and cyclones are used to separate the powder from the air, ensuring clean operation and preventing dust accumulation.
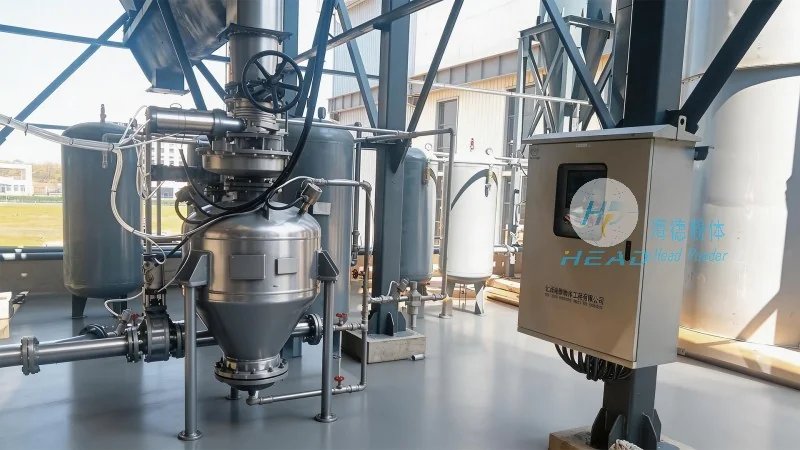
Working Scene Characteristics and Applications
The automatic weighing powder pneumatic conveying machine is widely used in various industrial sectors due to its versatility and precision. In the pharmaceutical industry, it is employed for the handling of active pharmaceutical ingredients (APIs) and excipients, where accuracy and contamination control are paramount. The food and beverage industry utilizes these systems for transporting powders like flour, sugar, and spices, ensuring consistent quality and preventing cross-contamination. The chemical industry benefits from the ability to handle hazardous or reactive powders safely, with the system's enclosed design minimizing exposure risks. In the cement and construction sectors, it aids in the efficient transfer of bulk cement and other building materials. The machine's adaptability to different operating environments, whether in a cleanroom or a heavy-duty industrial setting, makes it suitable for diverse applications. Its ability to handle both low and high flow rates, as well as varying particle sizes, further enhances its utility across multiple industries.
Advantages and Benefits for Industrial Operations
Implementing an automatic weighing powder pneumatic conveying machine offers several advantages that contribute to improved operational efficiency and cost savings. The primary benefit is the enhanced accuracy in material measurement, which reduces waste and ensures consistent product quality. The system's ability to operate continuously without manual intervention minimizes labor costs and increases productivity. The enclosed design of the machine helps maintain a clean and safe working environment, reducing the risk of dust explosions and improving workplace safety. Additionally, the system's flexibility allows for easy integration with existing production lines, minimizing downtime during installation. The real-time monitoring and control features enable operators to quickly respond to any deviations in the process, ensuring smooth and reliable operation. Over time, the investment in such a system can lead to significant reductions in material handling costs and improved overall operational efficiency.
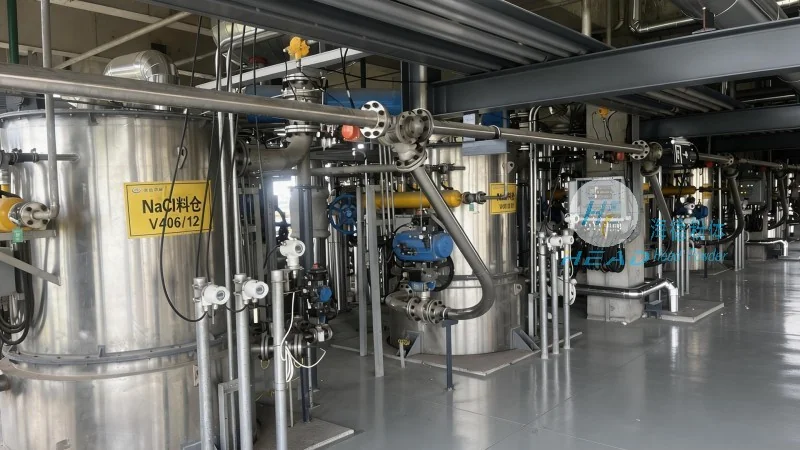
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer specializing in the design, development, and production of advanced powder handling equipment. With a strong presence in China, particularly in Shandong, the company has built a reputation for delivering high-quality, reliable, and innovative solutions tailored to the needs of various industries. The company's commitment to research and development ensures that its products incorporate the latest technological advancements, meeting the evolving demands of the market. HeadPowder's team of experts works closely with clients to understand their specific requirements, providing customized solutions that enhance operational efficiency and product quality. The company adheres to strict quality control standards, ensuring that each product meets or exceeds industry benchmarks. By leveraging its expertise and experience, headpowder continues to be a trusted partner for businesses seeking efficient and effective powder handling solutions.




