High-pressure pneumatic conveying systems represent a sophisticated method for transporting bulk materials over long distances or within industrial facilities. These systems utilize compressed air or other gases to move powders, granules, and other particulate materials through a pipeline network, offering advantages such as non-contact material handling, reduced contamination risk, and the ability to operate in diverse environments. The technology has become increasingly vital in sectors like pharmaceuticals, food processing, and chemical manufacturing, where maintaining product integrity and process efficiency is paramount.
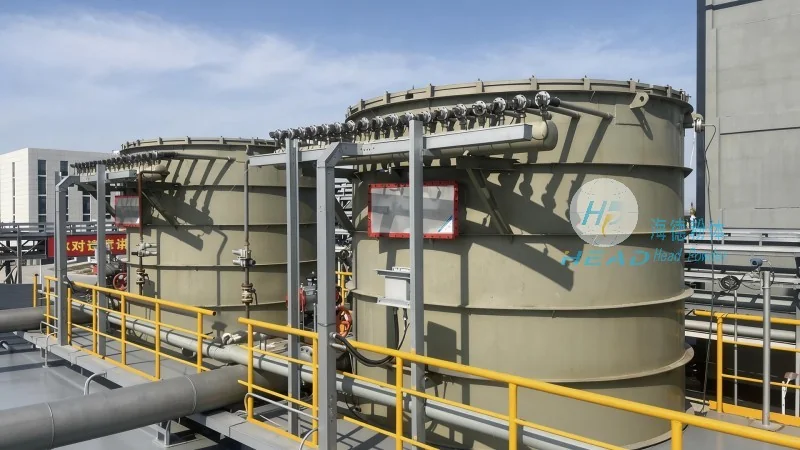
Key Components of High-Pressure Pneumatic Conveying Systems
At the core of a high-pressure pneumatic conveying system are several critical components that work in tandem to ensure efficient material transport. The primary elements include a compressor or blower to generate the necessary air pressure, a material feed hopper or feeder to introduce the bulk material into the system, a pipeline network that conveys the material, and a receiver or discharge hopper where the material is collected. Additionally, components such as filters, silencers, and pressure regulators are often integrated to enhance system performance and safety. The compressor is typically the most energy-intensive component, responsible for maintaining the high pressure required for effective material movement. The material feeder, which can be a rotary valve, screw feeder, or vibrating feeder, ensures a consistent flow of material into the pipeline, preventing blockages and maintaining system stability. The pipeline itself is usually made of stainless steel or other corrosion-resistant materials to accommodate various material types and prevent contamination. Filters are essential for capturing fine particles and preventing them from entering the compressor or other downstream equipment, while silencers reduce noise levels associated with high-pressure air operation. Pressure regulators help maintain a stable pressure within the system, ensuring consistent material transport rates.
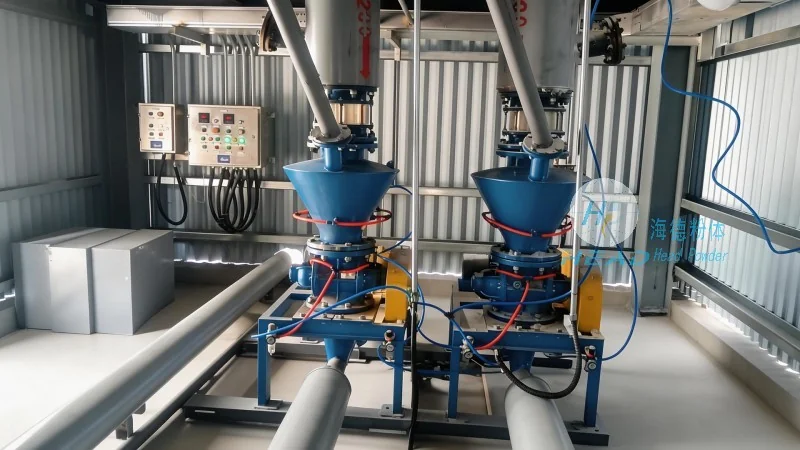
Working Principles of High-Pressure Pneumatic Conveying
The operation of a high-pressure pneumatic conveying system is based on the principle of air flow and pressure differentials. In a typical system, the compressor generates high-pressure air, which is then directed into the pipeline. The material is introduced into the pipeline at a specific point, often via a feeder, and is entrained by the high-velocity air stream. The air and material mixture travels through the pipeline under pressure, with the air providing the necessary force to move the material. The system can operate in either positive pressure or negative pressure modes, depending on the application and material characteristics. In positive pressure systems, the entire pipeline is maintained at a pressure above atmospheric, ensuring that material does not escape and that the system can handle abrasive or dusty materials. Negative pressure systems, on the other hand, create a vacuum in the pipeline, drawing material from a hopper or silo and moving it to a receiver. The choice between positive and negative pressure depends on factors such as material properties, distance to be conveyed, and the need for containment. The velocity of the air in the pipeline is a critical parameter, as it must be sufficient to entrain the material without causing excessive wear on the pipeline or components. The system's design must account for the specific characteristics of the material being conveyed, including its density, particle size, and flowability, to ensure optimal performance and prevent issues like clogging or material degradation.
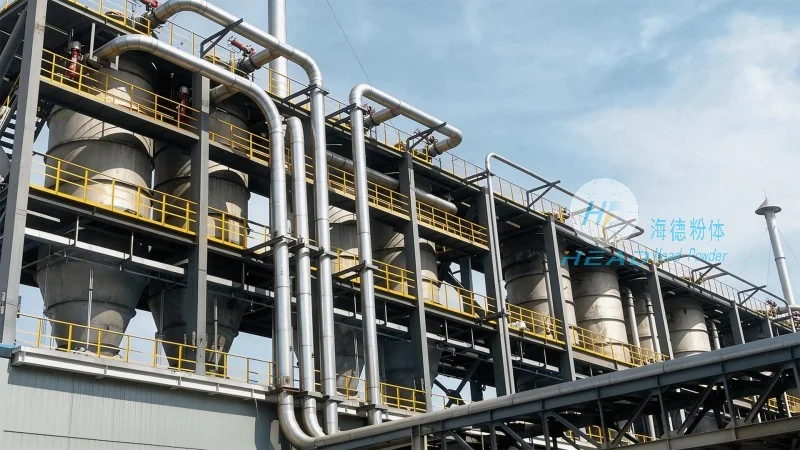
Applications and Benefits of High-Pressure Pneumatic Conveying
High-pressure pneumatic conveying systems are widely used across various industries due to their versatility and efficiency. In the pharmaceutical industry, these systems are employed to transport active pharmaceutical ingredients (APIs) and other sensitive materials, ensuring that the materials remain sterile and free from contamination. The non-contact nature of the system minimizes the risk of cross-contamination, which is crucial in pharmaceutical manufacturing. In food processing, high-pressure pneumatic conveying is used to handle powders like flour, sugar, and spices, maintaining product quality and preventing the introduction of foreign particles. The system's ability to operate in a clean environment makes it suitable for food-grade applications. The chemical industry also benefits from high-pressure pneumatic conveying, as it can handle corrosive or hazardous materials safely. The system's containment features, such as sealed pipelines and filters, help prevent the release of harmful substances into the environment. Additionally, the system's ability to transport materials over long distances without the need for multiple transfer points makes it ideal for large-scale industrial operations. The benefits of high-pressure pneumatic conveying extend beyond material transport, as the technology can also be used for dust collection and material recovery in certain applications. Overall, the system offers a reliable and efficient solution for bulk material handling, with the ability to adapt to a wide range of material types and operational requirements.
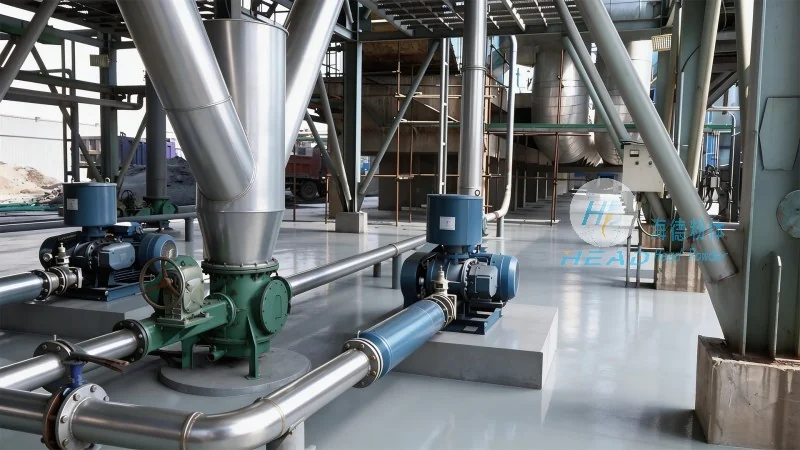
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of high-pressure pneumatic conveying systems and related equipment. With its headquarters located in Shandong, China, the company has established itself as a trusted partner in the bulk material handling industry. HeadPowder specializes in designing, manufacturing, and installing customized pneumatic conveying solutions tailored to the specific needs of its clients. The company's products are known for their durability, efficiency, and compliance with industry standards, making them suitable for a wide range of applications. HeadPowder's commitment to quality and innovation has enabled it to serve clients in various sectors, including pharmaceuticals, food processing, chemicals, and more. The company's team of experienced engineers and technicians ensures that each system is designed and manufactured to meet the highest standards of performance and reliability. HeadPowder's dedication to customer satisfaction and technical excellence has made it a preferred choice for businesses seeking reliable and efficient bulk material handling solutions.




