HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced dust-free automatic pneumatic conveying systems. These systems are engineered to efficiently transport bulk materials in industrial settings while maintaining a clean and controlled environment. The core technology behind these systems involves the use of air pressure to move materials through a sealed pipeline network, ensuring minimal dust generation and contamination. This approach is particularly crucial in industries such as food processing, pharmaceuticals, and chemical manufacturing, where product purity and operational safety are paramount.
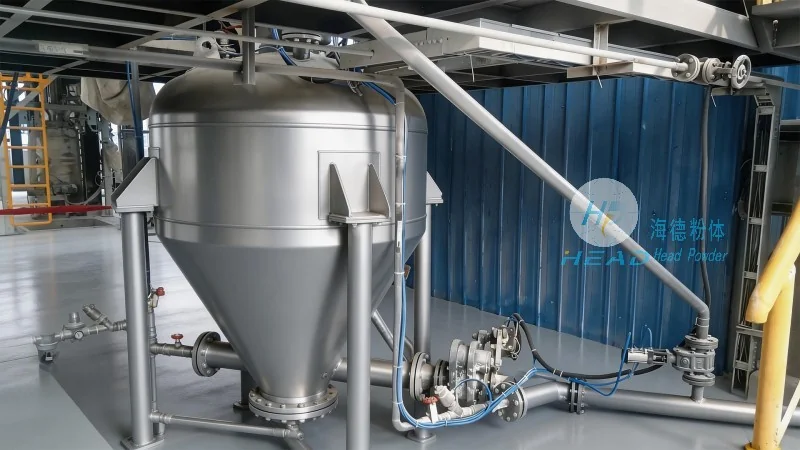
Key Structural Components of the Pneumatic Conveying System
The dust-free automatic pneumatic conveying system consists of several critical components that work in tandem to achieve efficient material transport. The main elements include a material hopper or feeder, which holds the bulk material and regulates its flow into the system. A rotary valve or feeder is typically used to control the discharge of material from the hopper, ensuring a consistent feed rate. The conveying line itself is made of high-quality, airtight materials, often stainless steel or specialized plastic, to prevent leaks and maintain the dust-free environment. At the receiving end, a receiver or silo collects the material, and a discharge valve or outlet allows for controlled release. Additionally, a filter system is integrated to capture any fine particles that may escape, ensuring that the air expelled is clean and compliant with environmental regulations. The system is powered by a blower or compressor, which generates the necessary air pressure to move the material through the pipeline. Control panels and sensors are also included to monitor and adjust the system's performance in real-time, enhancing operational efficiency and reliability.
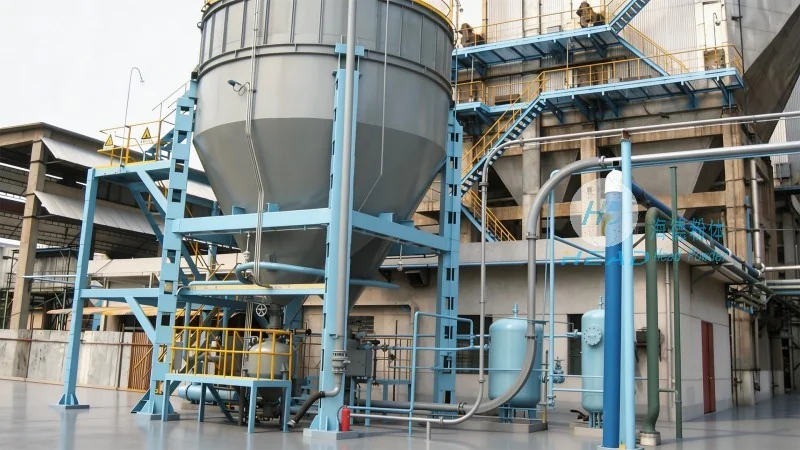
Working Principle of the Pneumatic Conveying Process
The operation of the dust-free automatic pneumatic conveying system follows a systematic process. Initially, the bulk material is loaded into the material hopper. The rotary valve then regulates the flow of material into the conveying line. Simultaneously, the blower generates a high-pressure airflow that travels through the pipeline. As the material enters the line, it is entrained by the air stream and carried to the receiving end. The filter system continuously removes any particles from the air, preventing contamination and ensuring the system operates in a clean environment. At the destination, the material is deposited into the receiver, and the air is filtered before being released back into the environment. The control system monitors parameters such as pressure, flow rate, and material level, allowing for automatic adjustments to maintain optimal performance. This closed-loop system minimizes human intervention, reduces labor costs, and enhances overall productivity.
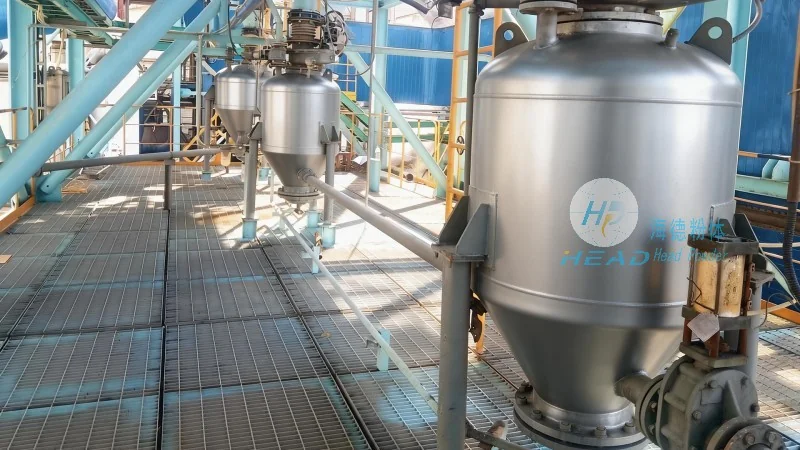
Benefits of Using Dust-Free Pneumatic Conveying Systems
Implementing a dust-free automatic pneumatic conveying system offers numerous advantages for industrial operations. Firstly, it significantly reduces dust emissions, improving workplace safety and compliance with environmental regulations. The sealed system prevents material from escaping into the air, protecting both workers and the surrounding environment. Secondly, the system enhances product quality by minimizing contamination from external particles. This is especially important in industries where product purity is critical, such as food and pharmaceuticals. Thirdly, the automated nature of the system increases operational efficiency and reduces labor costs. The consistent flow of material and real-time monitoring reduce downtime and improve overall productivity. Additionally, the system is versatile and can handle a wide range of materials, from powders to granules, with minimal adjustments. Its compact design also saves space in industrial facilities, making it suitable for both new installations and retrofit applications. The long-term cost savings from reduced maintenance and increased efficiency further justify the investment in such advanced conveying systems.
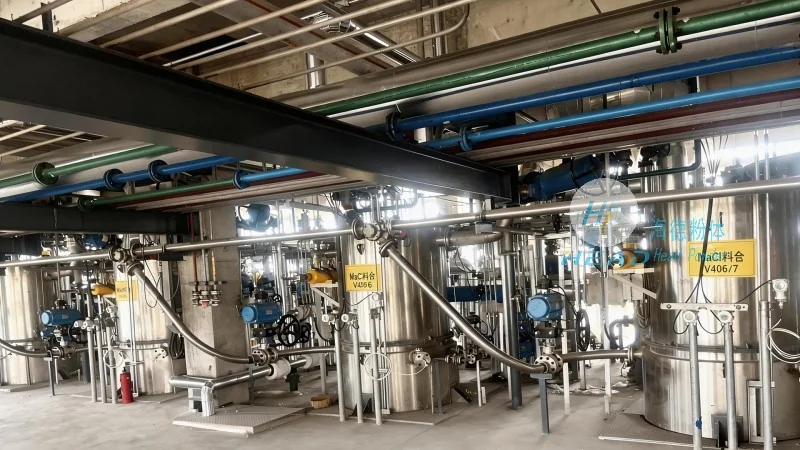
Application Scenarios in Different Industries
Dust-free automatic pneumatic conveying systems are widely used across various industries due to their adaptability and efficiency. In the food and beverage industry, these systems are employed to transport ingredients like flour, sugar, and spices without compromising their quality or safety. The sealed environment prevents cross-contamination and maintains hygiene standards, which are essential for food processing. In the pharmaceutical industry, the system is used to handle active pharmaceutical ingredients (APIs) and other sensitive materials, ensuring that they remain pure and free from contaminants. The dust-free operation is critical to meet stringent regulatory requirements. In the chemical industry, the system transports powders and granules, such as fertilizers or industrial chemicals, while preventing dust explosions and maintaining a safe working environment. The ability to handle hazardous materials safely makes the system invaluable in this sector. Additionally, in the packaging and manufacturing industries, the system is used to convey raw materials to production lines, streamlining the manufacturing process and reducing manual handling. The consistent and reliable material transport enhances overall production efficiency and quality control.




