HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced powder conveying systems for dust extraction stations. This article provides an overview of the key components, operational principles, and structural design of such systems, highlighting their efficiency and reliability in industrial applications.
Company Profile and Background
HeadPowder Engineering Co., Ltd. is a professional enterprise dedicated to providing high-quality powder handling solutions. With a strong focus on innovation and customer satisfaction, the company has established itself as a trusted partner in the industry. HeadPowder's headquarters is located in Shandong, China, where its team of experienced engineers and technicians work tirelessly to develop cutting-edge technologies for powder conveying systems. The company's commitment to quality and precision ensures that every product meets the highest industry standards.
Overview of Dust Extraction Station Powder Conveying Systems
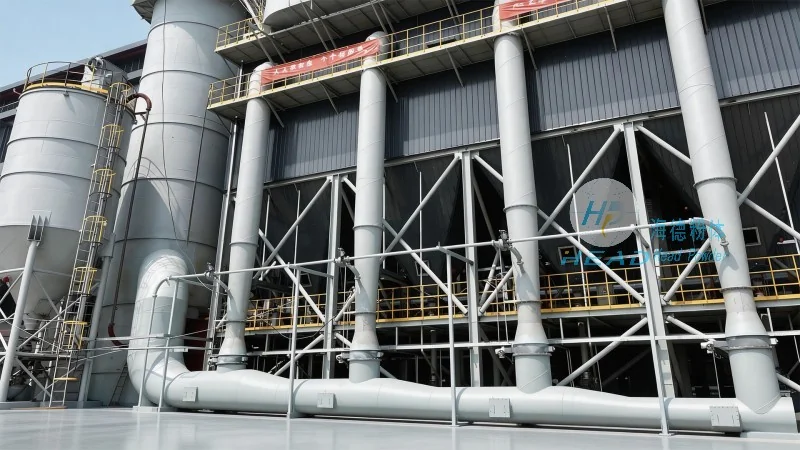
The powder conveying system for dust extraction stations is a critical component in industrial processes that involve the handling of powders, such as in manufacturing, pharmaceuticals, and food processing. These systems are designed to transport powders from the dust extraction point to storage or processing units, ensuring a smooth and efficient workflow. The system typically integrates with dust collection equipment, such as cyclones or bag filters, to collect airborne particles and then transfer them through a sealed pipeline to the designated destination.
Structural Components and Design Principles
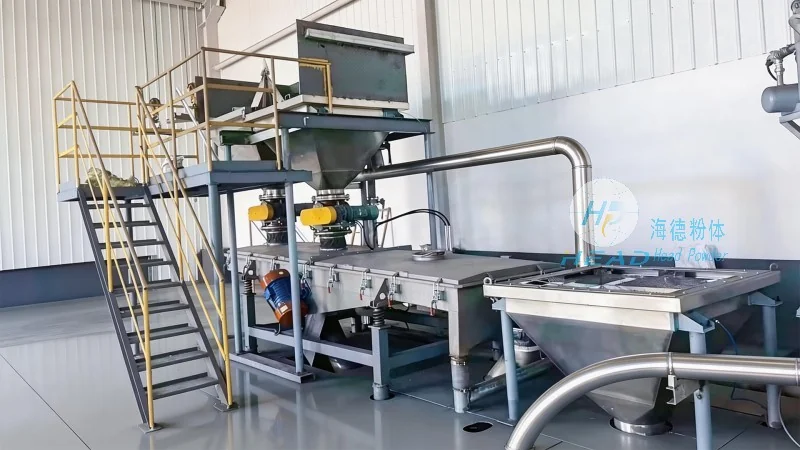
The core structure of a dust extraction station powder conveying system consists of several key components, each playing a vital role in the overall operation. The main parts include the dust collector, conveying pipeline, feeding device, and control system. The dust collector is responsible for capturing airborne particles and separating them from the air stream. The conveying pipeline, often made of stainless steel or other corrosion-resistant materials, ensures the safe and efficient transport of the powder. The feeding device, such as a rotary valve or star feeder, regulates the flow of powder into the pipeline, preventing blockages and maintaining consistent pressure. The control system monitors and adjusts the operation of the conveying system, ensuring optimal performance and safety.
Principle of Operation
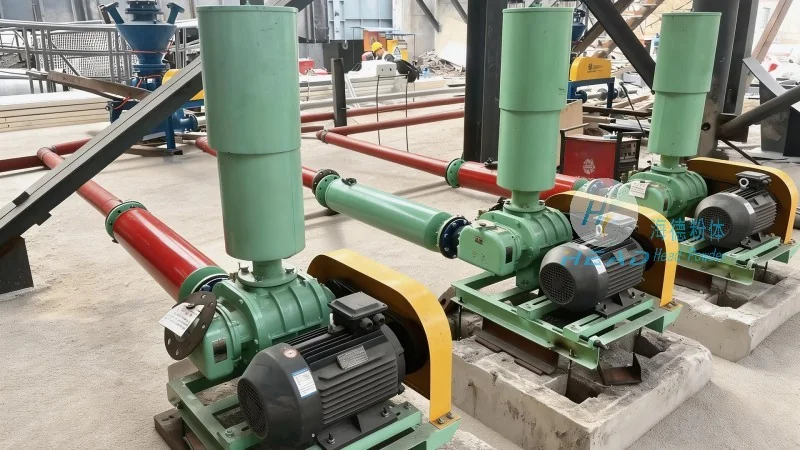
The operation of the powder conveying system follows a systematic process. Initially, the dust collector captures the airborne particles and directs them into the conveying pipeline. The feeding device then introduces the powder into the pipeline at a controlled rate. The system uses either pneumatic or mechanical conveying methods, depending on the specific requirements of the application. Pneumatic conveying systems utilize compressed air to move the powder through the pipeline, while mechanical systems use positive displacement pumps or screw conveyors. The choice of method depends on factors such as the powder's properties, the distance to be conveyed, and the required flow rate. The control system continuously monitors the pressure, flow rate, and other parameters to maintain stable operation and prevent system failures.
Advantages and Applications
Dust extraction station powder conveying systems offer numerous advantages, making them indispensable in various industrial settings. These systems enhance productivity by ensuring a continuous and efficient flow of powders, reducing downtime and improving overall operational efficiency. They also contribute to better workplace safety by containing dust and preventing its release into the environment. The systems are widely used in industries such as chemical manufacturing, pharmaceuticals, food processing, and cement production, where the handling of powders is a critical part of the production process.
Conclusion
HeadPowder Engineering Co., Ltd. provides comprehensive solutions for dust extraction station powder conveying systems, combining advanced technology with expert engineering. By understanding the structural components and operational principles of these systems, industries can optimize their powder handling processes, improve efficiency, and ensure compliance with safety and environmental regulations. With its commitment to quality and innovation, HeadPowder continues to be a leading provider of reliable and efficient powder conveying solutions for customers worldwide.




