Grain bulk pneumatic conveying equipment is a specialized system designed to transport bulk materials like grains, powders, and granules through a pipeline using air or other gases as the conveying medium. This technology offers a highly efficient and flexible method for material handling in various industrial applications, from agricultural processing to food and chemical industries. The core of such equipment lies in its ability to move materials without direct contact with mechanical components, reducing wear and tear while maintaining product integrity.
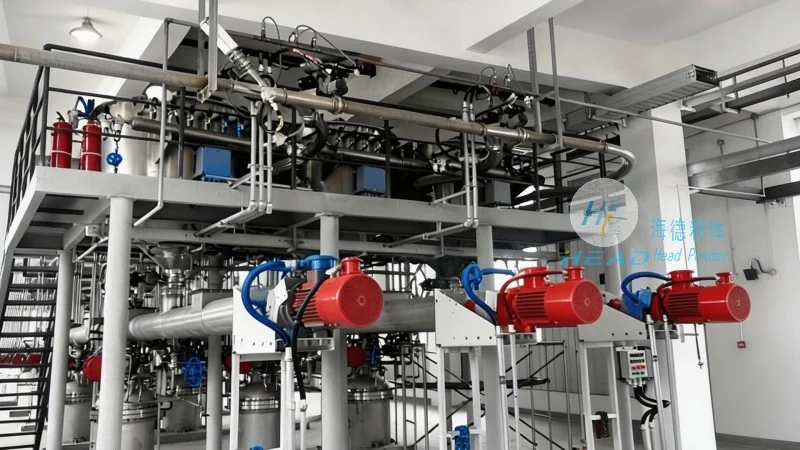
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, development, and production of advanced pneumatic conveying systems. With years of experience in the industry, the company has established itself as a trusted provider of high-quality equipment tailored to meet the diverse needs of clients worldwide. The company’s commitment to innovation and precision engineering ensures that its products deliver optimal performance, reliability, and cost-effectiveness for bulk material handling operations.
Design Principles of Pneumatic Conveying Systems
The design of grain bulk pneumatic conveying equipment is based on fundamental principles of fluid dynamics and material flow. The system typically consists of a blower or compressor that generates the necessary air pressure to move the material through a pipeline. Key components include the hopper for material storage, the conveying line, and the discharge point. The choice of conveying method—whether positive or negative pressure—depends on factors such as material characteristics, distance, and required throughput. Positive pressure systems use compressed air to push material forward, while negative pressure systems create a vacuum to pull material into the line. The design also considers factors like particle size, moisture content, and abrasiveness to ensure efficient and safe operation.
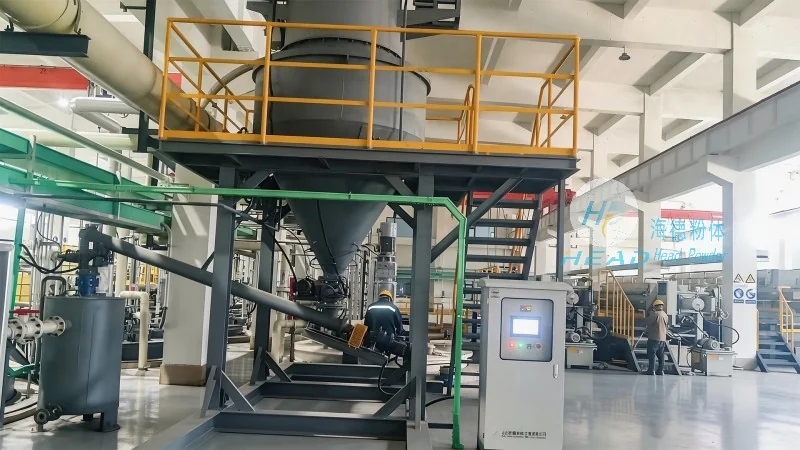
Key Components and Their Functions
Several critical components work together to ensure the smooth operation of pneumatic conveying equipment. The hopper, or feed bin, is responsible for storing and feeding the grain material into the system. It is designed to maintain a consistent flow rate, preventing blockages and ensuring uniform material distribution. The blower or compressor provides the necessary air pressure, with options ranging from rotary lobe blowers to centrifugal compressors, depending on the application requirements. The conveying line, often made of stainless steel or other corrosion-resistant materials, is engineered to withstand the pressure and abrasion from the material. The discharge unit, such as a rotary valve or a dust collector, controls the release of material at the end of the line, preventing dust emissions and maintaining a clean environment. Additionally, the system may include filters and cyclones to separate the conveyed material from the air, ensuring compliance with environmental regulations.
Advantages of Using Pneumatic Conveying Equipment
Grain bulk pneumatic conveying equipment offers numerous advantages over traditional mechanical conveying methods. One of the primary benefits is the ability to transport materials over long distances without the need for multiple transfer points, reducing operational complexity and costs. The system is also highly flexible, allowing for changes in material flow direction or speed without significant modifications. Furthermore, pneumatic conveying minimizes product contamination and degradation, as the material is not in direct contact with metal surfaces or other contaminants. This is particularly important for food-grade grains, where hygiene and product quality are paramount. Additionally, the system can handle a wide range of particle sizes and densities, making it suitable for various applications, from fine powders to large granules. The reduced need for maintenance and lower energy consumption compared to traditional methods also contribute to long-term cost savings.
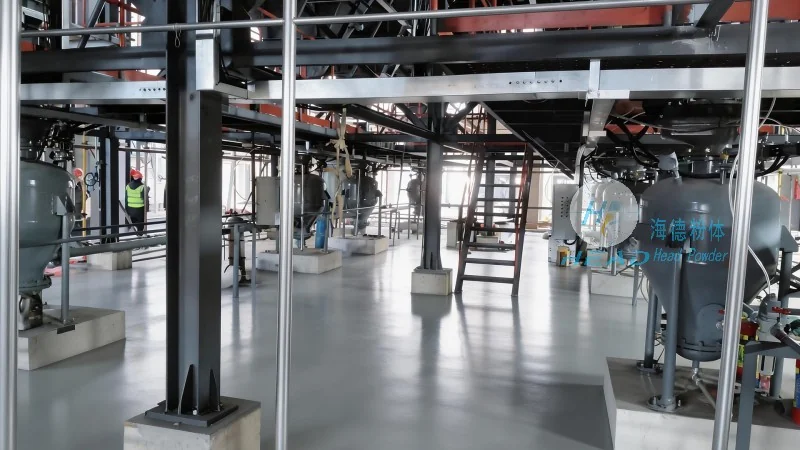
Applications in the Agricultural and Food Industry
HeadPowder’s grain bulk pneumatic conveying equipment is widely used in the agricultural and food processing sectors. In grain storage facilities, the equipment efficiently transfers harvested grains from storage bins to processing plants, ensuring a continuous supply of raw materials. During the milling process, pneumatic conveying systems transport flour and other byproducts between different stages of production, maintaining a clean and hygienic environment. The technology is also applied in the packaging industry, where it helps move bulk ingredients into packaging machines, improving production efficiency and reducing labor costs. Moreover, the system is used in the production of animal feed, where it handles various feed ingredients and additives, ensuring consistent mixing and distribution. The reliability and efficiency of pneumatic conveying equipment make it an essential component in modern food and agricultural operations.
Customization and Solutions for Specific Needs
HeadPowder understands that each client’s material handling requirements are unique. Therefore, the company offers customized pneumatic conveying solutions tailored to specific applications and operational conditions. The design process involves a thorough analysis of the material properties, such as particle size, moisture content, and flow characteristics, as well as the required conveying distance and throughput. Based on this analysis, engineers at HeadPowder develop a system that optimizes performance and minimizes energy consumption. The company also provides after-sales support, including maintenance services and technical assistance, to ensure the long-term reliability of the equipment. By working closely with clients, HeadPowder ensures that its products meet not only current but also future operational needs, providing a sustainable solution for bulk material handling.




