Molybdenum oxide, a critical industrial material, often necessitates specialized handling systems to ensure efficient and safe transport. The molybdenum oxide powder handling system is engineered to address the unique challenges associated with processing this fine powder, including dust control, material flow management, and operational reliability.
Company Overview: HeadPowder
HeadPowder, operating as Shandong HeadPowder Engineering Co., Ltd., is a leading provider of engineering solutions for powder handling and material processing. With a focus on innovation and customer-centric design, the company specializes in developing customized systems tailored to the specific needs of industrial applications. HeadPowder's headquarters is located in Shandong, China, where the company leverages local expertise and advanced manufacturing capabilities to deliver high-quality products.
Core Design Principles of the Molybdenum Oxide Powder Handling System
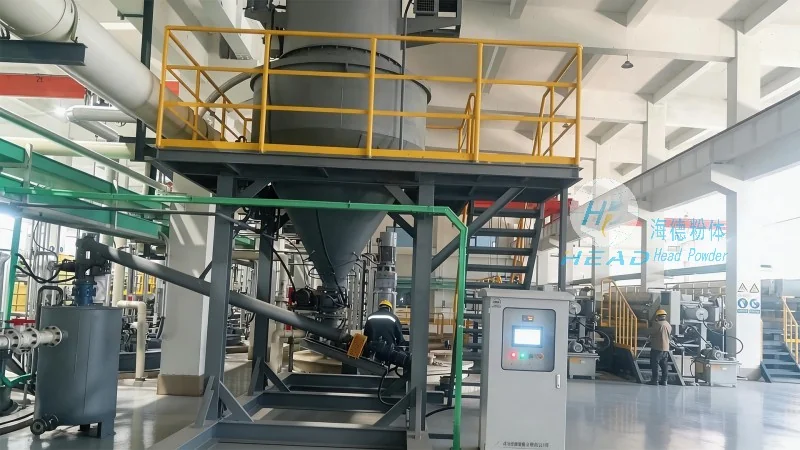
The design of a molybdenum oxide powder handling system is guided by several key principles to ensure optimal performance and safety. Firstly, dust containment is a critical aspect, as molybdenum oxide powder can be hazardous if inhaled. The system incorporates sealed enclosures, air filtration systems, and proper ventilation to minimize exposure risks. Secondly, material flow management is essential to prevent clogging and ensure consistent throughput. This involves the use of specialized hoppers, feeders, and conveyor systems that are engineered to handle the specific properties of molybdenum oxide, such as its particle size and density. Thirdly, the system prioritizes operational safety and ease of maintenance. Features like automatic shut-off valves, emergency stop buttons, and easy-to-access maintenance points are integrated to enhance user safety and reduce downtime.
Key Components and Their Functions
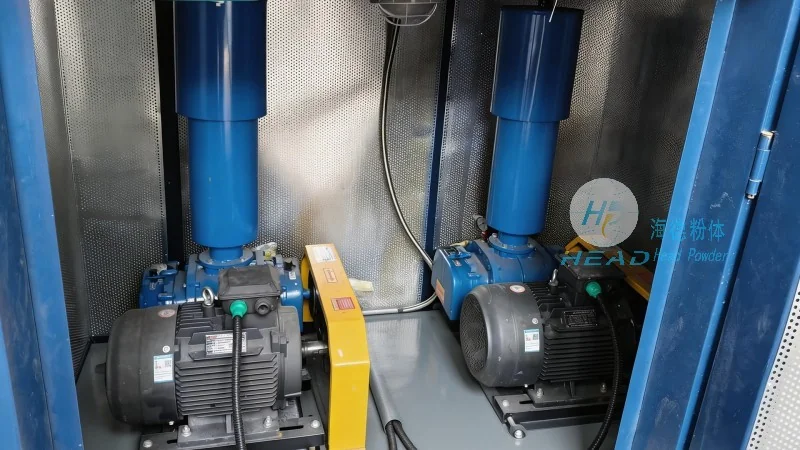
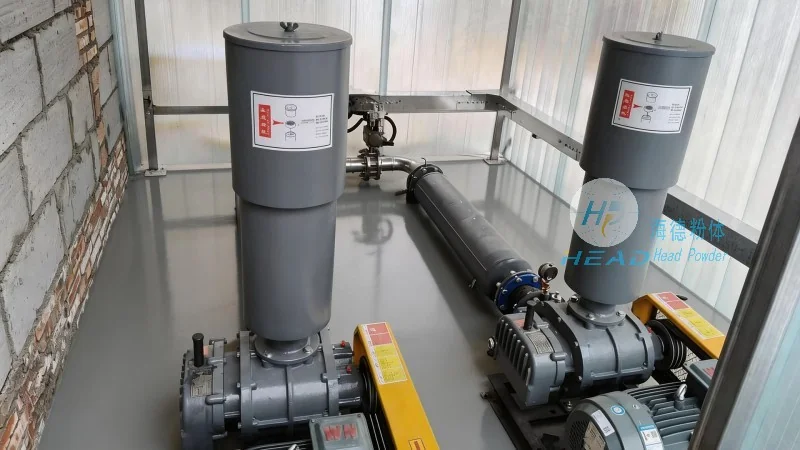
A typical molybdenum oxide powder handling system consists of several interconnected components, each playing a vital role in the overall operation. The primary components include a storage hopper, a feeding mechanism (such as a rotary valve or screw feeder), a conveying system (e.g., pneumatic or mechanical conveyor), and a control panel. The storage hopper is designed to hold the molybdenum oxide powder securely, with a lid that can be sealed to prevent contamination. The feeding mechanism regulates the flow of powder from the hopper to the conveyor, ensuring a consistent and controlled rate. The conveying system transports the powder to the processing or packaging area, with options ranging from pneumatic systems that use compressed air to mechanical systems like belt or screw conveyors. The control panel allows operators to monitor and adjust the system's parameters, such as flow rate and pressure, to maintain optimal performance.
Advantages and Applications
The molybdenum oxide powder handling system offers several advantages that make it indispensable in industrial settings. One of the key benefits is its ability to maintain a clean and safe working environment by effectively containing dust and preventing material loss. This not only enhances workplace safety but also reduces the risk of product contamination. Additionally, the system's design allows for high efficiency and reliability, with minimal downtime due to its robust construction and integrated safety features. The system is widely used in various industries, including chemical manufacturing, metallurgy, and pharmaceuticals, where the handling of fine powders is essential. For example, in the production of molybdenum compounds, the system ensures that the powder is transported smoothly from storage to processing equipment, improving overall production efficiency.




