

What is a Coal Ash Material Handling System? And What Are Its Design Principles?
Coal ash, also known as fly ash or bottom ash, is a byproduct generated during the combustion of coal in power plants. Efficient and reliable handling of this material is crucial for the safe and sustainable operation of thermal power facilities. A coal ash material handling system is a specialized equipment setup designed to transport, store, and manage coal ash from its generation point to disposal or utilization sites. This system plays a vital role in optimizing the overall performance of power generation plants while ensuring environmental compliance and operational safety.
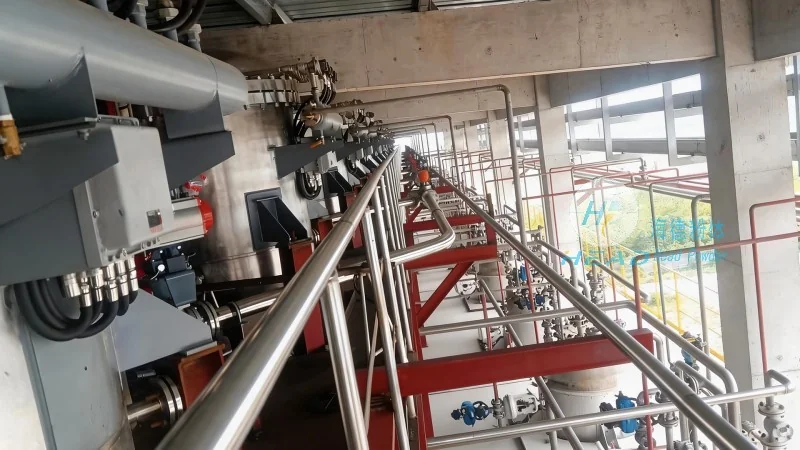
Components and Functions of the Coal Ash Material Handling System
The coal ash material handling system typically consists of several key components, each serving a specific function in the material flow process. The primary components include ash collection devices, conveyor systems, storage silos, and transfer mechanisms. Ash collection devices, such as electrostatic precipitators or baghouse filters, capture the fine ash particles from the flue gas. These collected ash particles are then transferred to the conveyor system, which transports the material to the storage silos. The storage silos are designed to hold large volumes of ash, providing a buffer for downstream processing or disposal. Transfer mechanisms, such as screw conveyors or pneumatic systems, facilitate the movement of ash between different stages of the system. Each component works in coordination to ensure a continuous and efficient flow of coal ash, minimizing downtime and maximizing operational efficiency.
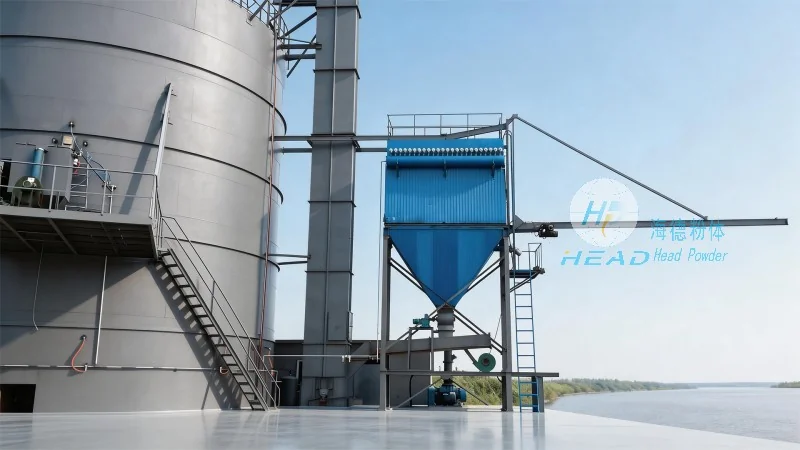
Design Principles of Coal Ash Material Handling Systems
The design of a coal ash material handling system is based on several critical principles that ensure its effectiveness and reliability. The first principle is material compatibility, which involves selecting equipment materials that can withstand the corrosive and abrasive nature of coal ash. Coal ash is known to be chemically reactive and can cause wear and tear on metal surfaces, so materials like stainless steel, high-chrome alloys, or special coatings are often used in the construction of conveyor components and storage silos. The second principle is system integration, which ensures that all components of the system are designed to work together seamlessly. This includes matching the capacity of each component to the overall system throughput, ensuring that the conveyor speed, storage silo volume, and transfer mechanisms are all optimized for the specific ash characteristics and plant requirements. The third principle is safety and environmental compliance, which is paramount in the design of coal ash handling systems. The system must be designed to prevent dust emissions, minimize the risk of ash spills, and comply with local and national environmental regulations. This includes features like dust suppression systems, leak-proof storage silos, and proper ventilation to maintain a safe working environment.
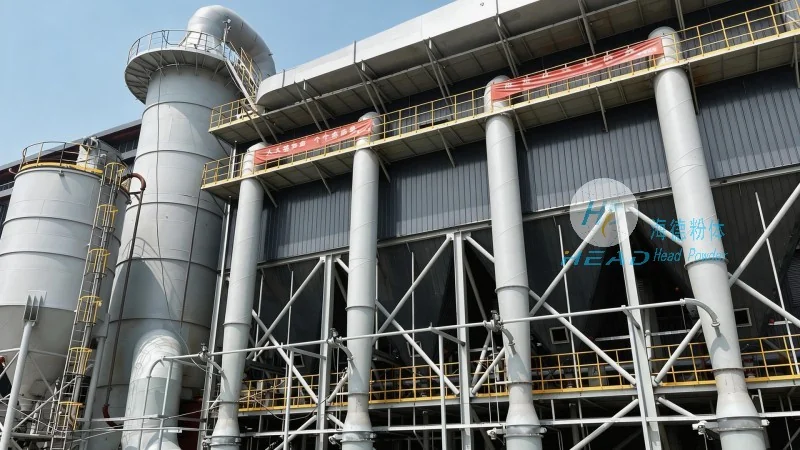
HeadPowder's Expertise in Coal Ash Material Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field of industrial material handling systems, specializes in providing customized coal ash material handling solutions. With years of experience and a deep understanding of the challenges faced by power plants, HeadPowder has developed advanced systems that meet the highest standards of efficiency, reliability, and safety. The company's engineers work closely with clients to assess their specific ash characteristics, plant layout, and operational requirements, then design and manufacture a system that is tailored to their needs. HeadPowder's products include a wide range of equipment, from ash collection devices and conveyors to storage silos and transfer mechanisms, all designed with the latest technology and materials to ensure long-term performance. The company's commitment to quality and customer satisfaction has made it a trusted partner for power plants worldwide, helping them to optimize their ash handling processes and reduce operational costs.
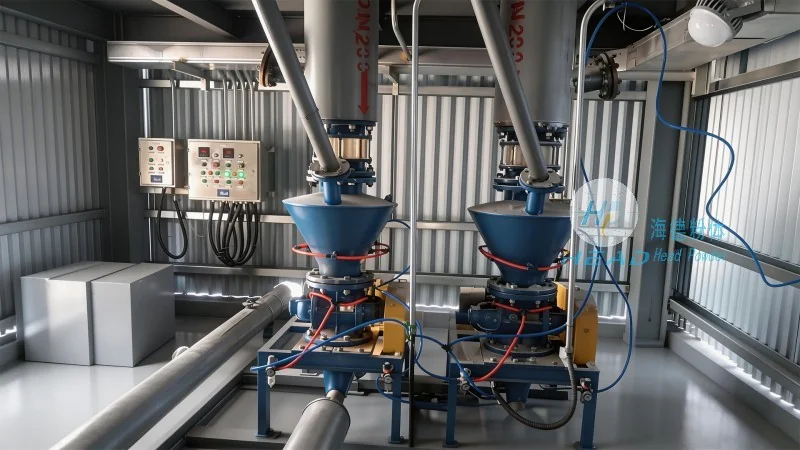
Key Features and Benefits of HeadPowder's Coal Ash Handling Systems
HeadPowder's coal ash material handling systems are equipped with several key features that enhance their performance and reliability. One of the main features is the use of high-quality materials, such as stainless steel and special alloys, which are resistant to corrosion and wear from coal ash. This ensures that the equipment has a long service life and requires minimal maintenance. Another feature is the integration of advanced control systems, which allow for real-time monitoring and control of the system's operations. This includes sensors for ash level, temperature, and pressure, as well as automated controls for conveyor speed and storage silo filling. The advanced control systems help to optimize the system's performance, reduce energy consumption, and prevent operational issues. Additionally, HeadPowder's systems are designed with safety in mind, featuring dust suppression systems, leak-proof storage, and proper ventilation to maintain a safe working environment. The benefits of using HeadPowder's coal ash handling systems are significant. They help power plants to improve their operational efficiency by reducing downtime and increasing throughput. They also help to minimize environmental impact by preventing dust emissions and ensuring proper ash disposal. Furthermore, the systems help to reduce maintenance costs by using durable materials and advanced control systems.