

What is an Automatic Powder Pneumatic Conveying Equipment? And What Are Its Design Principles?
Automatic powder pneumatic conveying equipment is a specialized system designed to transport bulk powder materials through a pipeline using air as the conveying medium. This technology has become increasingly important in various industrial sectors, including pharmaceuticals, food processing, and chemical manufacturing, due to its efficiency, flexibility, and ability to handle a wide range of powder types. Understanding the fundamental principles behind this equipment is crucial for optimizing its performance and ensuring safe and reliable operation.
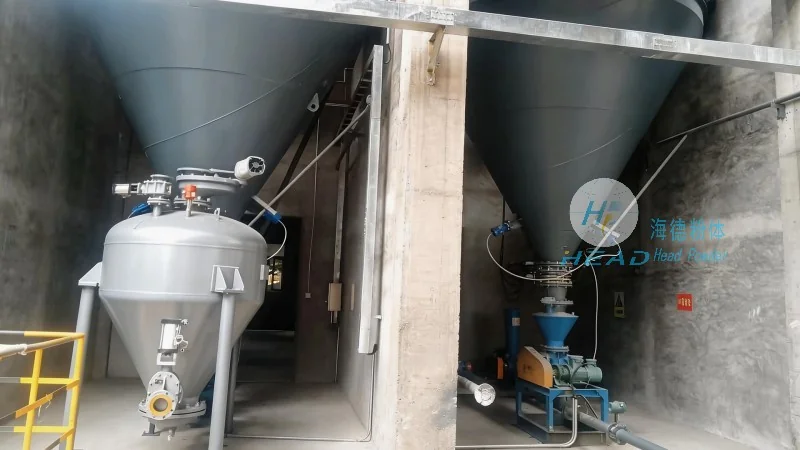
Overview of Automatic Powder Pneumatic Conveying Equipment
At its core, an automatic powder pneumatic conveying system consists of several key components that work in tandem to move powder from a source to a destination. The primary components include a hopper or feeder for material storage, a blower or compressor to generate the air flow, a pipeline network to transport the powder-air mixture, and a receiver or discharge unit to collect the material at the end of the line. The system operates by creating a pressure differential or using vacuum to draw the powder into the pipeline, where it is suspended and carried by the air stream. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance and increasing operational safety.
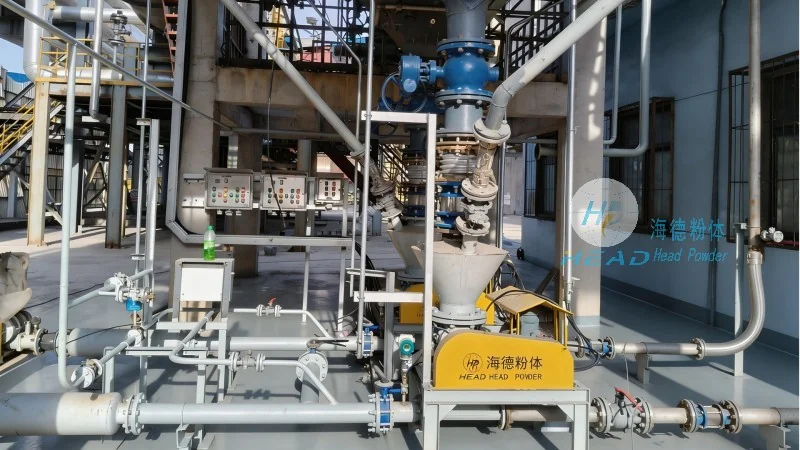
Design Principles of Automatic Powder Pneumatic Conveying Equipment
The design of an automatic powder pneumatic conveying system is governed by several critical principles that ensure efficient and reliable operation. One of the most important principles is the selection of the appropriate air velocity, which must be high enough to keep the powder particles suspended in the air stream but low enough to prevent excessive wear on the pipeline and components. The air velocity is typically determined based on the particle size, density, and flow rate of the powder being conveyed. Another key design principle is the use of appropriate pipeline materials and diameters. The pipeline must be able to withstand the pressure and temperature conditions of the conveying process, and its diameter should be optimized to minimize pressure drop and energy consumption. Additionally, the system design must consider the need for proper cleaning and maintenance, as powder can accumulate in the pipeline and affect performance over time. The use of features such as pulse-jet cleaning or automatic valve control helps to maintain the system's efficiency and longevity.
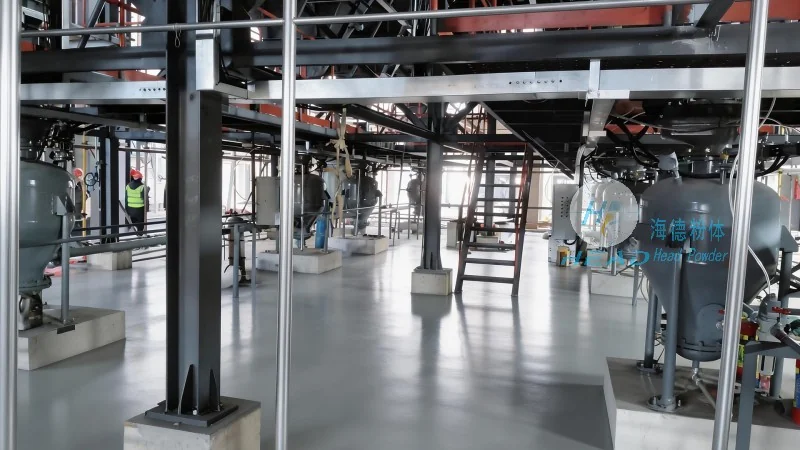
Key Features and Advantages of Automatic Powder Pneumatic Conveying Equipment
Automatic powder pneumatic conveying equipment offers several advantages over traditional mechanical conveying methods. One of the main benefits is its ability to handle a wide variety of powder types, including fine powders, cohesive powders, and powders with high moisture content. The system can also transport materials over long distances and through complex layouts, making it suitable for large-scale industrial applications. Another advantage is the reduced risk of contamination, as the enclosed pipeline system prevents exposure to external elements and reduces the risk of cross-contamination between different materials. Furthermore, the system is relatively easy to install and maintain, with many components being modular and replaceable. This makes it a cost-effective solution for industries that require frequent changes in production processes or material types.
Applications of Automatic Powder Pneumatic Conveying Equipment
The versatility of automatic powder pneumatic conveying equipment makes it suitable for a wide range of applications across various industries. In the pharmaceutical industry, it is used to transport active pharmaceutical ingredients (APIs) and excipients with high precision and minimal contamination. In the food processing industry, it is used to convey ingredients such as flour, sugar, and spices, ensuring consistent quality and safety. In the chemical manufacturing industry, it is used to transport raw materials and intermediates, improving process efficiency and reducing downtime. Additionally, the system is used in the mining and mineral processing industry to transport ore and other bulk materials from processing plants to storage facilities. The ability to handle different materials and process conditions makes it a valuable asset in many industrial settings.
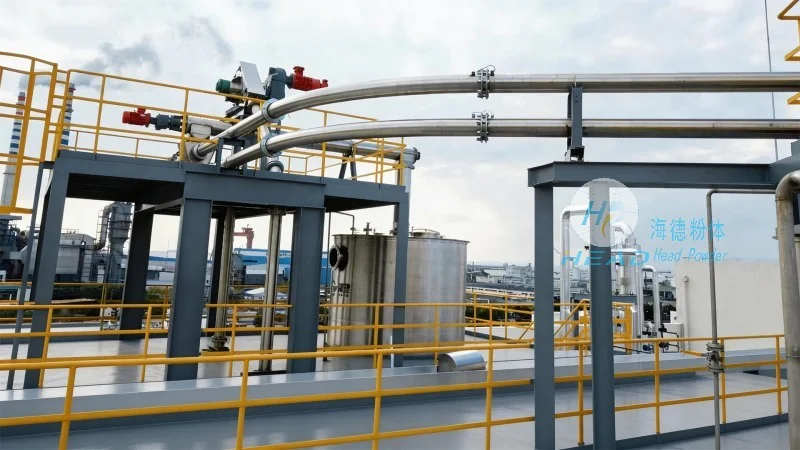
Conclusion and Company Information
Automatic powder pneumatic conveying equipment is a sophisticated and efficient solution for transporting bulk powder materials in industrial applications. Its design principles, which focus on air velocity, pipeline design, and system maintenance, ensure optimal performance and reliability. The equipment offers numerous advantages, including versatility, reduced contamination risk, and ease of maintenance, making it a preferred choice for many industries. As a leading manufacturer in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in providing high-quality automatic powder pneumatic conveying systems tailored to the specific needs of its clients. With a focus on innovation and customer satisfaction, HeadPowder has established itself as a trusted partner in the industry, delivering reliable and efficient solutions for powder handling challenges. The company's headquarters is located in Shandong, China, and it continues to serve clients worldwide with its expertise and commitment to quality.