Multi-hopper pneumatic conveying systems represent a sophisticated solution for the efficient and reliable transportation of bulk powders and granular materials across industrial facilities. These systems are integral to processes in sectors such as chemicals, food, pharmaceuticals, and cement, where precise material handling is critical to maintaining product quality and operational efficiency. The core technology behind these systems is the multi-hopper pump, which enables the sequential or simultaneous feeding of different powders, thereby enhancing process flexibility and control.
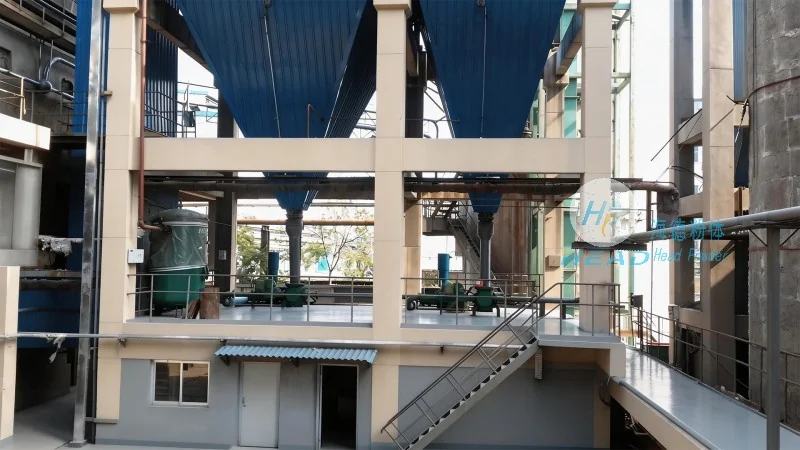
Working Principle of Multi-Hopper Powder Conveying Systems
The operation of a multi-hopper powder conveying system is grounded in pneumatic conveying principles, where compressed air or gas acts as the medium to transport material through a pipeline network. The system typically comprises multiple hoppers, each holding a distinct powder or material, connected to a central conveying line. When activated, compressed air is introduced into the hoppers, creating a pressure differential that forces the material into the pipeline. The material is then carried by the air stream to the target destination, such as a storage silo, processing unit, or packaging station. The multi-hopper design allows for simultaneous or sequential discharge of different powders, facilitating complex material blending and processing without the need for separate conveying lines for each material.
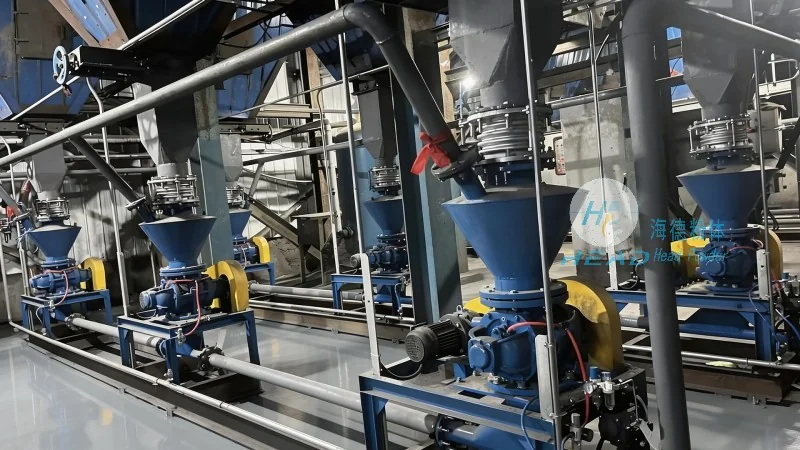
Key Features of Multi-Hopper Powder Conveying Systems
Multi-hopper powder conveying systems offer several distinct advantages that make them suitable for modern industrial applications. Firstly, they provide high flexibility in material handling, enabling precise control over the composition of blended products. This is particularly valuable in industries where product customization is required. Secondly, these systems are energy-efficient and cost-effective, as they reduce reliance on mechanical components like conveyors or elevators, which can be prone to wear and maintenance issues. Thirdly, the isolated hopper design minimizes material degradation and contamination, ensuring consistent product quality and compliance with industry standards. Additionally, the compact and modular design allows for easy integration into existing production lines, with minimal disruption to operations. The systems are also designed for durability, with robust construction to withstand the demands of continuous use.
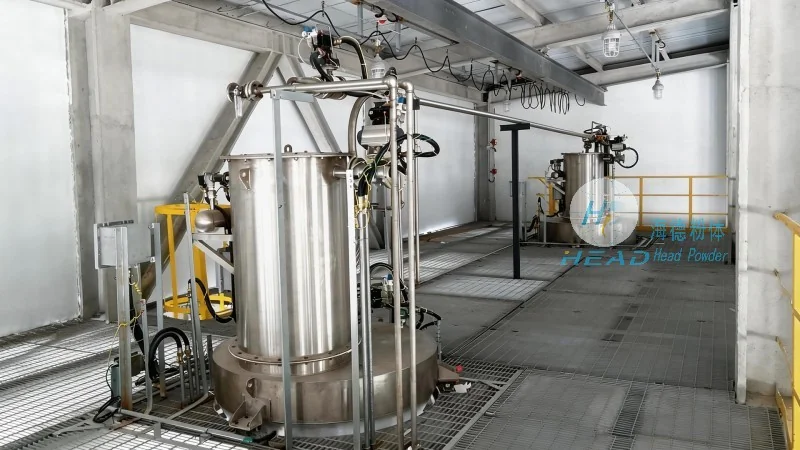
Applications and Benefits in Industrial Settings
Multi-hopper powder conveying systems are widely adopted in industries where material handling efficiency and product safety are paramount. For instance, in the chemical industry, they are used to transport reactive powders and granules, ensuring safe and controlled handling. In the food and pharmaceutical sectors, the enclosed design and isolated hoppers prevent cross-contamination, maintaining hygiene standards. The ability to blend powders in real-time enhances product versatility, allowing manufacturers to meet diverse market demands. Furthermore, these systems improve workplace safety by reducing manual handling of bulk materials, minimizing accident risks. The reliability of the multi-hopper design also leads to reduced downtime, as the system can be easily maintained without interrupting production.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly referred to as HeadPowder, is a leading provider of advanced powder handling equipment. HeadPowder specializes in designing and manufacturing multi-hopper pneumatic conveying systems tailored to the unique needs of various industries. The company is headquartered in Shandong, China, and has built a strong reputation for delivering reliable, efficient, and cost-effective solutions. HeadPowder's commitment to innovation ensures its products incorporate the latest technological advancements, meeting industry standards for performance and durability. The company’s team of experienced engineers and technicians collaborates closely with clients to develop customized solutions that enhance operational efficiency and product quality. HeadPowder's multi-hopper systems are constructed with high-quality materials and advanced manufacturing techniques, ensuring long-term performance and minimal maintenance. The company’s customer-centric approach and comprehensive after-sales support further solidify its position in the competitive industrial equipment market.




