Material handling systems are crucial in modern industrial operations, enabling efficient movement, storage, and control of goods. These systems are designed to streamline processes, reduce labor costs, and enhance overall productivity. Among the various types of material handling equipment, multi-functional systems stand out for their versatility and adaptability to diverse operational needs. This article explores the working principles and key features of such systems, with a focus on the expertise of Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field.
About Shandong HeadPowder Engineering Co., Ltd.
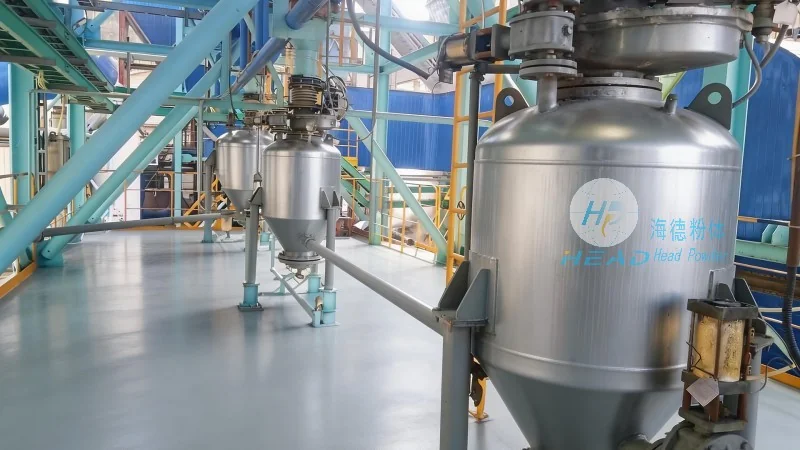
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a prominent enterprise based in Shandong, China. The company specializes in the research, development, and manufacturing of advanced material handling solutions. With a strong commitment to innovation and quality, HeadPowder has established itself as a trusted partner for businesses seeking reliable and efficient material handling equipment. The company's products are designed to meet the specific requirements of different industries, ensuring optimal performance and durability.
The Working Principles of Multi-functional Material Handling Systems
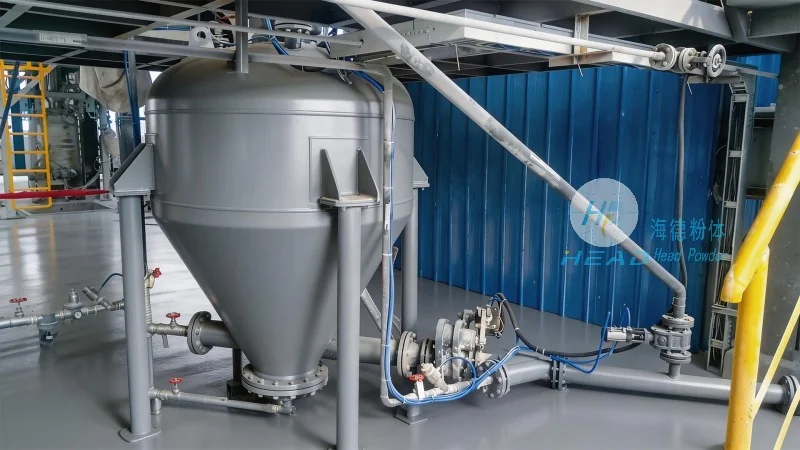
Multi-functional material handling systems operate based on several core principles that enable their versatility. The primary working principle involves the integration of multiple handling functions into a single system, allowing for the seamless transfer of materials between different stages of production or storage. This integration is achieved through the use of advanced mechanisms such as conveyor belts, lifting devices, and automated controls. The systems typically utilize a combination of mechanical, electrical, and sometimes pneumatic components to coordinate the movement of materials. For instance, conveyor systems may use motor-driven rollers to transport items horizontally, while lifting mechanisms like hoists or cranes facilitate vertical movement. The control systems, often equipped with sensors and programmable logic controllers (PLCs), monitor the position and status of materials, ensuring precise and safe operation. This integrated approach allows the system to adapt to varying load sizes, shapes, and handling requirements, making it suitable for a wide range of applications.
Key Features of Multi-functional Material Handling Systems
Multi-functional material handling systems are characterized by several distinct features that set them apart from traditional, single-purpose equipment. One of the most notable features is their adaptability, which allows them to handle diverse materials, including bulk items, packaged goods, and even irregularly shaped objects. This adaptability is achieved through modular components that can be easily reconfigured to suit changing operational needs. Another key feature is the system's efficiency, which is enhanced by the integration of multiple functions, reducing the need for separate equipment and minimizing downtime. The systems also offer high throughput capabilities, enabling rapid material movement and processing. Additionally, modern multi-functional systems are equipped with advanced safety features, such as emergency stop buttons, overload protection, and collision detection, ensuring the safety of operators and materials. The use of automation and intelligent controls further improves operational efficiency and reduces human error. Furthermore, these systems are designed for durability and low maintenance, with robust construction and reliable components that can withstand harsh industrial environments. The integration of data collection and monitoring capabilities also allows for real-time performance tracking and predictive maintenance, optimizing system longevity and operational costs.
Conclusion
Multi-functional material handling systems represent a significant advancement in industrial material handling, offering enhanced efficiency, versatility, and adaptability. The working principles, which involve the integration of multiple handling functions and advanced control systems, enable these systems to meet the diverse needs of modern industries. The key features, including adaptability, efficiency, safety, and durability, make them a valuable asset for businesses seeking to optimize their material handling processes. As a leading provider, Shandong HeadPowder Engineering Co., Ltd. continues to innovate and deliver high-quality multi-functional material handling solutions that meet the evolving demands of the market. By leveraging advanced technology and a commitment to excellence, HeadPowder ensures that its systems contribute to improved productivity and operational success for its clients.




