Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and supply of advanced bulk powder pneumatic conveying equipment, including systems tailored for loading and unloading trucks. With a focus on efficiency and reliability, the company's solutions are engineered to meet the demanding requirements of various industrial sectors.
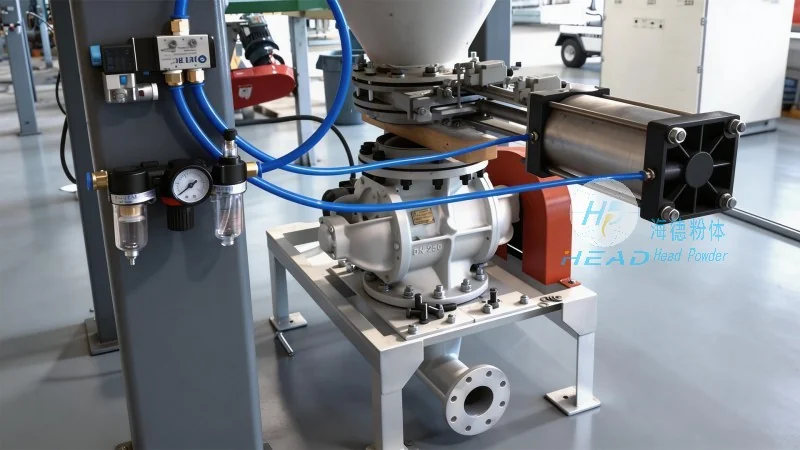
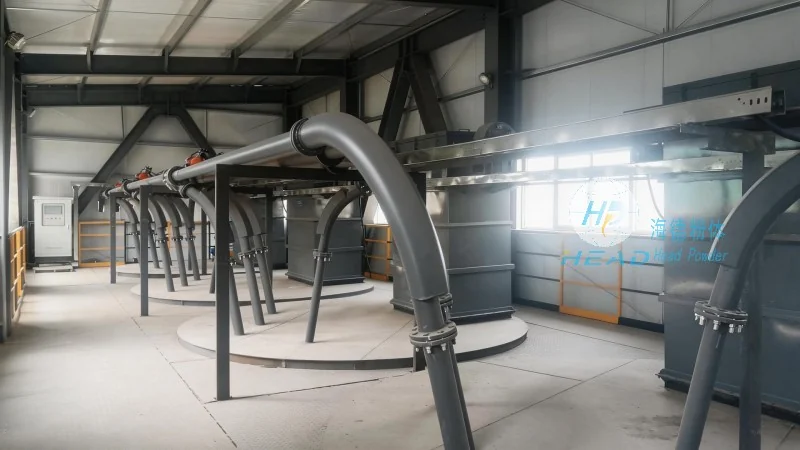
Bulk Powder Pneumatic Conveying Equipment for Truck Loading and Unloading
HeadPowder's bulk powder pneumatic conveying equipment is specifically designed to facilitate the efficient transfer of dry bulk materials between trucks and processing facilities. This equipment utilizes pneumatic technology to transport powders such as cement, flour, chemicals, and other fine or coarse materials with minimal loss and maximum control. The system operates by creating a pressure differential that draws the material from the truck into the conveying line, ensuring a smooth and continuous flow. Key components include a hopper, rotary valve, and a series of pipes or ducts that guide the material to its destination.
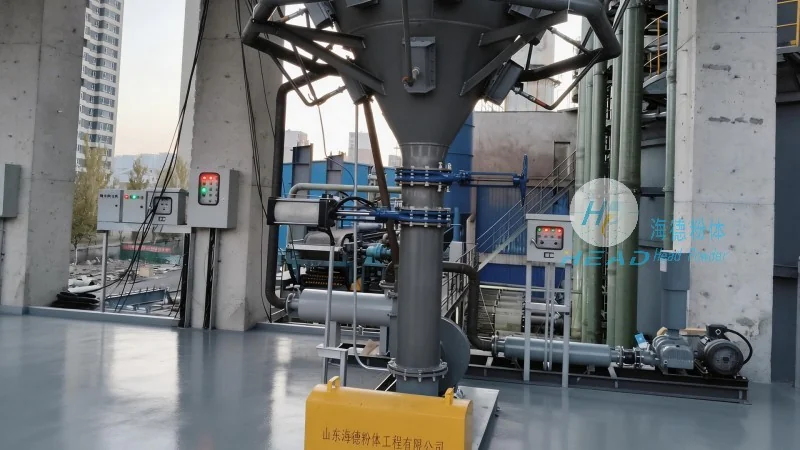
Working Principle of the Pneumatic Conveying System
The core mechanism of the bulk powder pneumatic conveying equipment involves the use of compressed air to move material through a closed system. The process begins with the material being fed into a hopper, where it is then discharged into a rotary airlock valve. This valve controls the flow of material into the conveying line, preventing backflow and ensuring a consistent feed rate. Compressed air is introduced into the system, creating a pressure that propels the material forward. The air and material mixture travels through the pipes, with the air acting as the carrier medium. At the receiving end, the material is separated from the air, typically through a cyclone separator or filter, and collected in a storage bin or processing unit. The air is then filtered and recycled back into the system, minimizing waste and energy consumption.
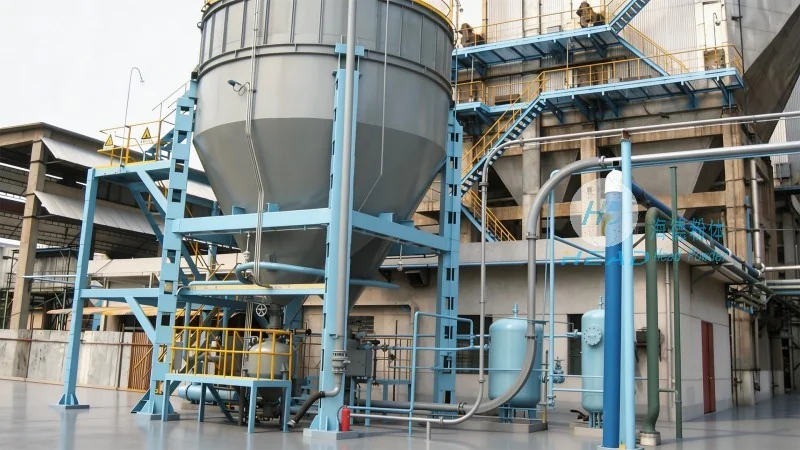
Key Features and Advantages
HeadPowder's truck loading and unloading pneumatic conveying systems offer several distinct advantages that make them ideal for industrial applications. First, the equipment provides a dust-free and hygienic transfer process, which is crucial for materials that require strict contamination control, such as food products or pharmaceuticals. The enclosed system prevents material spillage and reduces the risk of dust exposure, enhancing workplace safety and compliance with environmental regulations. Second, the system offers high efficiency and reliability, with minimal downtime due to its robust design and automated controls. The use of compressed air allows for precise control over the flow rate and pressure, ensuring consistent material transfer even with varying load conditions. Third, the equipment is versatile and can handle a wide range of materials, from fine powders to coarse granules, with adjustable settings to accommodate different material properties. Additionally, the system is compact and can be customized to fit specific site requirements, making it suitable for both new installations and retrofit applications. The energy efficiency of the system, through air recycling and optimized pressure management, contributes to lower operational costs over time.




