Bin pump material pneumatic conveying lines are essential equipment in modern industrial processes, particularly for the efficient and reliable transport of bulk materials over long distances or across different levels. This article provides an in-depth look at the working principle and key features of such systems, presented by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China.
Company Introduction
Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and installation of advanced material handling solutions. With a strong focus on innovation and customer satisfaction, the company has established itself as a trusted partner in the industry. HeadPowder's expertise lies in developing customized pneumatic conveying systems tailored to meet the specific needs of various sectors, including food, chemical, pharmaceutical, and mining industries.
Working Principle of Bin Pump Material Pneumatic Conveying Lines
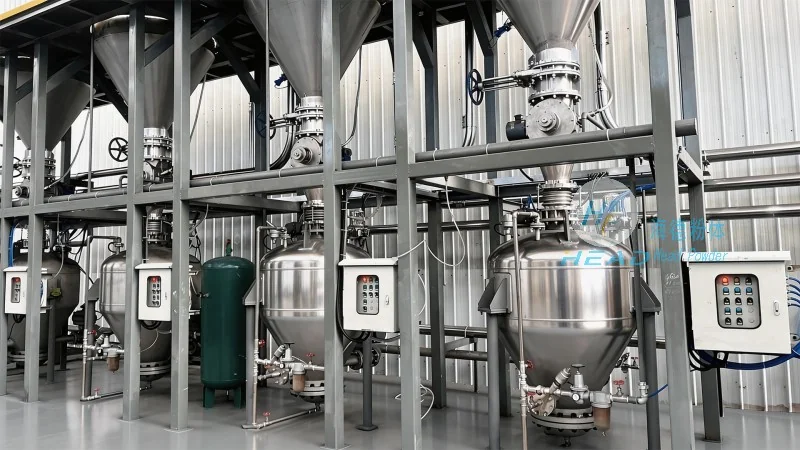
The core of a bin pump material pneumatic conveying line is the bin pump, which acts as the central component for material transport. The system operates on the principle of creating a pressure differential between the hopper and the discharge point. Initially, the bin pump is filled with the material to be conveyed. Then, air is introduced into the pump chamber, creating a high-pressure environment that forces the material to move through the pipeline. The bin pump's design typically includes a diaphragm or piston mechanism that alternately compresses and releases the air, ensuring a consistent and controlled flow of material. This mechanism allows for the efficient transport of bulk materials without the need for mechanical parts that come into direct contact with the material, reducing wear and maintenance requirements.
Key Features of Bin Pump Material Pneumatic Conveying Lines
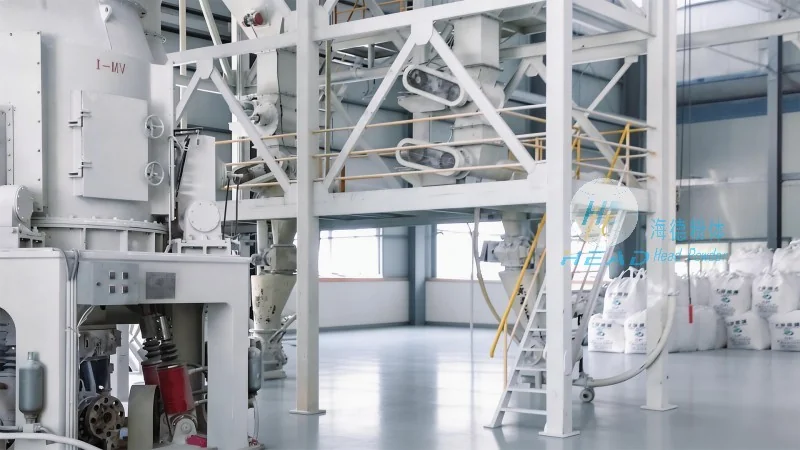
Bin pump material pneumatic conveying lines offer several advantages that make them ideal for industrial applications. One of the primary features is their ability to handle a wide range of materials, from fine powders to coarse granules, without the risk of clogging or degradation. The system's flexibility allows for horizontal, vertical, or inclined transport, making it suitable for complex layouts and challenging environments. Another significant feature is the low maintenance requirement. Unlike traditional screw or belt conveyors, bin pumps have fewer moving parts and are less prone to wear, resulting in lower operational costs and longer service life. Additionally, the system provides excellent material containment, minimizing dust emissions and ensuring compliance with environmental regulations. The ability to operate under negative pressure or positive pressure modes further enhances its versatility, allowing for both suction and pressure conveying applications.
Applications and Benefits
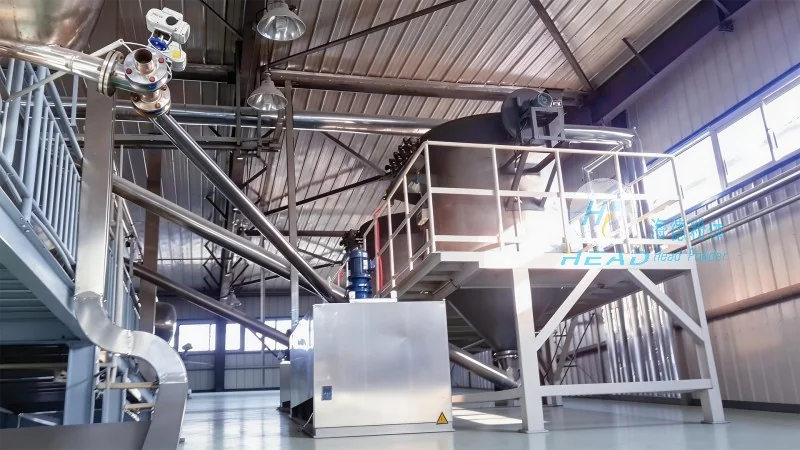
Bin pump material pneumatic conveying lines are widely used in various industries due to their adaptability and efficiency. In the food industry, they are used for transporting powders such as flour, sugar, and spices, ensuring hygienic and dust-free handling. In the chemical industry, they handle chemicals and additives, providing safe and controlled transport. The mining sector utilizes these systems for transporting ore and minerals, enabling efficient material movement in large-scale operations. The benefits of using bin pump systems include improved process reliability, reduced downtime, and enhanced safety. The consistent flow of material also helps in maintaining process stability, which is crucial for quality control in manufacturing processes.
Conclusion
Bin pump material pneumatic conveying lines represent a sophisticated solution for bulk material handling, combining advanced technology with practical design. By understanding the working principle and key features, industries can make informed decisions about implementing these systems to enhance operational efficiency and productivity. Shandong HeadPowder Engineering Co., Ltd. continues to lead in the development of such systems, providing customized solutions that meet the evolving needs of modern industrial applications.




