For industries that require precise material handling while maintaining a clean environment, dust-free closed material pneumatic conveying systems offer an efficient solution. These systems are designed to transport bulk materials from one location to another without exposing them to the air, thus preventing contamination and dust dispersion. In this article, we will explore the working principle and key features of such systems, highlighting how they contribute to operational efficiency and product integrity.
Working Principle of Dust-Free Closed Material Pneumatic Conveying Systems
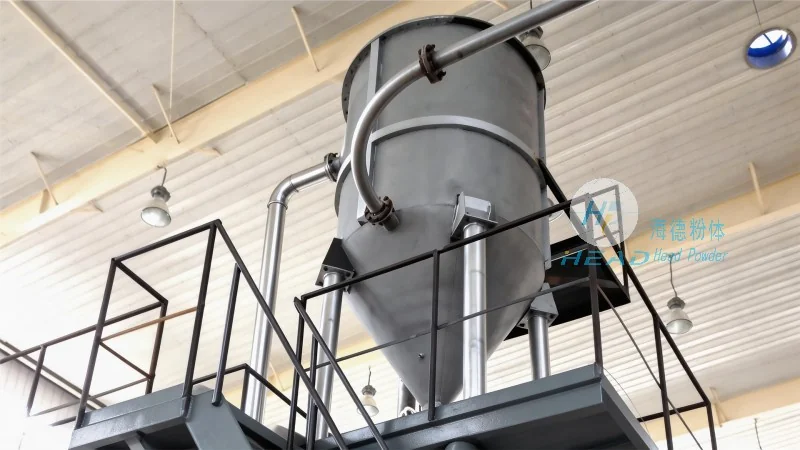
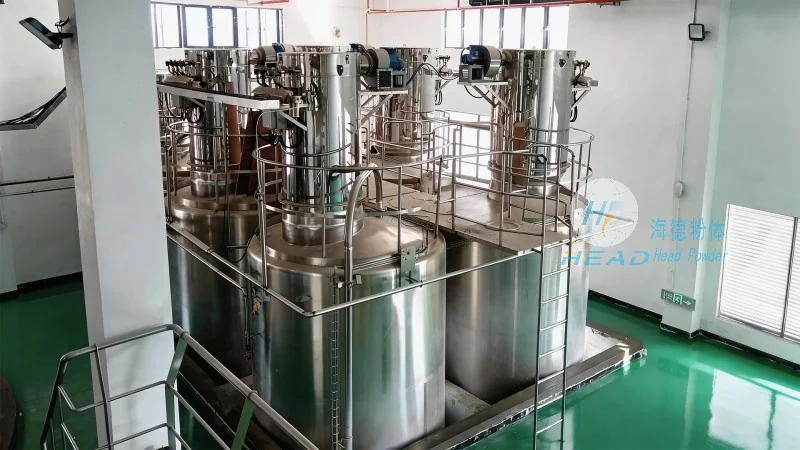
The core of a dust-free closed material pneumatic conveying system lies in its ability to transport materials through a sealed pipeline using air pressure. The process typically involves several key components: a material hopper, a feeder, a conveying line, and a receiver. The material is first loaded into the hopper, where it is then fed into the conveying line via a feeder. The feeder controls the flow rate of the material, ensuring a consistent and controlled transport. Compressed air is introduced into the conveying line, creating a pressure differential that propels the material through the system. The air and material mixture travels through the pipeline, and the material is separated from the air at the receiver, where the air is often filtered and recycled. This closed-loop system minimizes the risk of dust emissions and ensures that the material remains in a controlled environment throughout the conveying process.
Key Features of Dust-Free Closed Material Pneumatic Conveying Systems
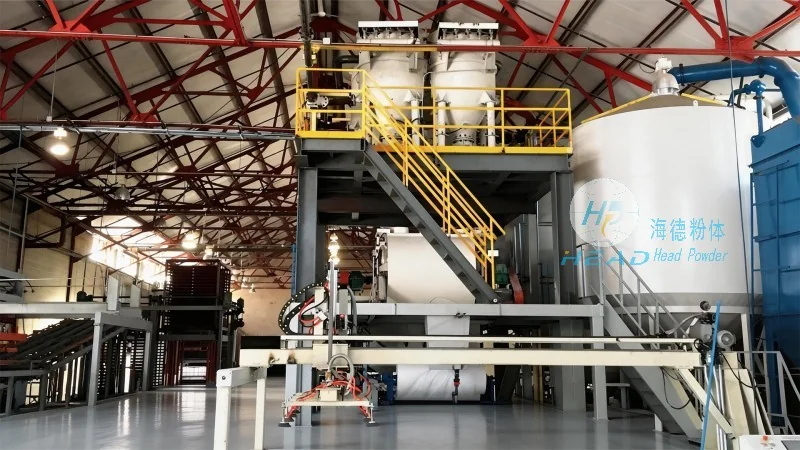
Several notable features distinguish dust-free closed material pneumatic conveying systems from traditional open systems. Firstly, the closed design prevents dust and particles from escaping into the environment, making them ideal for applications in pharmaceutical, food, and chemical industries where product purity is paramount. Secondly, these systems offer high transport efficiency, with the ability to move materials over long distances with minimal energy consumption. The sealed pipeline also reduces the risk of material degradation due to exposure to air or moisture. Additionally, the systems are easy to clean and maintain, as the entire pipeline can be flushed and sanitized to prevent cross-contamination. Another advantage is the flexibility in material handling, as they can transport a wide range of bulk materials, including powders, granules, and pellets. The control systems are often integrated with sensors that monitor pressure, flow, and material level, providing real-time data for process optimization.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of advanced material handling solutions. With a focus on innovation and quality, the company specializes in designing and manufacturing dust-free closed material pneumatic conveying systems tailored to the needs of various industries. HeadPowder's products are engineered to meet stringent industry standards, ensuring reliability, durability, and efficiency. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with the latest technology and skilled personnel. HeadPowder's commitment to customer satisfaction and technological advancement has made it a trusted partner for businesses seeking reliable material handling solutions.




