HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced material handling systems. The bulk bag unloading station material pneumatic conveying line is a critical component in many industrial processes, enabling efficient and safe transfer of bulk materials from large bags to processing equipment. This system combines the functionality of bulk bag unloading with pneumatic conveying technology to streamline material handling operations.
Working Principle of the Pneumatic Conveying Line
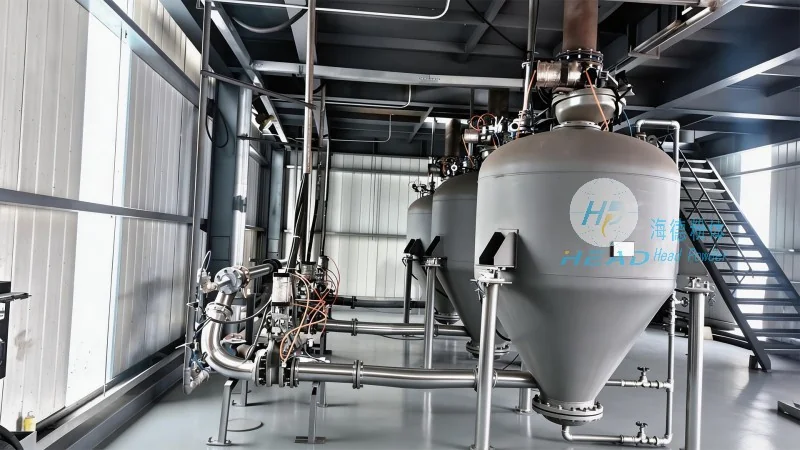
The operation of a bulk bag unloading station material pneumatic conveying line involves several key steps. First, the bulk bag is positioned over the unloading hopper, which is equipped with a discharge valve. The bag is then opened, and the material is released into the hopper. Simultaneously, a vacuum or pressure system is activated to draw the material from the hopper into the conveying pipeline. The conveying line transports the material to the desired destination, such as a storage silo or processing unit. The system uses air as the conveying medium, which is controlled by a blower or vacuum pump to ensure consistent material flow. The entire process is automated, reducing manual labor and minimizing the risk of material spillage or contamination.
Key Features and Advantages
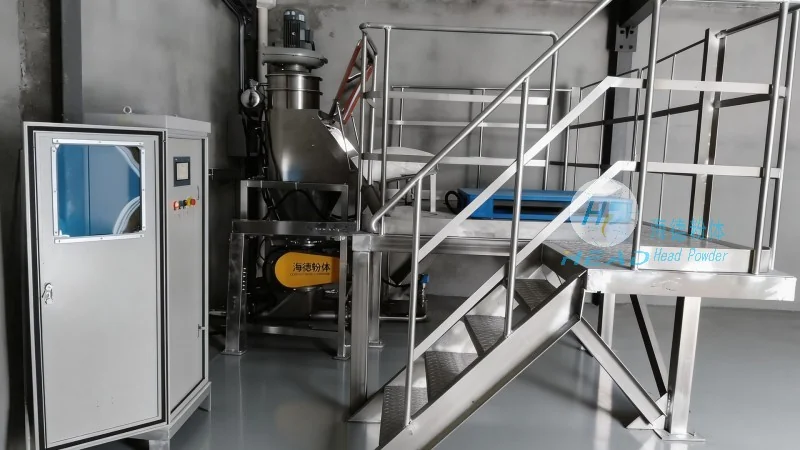
HeadPowder's bulk bag unloading station material pneumatic conveying line offers several notable features that enhance operational efficiency and reliability. One of the primary advantages is its ability to handle a wide range of bulk materials, including powders, granules, and fine particles, with minimal degradation. The system is designed for high throughput, allowing for rapid material transfer even with large bag capacities. Additionally, the pneumatic conveying method ensures a dust-free environment, which is crucial for maintaining product quality and worker safety. The equipment is also equipped with advanced control systems that monitor pressure, flow rate, and material level, providing real-time feedback and preventing system failures. Another key feature is the modular design, which allows for easy integration with existing production lines and scalability to accommodate future expansion. The robust construction of the components ensures long-term durability and low maintenance costs, making it a cost-effective solution for industrial material handling needs.
Application Scenarios
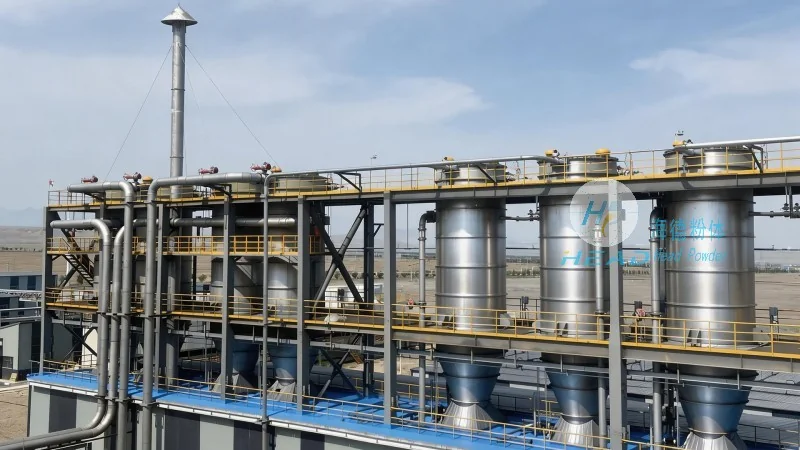
This material handling system is widely used in various industries, including chemical, pharmaceutical, food, and mining. In the chemical industry, it is used to transfer raw materials like powders and granules to reactors and storage tanks. In the pharmaceutical sector, the system ensures sterile and contamination-free material transfer, meeting stringent regulatory requirements. The food industry benefits from the dust-free operation and hygienic design, which are essential for maintaining food safety standards. In the mining industry, the line is used to transport ore and other bulk materials from storage to processing facilities. The versatility of the system makes it suitable for a wide range of applications, providing a reliable solution for material handling challenges in different sectors.




