For companies in the cement industry, efficient material handling is crucial to maintaining production efficiency and reducing operational costs. Pneumatic conveying systems offer a reliable solution for transporting bulk materials such as cement, fly ash, and mineral powders. These systems utilize air pressure to move materials through a network of pipes, providing a dust-free and automated method of material transport. In this article, we will explore the working principles and key features of pneumatic conveying lines specifically designed for cement, fly ash, and mineral powders, highlighting how they enhance operational performance and contribute to sustainable industrial practices.
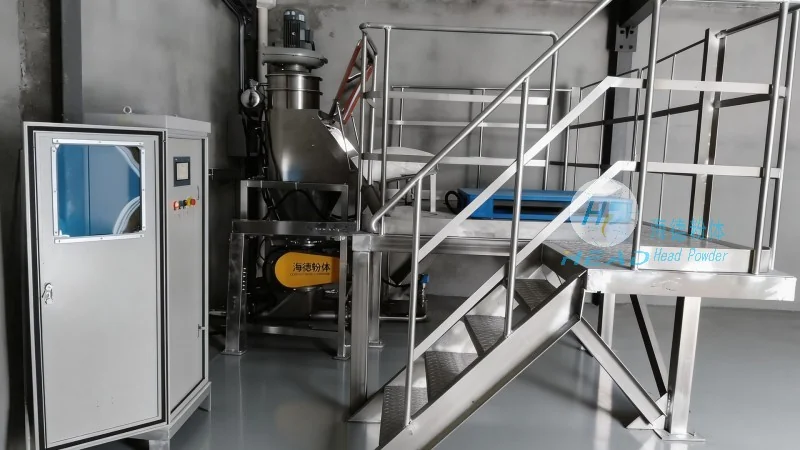
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of advanced material handling solutions. With a strong focus on innovation and customer satisfaction, HeadPowder specializes in designing and manufacturing high-quality pneumatic conveying systems tailored to the needs of the cement industry. The company’s headquarters is located in Shandong, China, where it leverages local expertise and resources to develop cutting-edge technologies that meet international standards. HeadPowder’s commitment to quality and reliability has made it a trusted partner for numerous cement manufacturers worldwide.
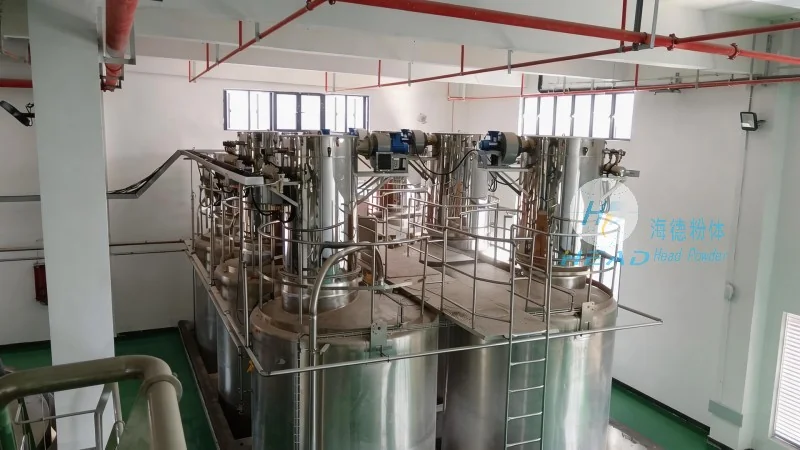
The Working Principle of Pneumatic Conveying Lines
The core of a pneumatic conveying system is its ability to transport bulk materials using air pressure. The system typically consists of a hopper, a blower or compressor, a pipeline network, and a discharge point. When material is added to the hopper, the blower creates a vacuum or positive pressure that draws the material into the pipeline. The material is then carried through the pipes by the moving air, which can be either in a dilute-phase or dense-phase mode, depending on the system design and material characteristics. The dilute-phase system is suitable for light materials like fly ash, while the dense-phase system is used for heavier materials such as cement, ensuring efficient and controlled transport. The system also includes control valves and filters to regulate the flow and prevent material buildup or contamination. This mechanism allows for a continuous, automated process that minimizes manual labor and reduces the risk of dust exposure.
Key Features of Cement, Fly Ash, and Mineral Powder Pneumatic Conveying Lines
HeadPowder’s pneumatic conveying lines for cement, fly ash, and mineral powders are designed with several key features that enhance performance and reliability. One of the primary features is the ability to handle a wide range of material types and particle sizes, from fine powders to coarse granules. The systems are equipped with adjustable air pressure and flow rates, allowing operators to optimize the transport process for different materials. Another important feature is the dust-free operation, which is achieved through sealed pipelines and efficient filtration systems. This not only improves workplace safety but also reduces the need for additional dust control measures. The systems also incorporate advanced control technology, including sensors and automation, which enable real-time monitoring and adjustment of the conveying process. This ensures consistent material flow and prevents system downtime due to blockages or other issues. Additionally, the modular design of the systems allows for easy installation and maintenance, reducing the overall lifecycle costs for the end-user.
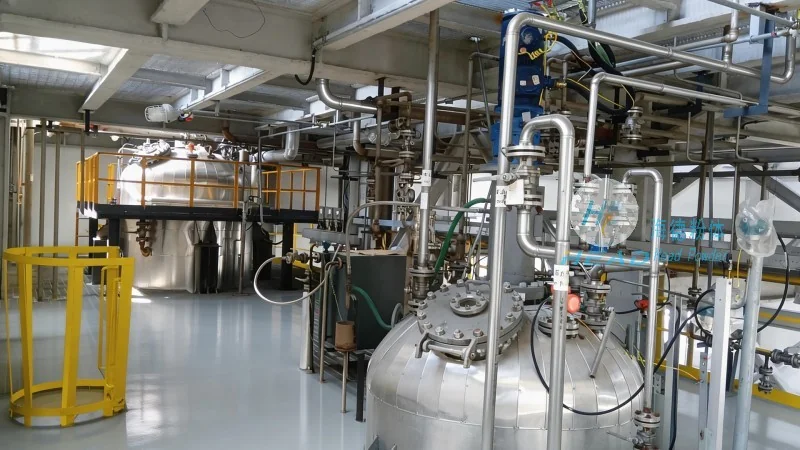
Benefits and Applications
The use of pneumatic conveying lines for cement, fly ash, and mineral powders offers numerous benefits for cement manufacturers. These systems improve production efficiency by enabling continuous material transport, reducing downtime and increasing throughput. The dust-free operation enhances workplace safety and compliance with environmental regulations. The modular design and ease of maintenance also contribute to lower operational costs over the long term. HeadPowder’s systems are widely used in various applications, including raw material transport from storage silos to production lines, and finished product delivery to storage or packaging areas. The company’s expertise in customizing systems to meet specific customer requirements ensures that each installation is optimized for the unique needs of the client, whether it’s a new plant or an upgrade to an existing facility.




