Positive pressure dilute phase pneumatic conveying systems are advanced industrial solutions designed to transport bulk materials efficiently over long distances with minimal operational complexity. These systems are widely used in various industries, including food processing, pharmaceuticals, chemicals, and mining, due to their ability to handle a wide range of materials while maintaining product integrity and operational flexibility.
Working Principle of Positive Pressure Dilute Phase Pneumatic Conveying Systems
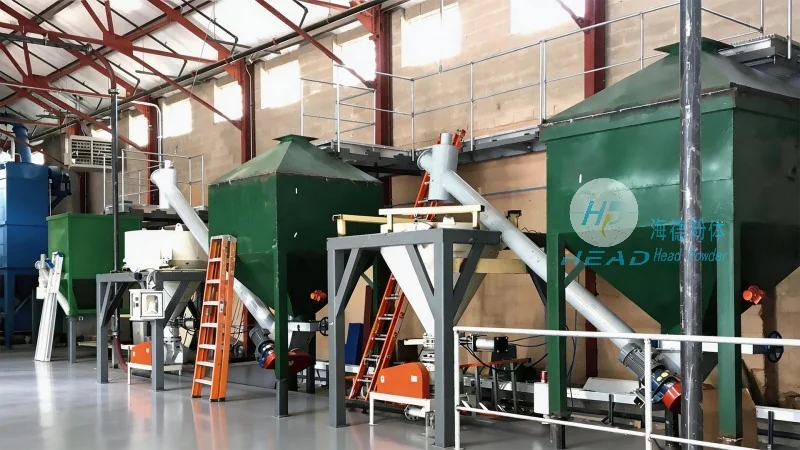
The working principle of a positive pressure dilute phase pneumatic conveying system involves several key steps. First, bulk material is fed into a hopper from which it is drawn into a feeder. The feeder then controls the flow rate of the material, ensuring a consistent supply to the system. Simultaneously, a blower or compressor generates compressed air, which is introduced into the pipeline at a controlled pressure. The compressed air creates a positive pressure environment that lifts and suspends the material particles in the air stream. As the material is suspended, it is transported through the pipeline to the discharge point. The system maintains a continuous flow of air and material, preventing material buildup and ensuring smooth operation. The pressure differential between the inlet and outlet of the system is carefully managed to achieve the desired flow rate and material transport efficiency. This coordinated operation of the blower, feeder, and pipeline network is essential for the effective functioning of the positive pressure dilute phase pneumatic conveying system.
Key Features of Positive Pressure Dilute Phase Pneumatic Conveyors
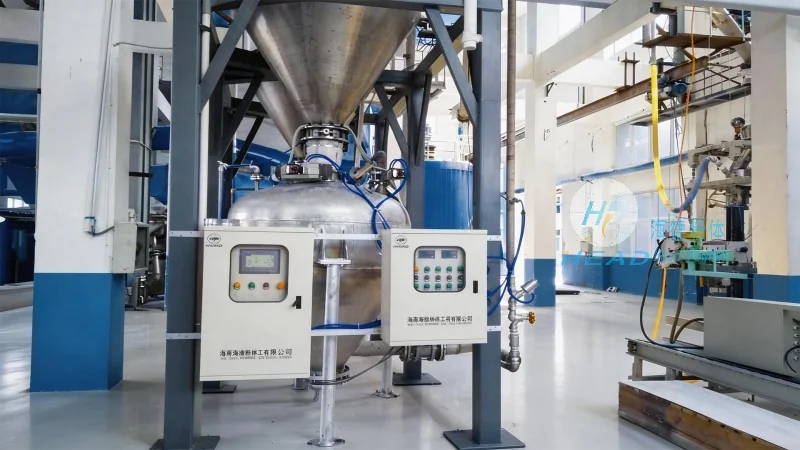
Key features of positive pressure dilute phase pneumatic conveyors include their ability to handle a wide range of materials, from fine powders to coarse granules, without the need for mechanical components that could cause contamination or damage. The closed-loop design of the system helps to prevent dust emissions and maintain a clean working environment, which is critical in industries such as food processing and pharmaceuticals. Flexibility is another significant feature, as the system can be easily modified to accommodate changes in material flow rates or pipeline configurations. The use of positive pressure ensures that air and material are continuously moving, reducing the risk of material buildup or clogging in the pipeline. Energy efficiency is also a key advantage, as the compressed air is used effectively to transport material over long distances with minimal energy loss. The system provides excellent control over material flow, enabling precise dosing and delivery to downstream processes. Additionally, these conveyors are highly reliable, with minimal maintenance requirements, making them a cost-effective solution for long-term material handling needs.
Applications and Benefits in Industrial Settings
Positive pressure dilute phase pneumatic conveying systems are widely used in various industrial applications due to their ability to handle diverse materials and operate in clean environments. In the food and pharmaceutical industries, these systems are essential for transporting ingredients and finished products without the risk of contamination. For example, in food processing, they are used to move flour, sugar, and other powders from storage to production lines, ensuring a hygienic and efficient process. In the pharmaceutical sector, they are critical for handling active pharmaceutical ingredients (APIs) and other sensitive materials, as the closed system prevents cross-contamination and maintains product purity. The chemical industry benefits from these systems when handling hazardous materials, as the enclosed design protects workers and the environment from exposure. In the mining and minerals sector, positive pressure dilute phase pneumatic conveyors are used to transport raw materials such as coal, ore, and minerals over long distances, improving operational efficiency and reducing transportation costs. The mining industry, in particular, relies on these systems to handle large volumes of material with minimal manual intervention, enhancing safety and productivity. The benefits of using these systems extend to improved workplace safety by reducing manual handling and exposure to dust, and enhanced operational efficiency by automating the material handling process. Overall, positive pressure dilute phase pneumatic conveyors offer a reliable and efficient solution for bulk material transport in a variety of industrial settings.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
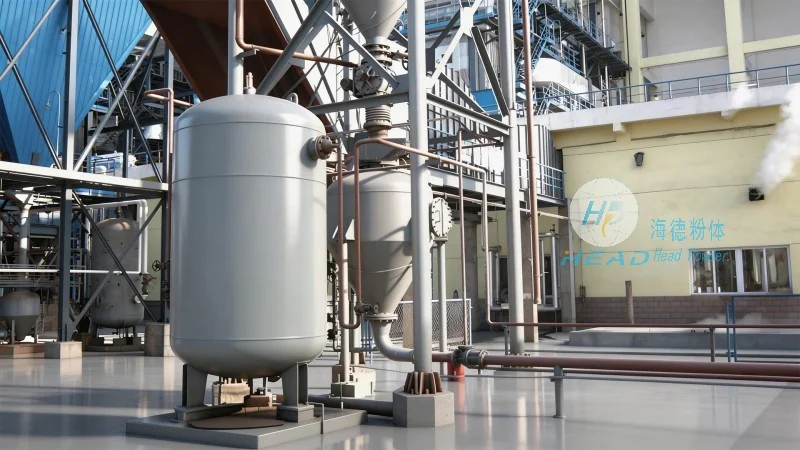
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of high-quality pneumatic conveying equipment. With a strong focus on innovation and customer satisfaction, HeadPowder has established itself as a trusted partner in the industry, providing tailored solutions to meet the diverse needs of its clients. The company’s products, including positive pressure dilute phase pneumatic conveyors, are designed to meet international standards and are backed by rigorous quality control processes. HeadPowder’s team of experienced engineers and technicians work closely with clients to understand their specific requirements and develop customized solutions that optimize material handling processes. The company’s commitment to excellence and reliability has made it a preferred choice for businesses seeking efficient and reliable pneumatic conveying systems. HeadPowder’s facilities are located in Shandong, China, where the company leverages advanced manufacturing technologies and skilled workforce to produce high-performance equipment. The company’s product range includes various types of pneumatic conveyors, such as positive pressure dilute phase systems, and is continuously expanding to meet evolving industry demands. HeadPowder’s dedication to research and development ensures that its products remain at the forefront of technological advancements, providing clients with cutting-edge solutions for their material handling challenges.




