Efficient and reliable conveying of cereal powders is a critical aspect of modern food processing operations. The equipment designed for this purpose plays a pivotal role in ensuring smooth production workflows, maintaining product quality, and enhancing overall operational efficiency. This article delves into the fundamental principles behind cereal powder conveying systems, as well as the distinct characteristics of their working environments, providing insights into how these technologies are applied in real-world scenarios.
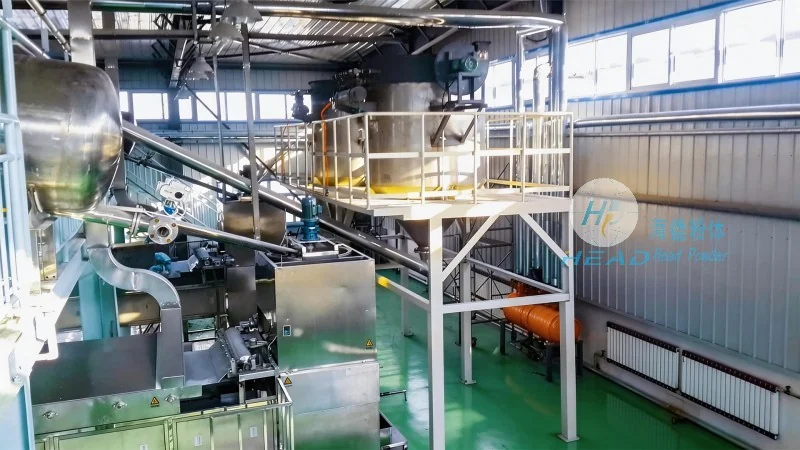
Introduction to Cereal Powder Conveying Equipment
At the core of many food processing facilities, cereal powder conveying equipment serves as a vital link between raw material handling and subsequent processing stages. These systems are engineered to transport dry, granular, or powdered cereal products with precision, ensuring minimal product degradation and consistent flow rates. The design and functionality of such equipment are tailored to meet the specific demands of cereal processing, including the need for gentle handling, low maintenance, and compatibility with various production scales.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field of powder handling technology, specializes in developing advanced conveying solutions for the food industry. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for businesses seeking reliable equipment for cereal powder processing. HeadPowder's headquarters is located in Shandong, China, where the company leverages local expertise and resources to deliver cutting-edge solutions that meet international standards.
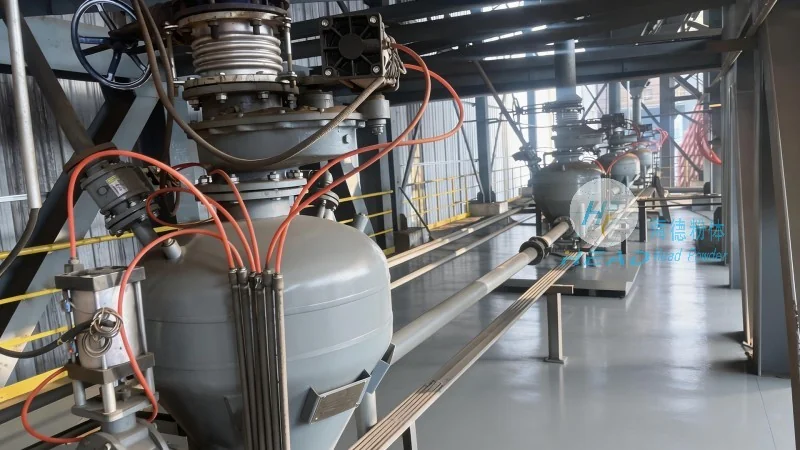
Principles of Cereal Powder Conveying
The operation of cereal powder conveying equipment is based on several key principles that ensure effective material transport. One of the primary mechanisms involves the use of air or mechanical forces to move the powder through a system of pipes or ducts. For instance, pneumatic conveying systems utilize compressed air to create a flow that carries the powder particles, while mechanical systems employ rotating components like screws or belts to propel the material. These principles are designed to maintain the integrity of the cereal powder, preventing issues such as clumping, segregation, or contamination during transport.
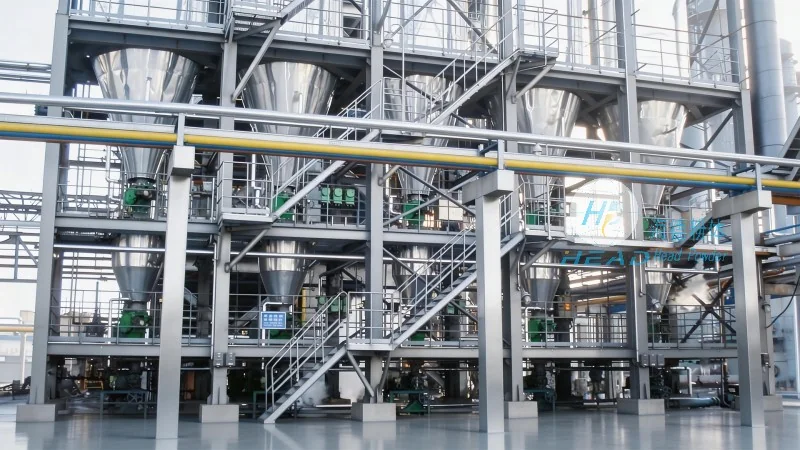
Working Scene Characteristics
The working environment of cereal powder conveying equipment varies significantly depending on the specific application and production scale. In large-scale industrial settings, such as cereal manufacturing plants or grain processing facilities, these systems are often integrated into complex production lines, requiring high throughput and consistent performance. The working scene characteristics include factors like the volume of material to be conveyed, the distance between processing stages, and the need for hygienic design to comply with food safety regulations. Additionally, the equipment must be adaptable to different types of cereal powders, including wheat, corn, oats, and other grains, each with unique physical properties that affect conveying efficiency.
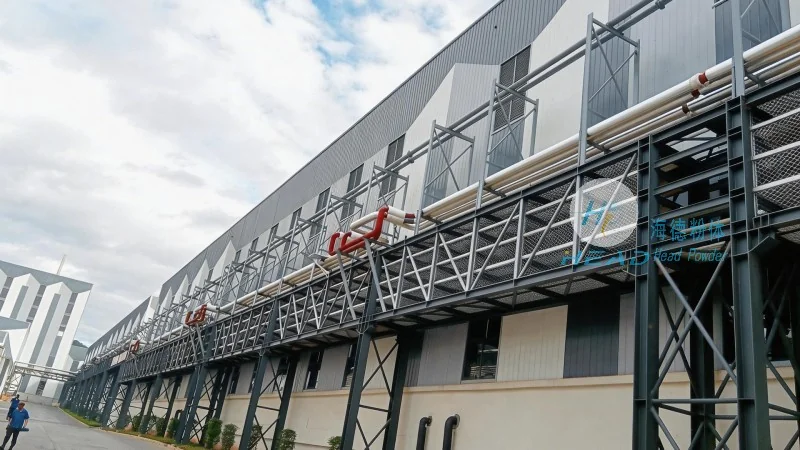
Application Scenarios and Operational Benefits
Cereal powder conveying equipment is widely used in various stages of the food processing industry. From raw material intake to packaging, these systems facilitate seamless material flow, reducing downtime and labor costs. In the context of cereal production, the equipment is essential for transporting raw grains into milling or grinding operations, as well as for moving finished powders to storage or packaging areas. The operational benefits of using specialized conveying systems include improved product quality through gentle handling, reduced waste due to minimal segregation, and enhanced safety by minimizing manual handling of powders. Furthermore, the systems are designed for easy integration with other processing equipment, allowing for streamlined production workflows and increased overall efficiency.
Conclusion
In summary, cereal powder conveying equipment is a critical component of modern food processing operations, enabling efficient and reliable transport of cereal products. The principles underlying these systems, combined with their adaptability to diverse working environments, make them indispensable in the industry. HeadPowder, with its expertise and commitment to quality, continues to provide advanced solutions that meet the evolving needs of cereal processing facilities, ensuring optimal performance and product integrity.




