HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of specialized equipment for handling ammonium bicarbonate powder. This article explores the fundamental principles behind the operation of such equipment and highlights the key working scene characteristics that define its application in various industrial settings.
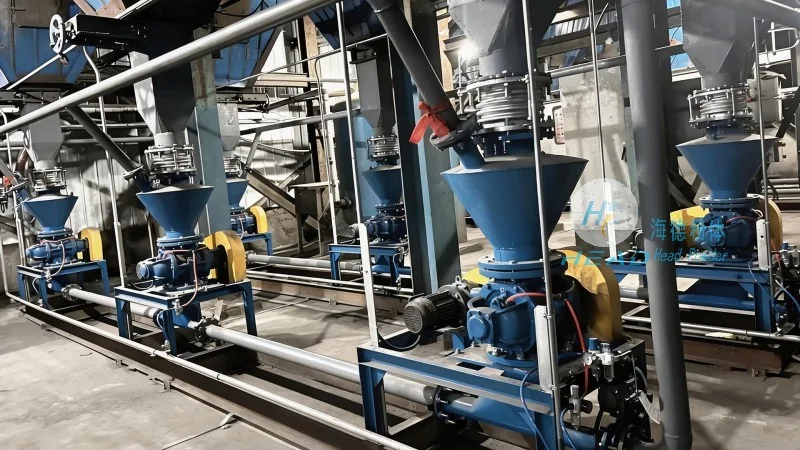
Overview of Ammonium Bicarbonate Powder Handling Equipment
Ammonium bicarbonate, a white crystalline powder commonly used as a leavening agent in baking and a precursor in chemical synthesis, presents unique handling challenges due to its hygroscopic nature and fine particle size. Traditional conveying methods often struggle with issues like caking, bridging, and material degradation, which can compromise product quality and operational efficiency. To address these challenges, specialized powder handling equipment has been developed, incorporating advanced engineering solutions tailored to the specific properties of ammonium bicarbonate. The equipment is designed to maintain the integrity of the powder, prevent moisture absorption, and ensure smooth, continuous transport from storage to processing or packaging stages.
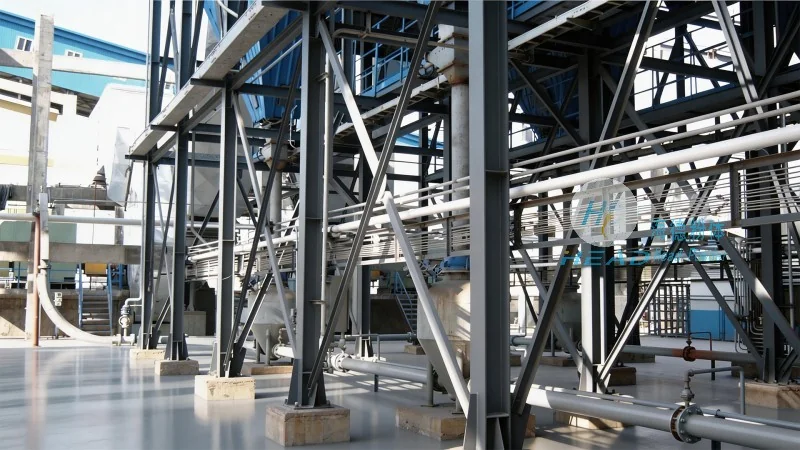
The Core Principles of Powder Conveying Systems
The operation of ammonium bicarbonate powder handling equipment is grounded in several key principles that ensure reliable and efficient material transport. One of the primary mechanisms is the use of pneumatic conveying systems, which utilize compressed air to move the powder through pipelines. This method is particularly effective for fine powders like ammonium bicarbonate, as it minimizes particle attrition and reduces the risk of blockages. Specifically, positive pressure systems, where air is blown into the pipeline, are commonly used for horizontal or slightly inclined conveying, while negative pressure systems, where air is drawn from the pipeline, are preferred for vertical or long-distance transport. The equipment also incorporates features such as rotary valves, which act as airlocks to control the flow of material and prevent backflow, ensuring a consistent and controlled discharge. Additionally, the use of flexible hoses and adjustable speed controls allows for precise regulation of the conveying rate, adapting to varying production demands. The system may also include dust collection and filtration components to maintain air quality and comply with environmental regulations.
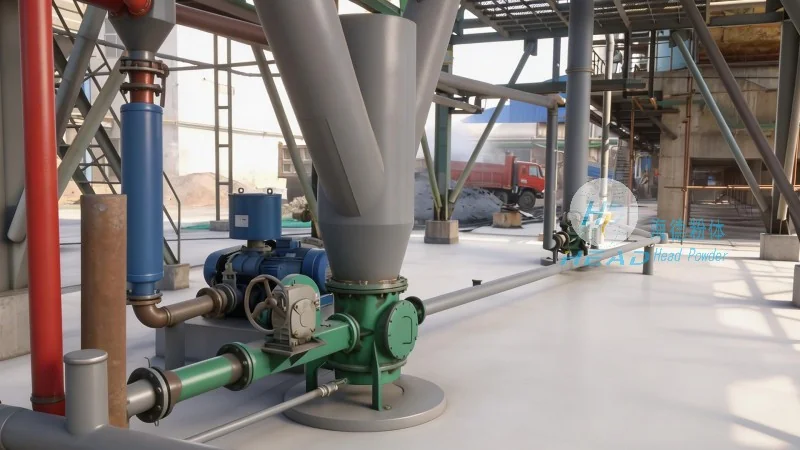
Working Scene Characteristics and Application Scenarios
The working scene characteristics of ammonium bicarbonate powder handling equipment are closely tied to the specific industrial environments where it is deployed. In baking and food processing facilities, the equipment is often integrated into production lines to transport the powder from storage silos to mixing and packaging stations. The design emphasizes hygiene and easy cleaning, as the equipment must comply with food safety regulations. The equipment may feature stainless steel construction and sanitary fittings to prevent contamination. In chemical manufacturing plants, the system may be part of larger production lines for the synthesis of ammonium bicarbonate or related compounds, where the equipment handles larger volumes and operates under more rigorous conditions. Here, the focus is on durability and resistance to corrosion, with materials like stainless steel and special coatings used to withstand the chemical environment.
Key Features and Advantages in Practical Applications
Practical applications of ammonium bicarbonate powder handling equipment showcase several advantages that enhance operational performance. For instance, the equipment’s ability to handle hygroscopic materials without causing caking or moisture absorption is a significant benefit. This is achieved through the use of sealed systems and controlled humidity levels within the conveying lines. Another advantage is the equipment’s adaptability to different production scales, from small-scale laboratory applications to large-scale industrial operations. The modular design allows for easy expansion or integration with existing production infrastructure, reducing downtime and installation costs. Furthermore, the equipment’s low maintenance requirements and long service life contribute to overall operational cost savings. The use of advanced sensors and monitoring systems can also provide real-time data on material flow and system performance, enabling proactive maintenance and optimizing production efficiency.
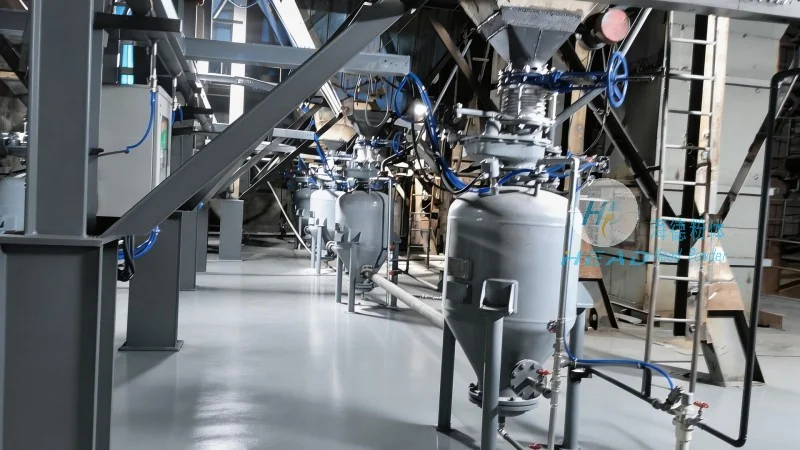
Conclusion and Company Expertise
HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, leverages decades of experience in powder handling technology to provide customized solutions for ammonium bicarbonate powder handling. The company’s commitment to innovation and adherence to industry standards ensures that their equipment meets the highest performance and safety requirements. By understanding the unique properties of ammonium bicarbonate and the specific demands of various working scenes, HeadPowder delivers reliable and efficient powder handling systems that enhance productivity and product quality in industrial applications. With a focus on customer-centric solutions, HeadPowder continues to lead the industry in developing advanced powder handling equipment tailored to the evolving needs of modern manufacturing.




