HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, production, and supply of advanced dust-free and airtight pneumatic conveying equipment. Our systems are engineered to handle bulk materials efficiently while maintaining a clean and safe working environment. This article delves into the operation process and working principle of our bulk material pneumatic conveying machines, highlighting their key features and benefits.
Understanding the Core Components of the Pneumatic Conveying System
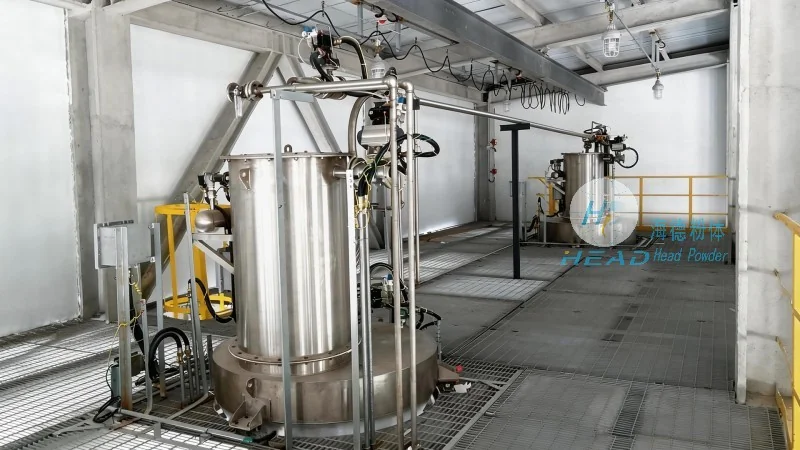
The dust-free bulk material pneumatic conveying system from HeadPowder consists of several critical components that work in tandem to ensure reliable material transport. These include the material hopper, feeder, air compressor, conveying pipeline, and dust collection unit. Each component plays a vital role in the overall operation, contributing to the system's efficiency and performance.
Step-by-Step Operation Process of the Pneumatic Conveying Machine
The operation of the dust-free pneumatic conveying machine follows a systematic process, starting with material loading into the hopper. The feeder then regulates the flow of material into the conveying pipeline, where it is propelled by compressed air. The air compressor provides the necessary pressure to move the material through the pipeline, while the dust collection system ensures that no particles are released into the environment. The process concludes with the material being discharged at the destination point, ready for further processing or use.
Working Principle of the Airtight Pneumatic Conveying Technology
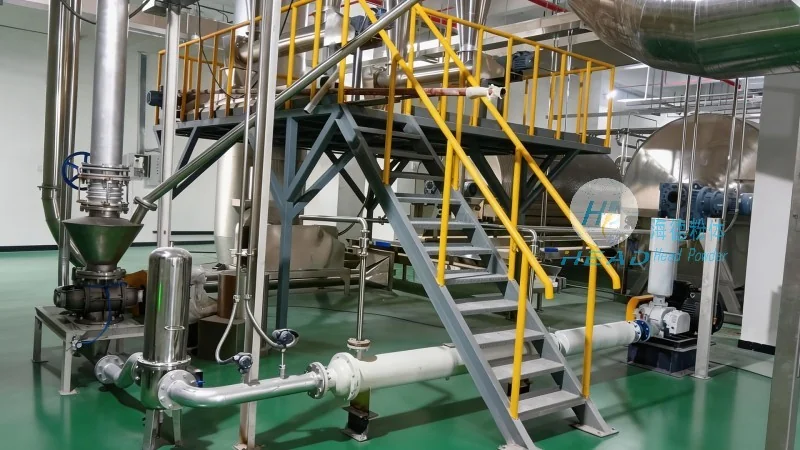
The working principle of the airtight pneumatic conveying system is based on the principle of air flow and pressure differential. When the air compressor generates high-pressure air, it creates a flow that draws the bulk material from the hopper into the conveying pipeline. The material is then carried along the pipeline by the moving air, maintaining an airtight seal to prevent dust leakage. The system uses a combination of positive and negative pressure to control the flow of material, ensuring precise and controlled transport. The dust collection unit works in conjunction with the conveying system to capture any particles that may escape, maintaining a clean and safe operation.
Key Advantages of HeadPowder's Dust-Free Pneumatic Conveying Equipment
Our dust-free and airtight pneumatic conveying machines offer several advantages over traditional material handling methods. These include improved safety by eliminating dust exposure, enhanced efficiency through continuous material flow, and reduced maintenance costs due to the airtight design. The systems are also designed to handle a wide range of bulk materials, from powders to granules, with minimal product degradation. Additionally, the airtight design helps maintain product quality by preventing contamination and moisture absorption.
Applications and Industries Served by HeadPowder's Pneumatic Conveying Systems
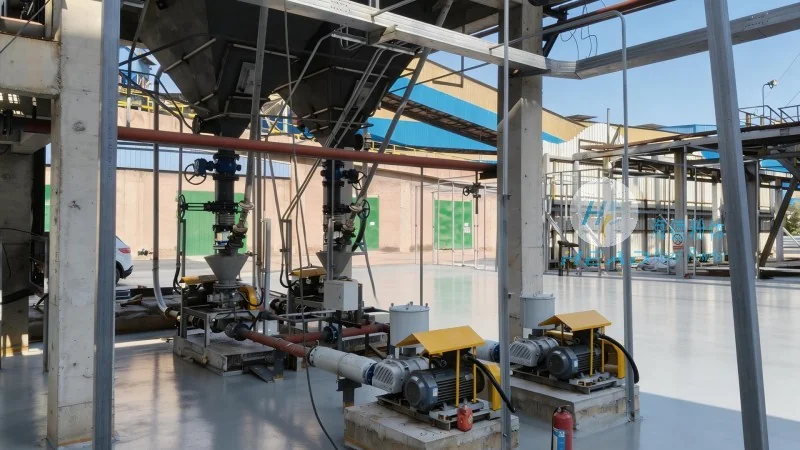
HeadPowder's dust-free pneumatic conveying systems are widely used in various industries, including food processing, pharmaceuticals, chemicals, and mining. These systems are particularly suitable for applications where dust control and product purity are critical. For example, in the food industry, the systems are used to transport ingredients such as flour, sugar, and spices without compromising their quality. In the pharmaceutical industry, the airtight design ensures that the materials are handled in a sterile environment, meeting regulatory requirements. The systems are also used in the chemical industry to transport powders and granules, reducing the risk of explosion and fire hazards.
Conclusion: Reliable and Efficient Material Handling Solutions from HeadPowder
HeadPowder's dust-free and airtight bulk material pneumatic conveying equipment provides a reliable and efficient solution for material handling needs. The systems are designed to meet the highest standards of safety, efficiency, and product quality. With our expertise in pneumatic conveying technology, we offer customized solutions tailored to the specific requirements of our clients. Whether you are in the food, pharmaceutical, chemical, or mining industry, HeadPowder's systems can help you achieve optimal material handling performance while maintaining a clean and safe working environment.




