HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for handling rare earth crystal powders. This article provides an overview of the equipment, its structural design, and the underlying principles that enable efficient material transport.
Company Profile and Background
HeadPowder Engineering Co., Ltd. is a professional enterprise dedicated to the research, development, and manufacturing of pneumatic conveying solutions. With a strong focus on precision engineering and material handling technologies, the company has established itself as a trusted partner in the industry. HeadPowder's headquarters is located in Shandong, China, where the company leverages local industrial resources and expertise to deliver high-quality equipment.
Overview of Rare Earth Crystal Powder Pneumatic Conveying Equipment
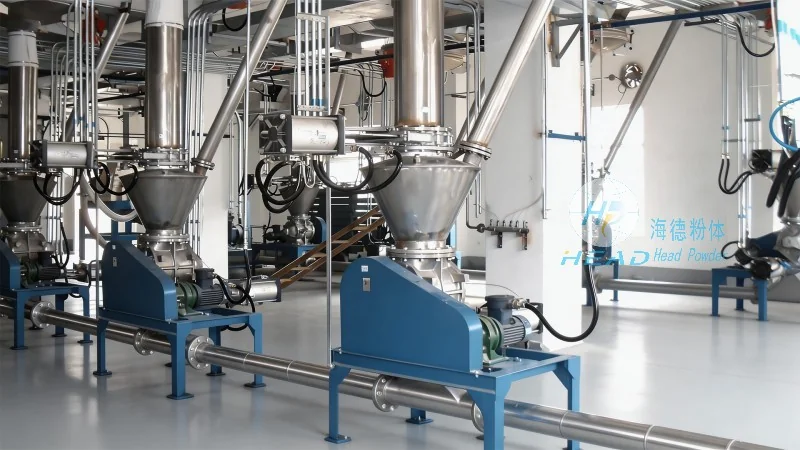
The pneumatic conveying equipment for rare earth crystal powders is engineered to handle fine, abrasive, and potentially sensitive materials with minimal degradation. This system is designed to replace traditional bulk material handling methods, such as belt conveyors or screw conveyors, which may cause contamination or material loss. The equipment operates by using compressed air to transport the powder through a pipeline network, ensuring a clean, dust-free, and efficient transfer process.
Structural Components and Design
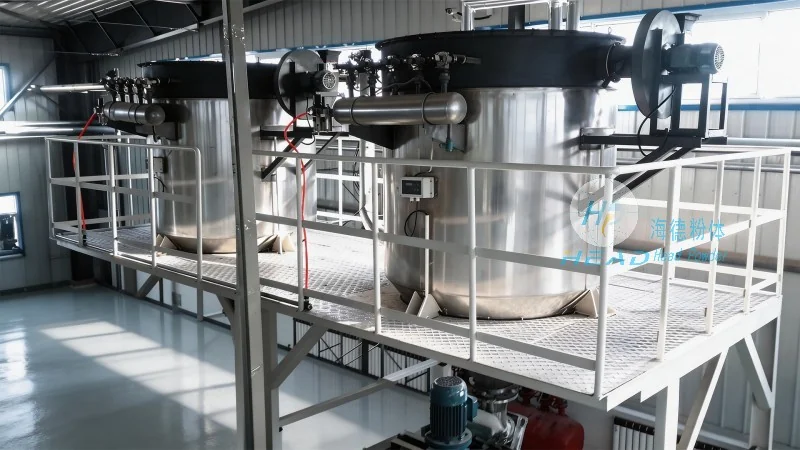
The core components of the rare earth crystal powder pneumatic conveying system include a feeding hopper, a rotary valve, a conveying pipeline, a dust collection system, and a receiving hopper. The feeding hopper is equipped with a material level indicator and a discharge valve to control the flow of powder into the system. The rotary valve, typically a star valve or slide valve, acts as a controlled gate to regulate the material feed rate, preventing overloading and ensuring consistent air-powder ratio. The conveying pipeline is constructed from corrosion-resistant materials, such as stainless steel or special alloys, to withstand the chemical properties of rare earth powders and prevent material buildup or clogging. The pipeline system includes bends, expansion joints, and check valves to maintain smooth flow and prevent backflow. The dust collection system, often a cyclone separator or a bag filter, captures any fine particles that may escape during the conveying process, ensuring environmental compliance and product purity. The receiving hopper is designed to store the conveyed powder and includes a discharge valve for downstream processing or packaging.
Working Principle of the Pneumatic Conveying System
The operation of the rare earth crystal powder pneumatic conveying system is based on the principle of air-powder mixture transport. Compressed air is introduced into the feeding hopper, creating a low-pressure zone that draws the powder into the pipeline. The air and powder mixture travels through the conveying pipeline at a controlled velocity, typically ranging from 15 to 30 meters per second, depending on the material characteristics and system design. The air flow rate is carefully adjusted to maintain a stable suspension of the powder particles, preventing settling or clogging. At the receiving end, the air is separated from the powder using a dust collection device, and the purified air is either vented to the atmosphere or recycled back into the system. The separated powder is collected in the receiving hopper, ready for further processing or use.
Key Technical Features and Advantages
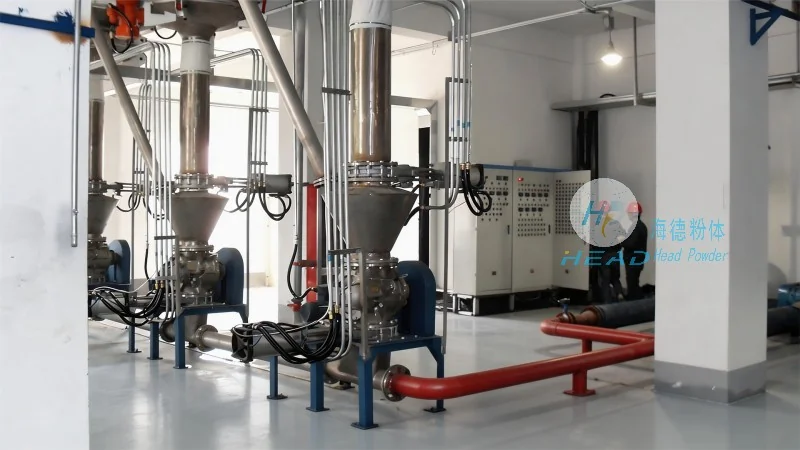
HeadPowder's rare earth crystal powder pneumatic conveying equipment offers several advantages over traditional handling methods. Firstly, the system provides a dust-free and hygienic environment, which is critical for maintaining the purity of rare earth powders, which are often used in high-value applications such as electronics, magnets, and catalysts. Secondly, the equipment minimizes material degradation by reducing friction and impact during transport, preserving the particle size distribution and chemical properties of the powder. Thirdly, the system is highly flexible and can be integrated with existing production lines, allowing for easy expansion or modification. Additionally, the equipment is designed for low maintenance, with components such as the rotary valve and pipeline system constructed from durable materials that resist wear and corrosion. The use of advanced control systems enables precise regulation of the air flow and powder feed rate, ensuring consistent performance and reducing operational costs.
Application Scenarios and Industries
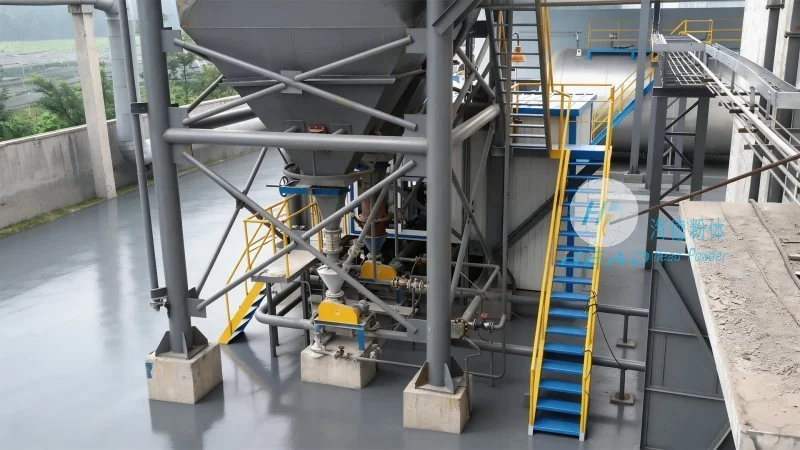
The rare earth crystal powder pneumatic conveying equipment is widely used in various industries that rely on the handling of fine powders. In the rare earth industry, the equipment is used to transport raw materials from storage silos to processing plants, ensuring a continuous and efficient supply chain. In the electronics industry, the system is employed to convey rare earth powders used in the production of permanent magnets, which are essential components in electric motors and generators. The equipment is also utilized in the chemical industry for the transport of catalysts and additives, where maintaining product purity is paramount. Furthermore, the system is suitable for applications in the aerospace and automotive sectors, where high-performance materials require precise handling and minimal contamination.
Conclusion and Service Commitment
HeadPowder Engineering Co., Ltd. provides comprehensive solutions for the pneumatic conveying of rare earth crystal powders, combining advanced engineering, quality materials, and reliable performance. The company's commitment to customer satisfaction and technological innovation ensures that clients receive equipment tailored to their specific needs. With a strong presence in Shandong, China, HeadPowder continues to lead the industry in the development of efficient and sustainable material handling systems for rare earth materials. By leveraging its expertise and experience, the company aims to support the growth and success of its clients in the global market.




