For industries dealing with fine chemicals, the selection of an appropriate material handling system is crucial. A fine chemicals pneumatic conveying system is a specialized solution designed to transport powders and granules efficiently and safely. This article explores the fundamental aspects of such systems, including their design principles and the key considerations for implementation.
Understanding Pneumatic Conveying Technology
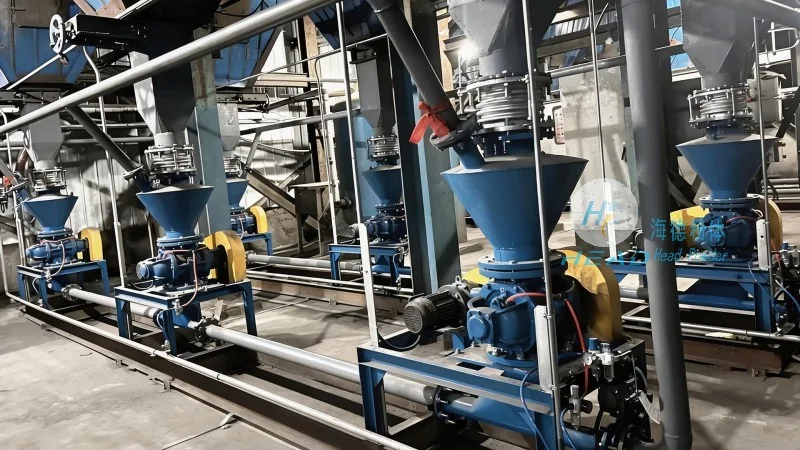
Pneumatic conveying systems utilize air or other gases to move bulk materials from one location to another. In the context of fine chemicals, these systems are engineered to handle materials with specific properties, such as low bulk density, high reactivity, or sensitivity to moisture. The technology offers several advantages over traditional methods like belt conveyors or bucket elevators, including reduced product contamination, improved process control, and enhanced safety.
Key Design Principles of Fine Chemicals Pneumatic Conveying Systems
The design of a fine chemicals pneumatic conveying system involves several critical principles to ensure optimal performance and compliance with industry standards. These principles include:
- Material Compatibility: The system components must be compatible with the specific chemical properties of the fine chemicals being transported. This includes considerations of corrosion resistance, chemical inertness, and temperature stability.
- Pressure and Flow Control: Precise control of air pressure and flow rate is essential to maintain consistent material transport and prevent issues like blockages or excessive wear.
- System Layout and Configuration: The layout of the conveying system, including the number and type of ducts, bends, and filters, is carefully designed to minimize pressure losses and ensure smooth material flow.
- Filter and Dust Collection: Efficient filtration systems are integral to maintaining air quality and preventing product loss or contamination. High-efficiency particulate air (HEPA) filters are commonly used to capture fine particles and ensure compliance with environmental regulations.
Components of a Fine Chemicals Pneumatic Conveying System
A typical fine chemicals pneumatic conveying system consists of several key components, each playing a vital role in the overall operation. These components include:
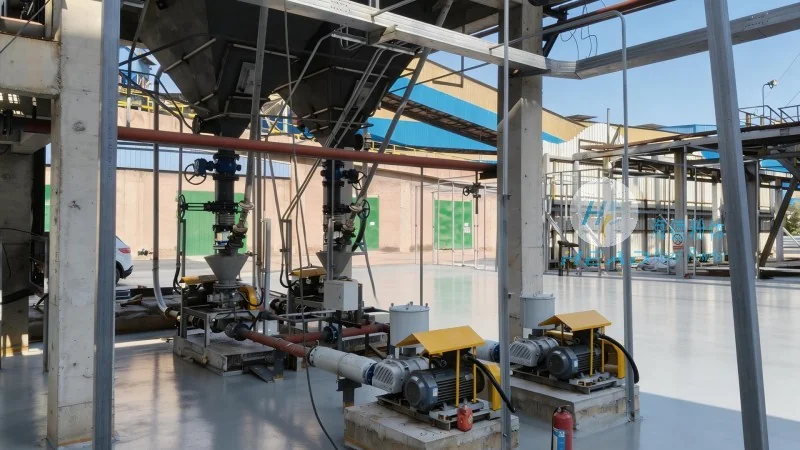
- Feeder: The feeder is responsible for feeding the material into the conveying line at a controlled rate. For fine chemicals, this may involve rotary valves, screw feeders, or vibratory feeders to ensure consistent and gentle material introduction.
- Ductwork: The ducts are the primary conduits for transporting the material and air mixture. They are typically made of materials like stainless steel or PTFE to prevent corrosion and ensure chemical compatibility.
- Conveying Air System: This includes the air compressor, filters, and regulators that provide the necessary air pressure and quality for the conveying process.
- Receiver: The receiver is the final destination for the material, where it is collected and stored. It is designed to minimize product loss and ensure easy access for maintenance.
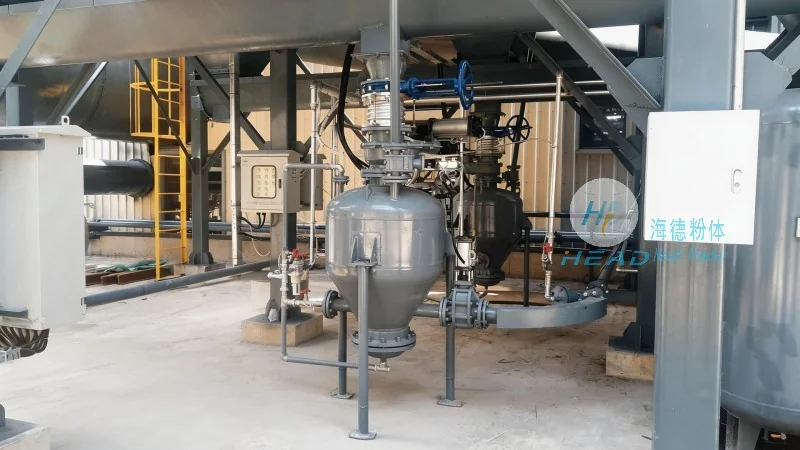
- Filter and Dust Collector: As mentioned earlier, these components are crucial for maintaining air quality and preventing environmental contamination.
Applications in the Fine Chemicals Industry
Fine chemicals pneumatic conveying systems are widely used in various applications within the fine chemicals industry. These include:
- Pharmaceutical Manufacturing: Transporting active pharmaceutical ingredients (APIs), excipients, and other powders with high purity requirements.
- Food and Beverage Processing: Handling ingredients like spices, flavors, and colorants, where contamination control is paramount.
- Chemical Production: Moving raw materials and intermediates in the production of specialty chemicals, such as pigments, coatings, and adhesives.
- Biotechnology: Conveying powders and granules used in bioprocessing, including fermentation products and cell cultures.
Benefits of Using Fine Chemicals Pneumatic Conveying Systems
Implementing a fine chemicals pneumatic conveying system offers numerous benefits for industrial operations. These benefits include:
- Improved Product Quality: Reduced product contamination and minimal exposure to air and moisture help maintain the quality and stability of fine chemicals.
- Enhanced Process Efficiency: Precise control of material flow and pressure leads to optimized production rates and reduced downtime.
- Increased Safety: Enclosed systems minimize dust exposure and prevent accidental spills or releases, improving workplace safety.
- Space Efficiency: Pneumatic conveying systems can be designed to fit into compact spaces, making them suitable for facilities with limited floor area.
- Environmental Compliance: Efficient filtration systems ensure compliance with environmental regulations regarding air emissions and waste disposal.
Choosing the Right System Provider
When selecting a pneumatic conveying system for fine chemicals applications, it is essential to partner with a reputable and experienced provider. Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer specializing in custom-designed material handling solutions for the fine chemicals industry. With years of experience and a commitment to quality, headpowder offers comprehensive services, including system design, manufacturing, installation, and maintenance.
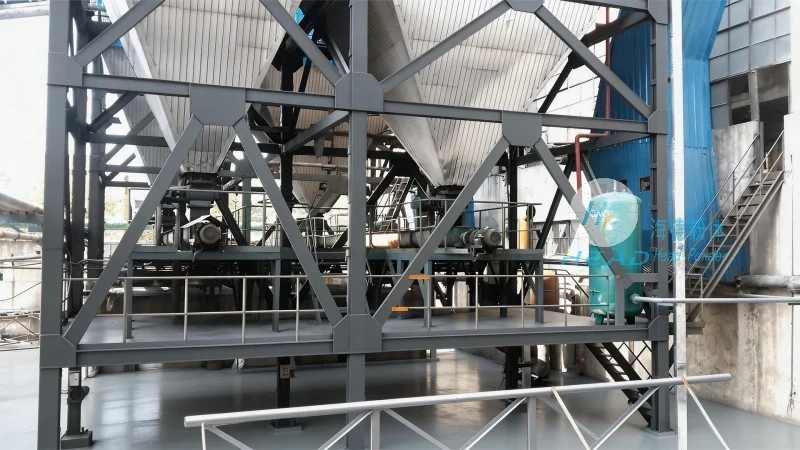
Headpowder’s team of engineers works closely with clients to understand their specific process requirements and material characteristics. This collaborative approach ensures that the final system is tailored to meet the unique needs of each application, providing optimal performance and reliability. The company’s facilities are equipped with advanced technology and adheres to international standards, ensuring that all products meet the highest quality and safety standards.
Headpowder’s location in Shandong, China, provides a strategic advantage for clients seeking cost-effective and efficient solutions. The company’s proximity to major industrial hubs and its extensive supply chain network enable timely delivery and support. By choosing headpowder, clients can benefit from a reliable partner that delivers customized pneumatic conveying systems designed to enhance their operational efficiency and product quality.




