Denitrizer powder conveying systems are critical components in industrial processes that require the efficient transport of powder materials, particularly in applications related to flue gas treatment and environmental control. These systems are designed to handle denitrizer powders, which are essential for reducing nitrogen oxide emissions from industrial facilities. Understanding the working principle and key features of such systems is vital for optimizing operational efficiency and ensuring compliance with environmental regulations.
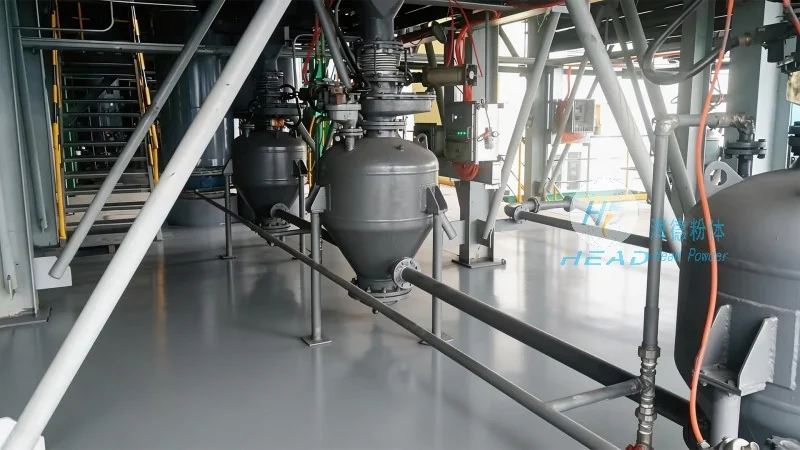
HeadPowder, a leading provider of engineering solutions in China, specializes in the design, manufacturing, and installation of advanced powder conveying systems. With a focus on innovation and reliability, the company’s systems are tailored to meet the specific demands of various industrial sectors, including power generation, chemical manufacturing, and environmental protection. The company’s headquarters is located in Shandong, China, where it leverages local expertise and resources to deliver high-quality solutions.
The Working Principle of Denitrizer Powder Conveying Systems
The core working principle of denitrizer powder conveying systems revolves around the use of pneumatic or mechanical methods to transport powder materials from a source to a destination. In many industrial applications, pneumatic conveying is the preferred method due to its ability to handle fine powders and provide a clean, dust-free operation. The system typically consists of several key components, including a hopper for material storage, a feeder to control the flow rate, a conveying line (often equipped with air pipes or mechanical components), and a receiver for the delivered material.
During operation, the denitrizer powder is first loaded into the hopper. The feeder then regulates the amount of powder released into the conveying line. In pneumatic systems, compressed air is introduced to create a flow that carries the powder particles through the line. The air and powder mixture travels to the receiver, where the air is separated from the powder, often through a cyclone or filter system. This separation process ensures that the powder is delivered to the target location without contamination or loss of material.
Mechanical conveying systems, such as screw conveyors or belt conveyors, may also be used for denitrizer powder transport. These systems rely on mechanical components to move the powder through a closed or open channel. Screw conveyors use rotating screws to push the powder forward, while belt conveyors utilize moving belts to transport the material. Both methods are effective for handling bulk quantities of powder but may require more maintenance and are less suitable for fine powders that are prone to clogging.
Key Features of Denitrizer Powder Conveying Systems
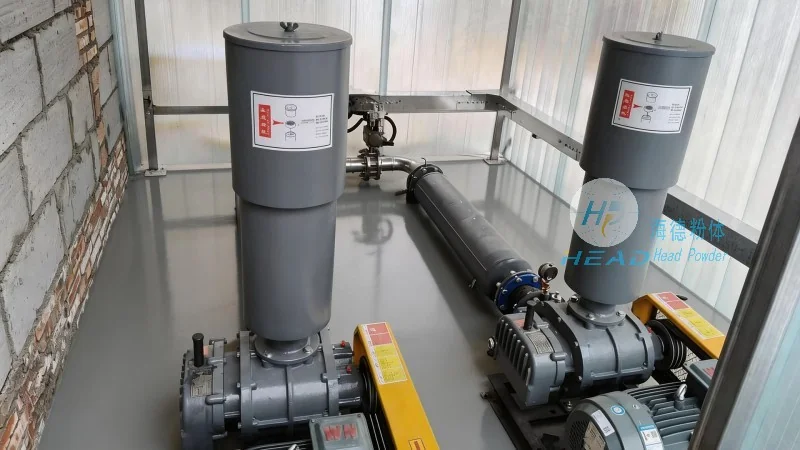
Denitrizer powder conveying systems from HeadPowder are characterized by several key features that enhance performance and reliability. One of the primary features is the ability to handle fine and abrasive powders without causing wear or damage to the system components. The materials used in the construction of the conveying equipment, such as stainless steel or specialized alloys, are chosen to withstand the corrosive and abrasive nature of denitrizer powders.
Another important feature is the system’s efficiency in terms of energy consumption and operational costs. Advanced designs incorporate energy-saving mechanisms, such as variable speed drives and optimized air flow, to reduce power usage while maintaining consistent material transport. This not only lowers operational expenses but also contributes to environmental sustainability by minimizing energy waste.
System flexibility is also a critical feature, allowing for adjustments to accommodate varying powder quantities and flow rates. This adaptability is essential in dynamic industrial environments where production demands may fluctuate. HeadPowder’s systems are designed with modular components that can be easily reconfigured or expanded to meet changing operational requirements.
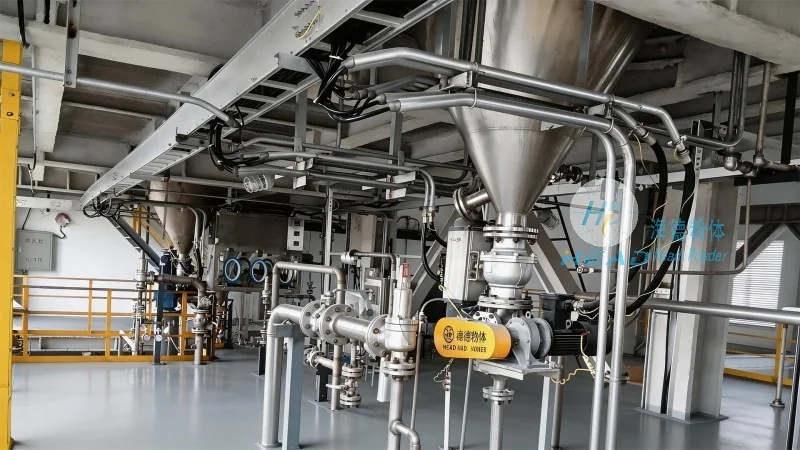
Additionally, the systems are equipped with advanced monitoring and control technologies. Sensors and control panels provide real-time data on flow rates, pressure, and material levels, enabling operators to monitor performance and detect potential issues promptly. This proactive approach to maintenance helps prevent downtime and ensures the system operates at optimal efficiency.
Applications and Benefits
Denitrizer powder conveying systems are widely used in industries where precise control of nitrogen oxide emissions is critical. In power plants, for example, these systems are integral to the flue gas treatment process, ensuring that denitrizer powders are delivered to the reaction zones efficiently. The benefits of using such systems include improved process control, reduced environmental impact, and enhanced safety by minimizing dust exposure and handling risks.
HeadPowder’s denitrizer powder conveying systems offer significant advantages over traditional methods, such as manual handling or less efficient conveying technologies. By automating the powder transport process, the company’s solutions reduce labor costs, improve product quality, and enhance overall operational reliability. The systems are also designed to be compatible with existing industrial infrastructure, minimizing installation time and disruption.
In conclusion, denitrizer powder conveying systems are essential for modern industrial operations that prioritize environmental compliance and operational efficiency. HeadPowder, with its expertise and commitment to quality, provides advanced solutions that address the unique challenges of powder transport in denitrization applications. By understanding the working principle and key features of these systems, industries can make informed decisions to enhance their processes and meet regulatory requirements effectively.




