Soil powder conveying equipment is a specialized system designed to transport loose, powdery materials such as soil, sand, and other fine particulate substances efficiently and reliably. Understanding its working principle and key features is essential for selecting the right equipment for various industrial applications. This article explores the fundamental mechanisms behind these systems and highlights the advantages that make them indispensable in modern material handling operations.
About HeadPowder: A Leading Provider of Soil Powder Conveying Solutions
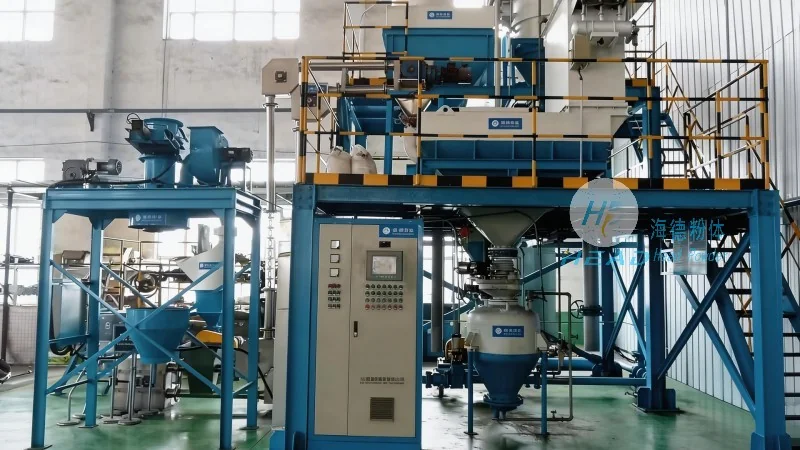
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a prominent manufacturer based in China. With a strong commitment to innovation and quality, the company specializes in developing advanced soil powder conveying equipment tailored to meet the diverse needs of construction, mining, and environmental industries. HeadPowder's headquarters is located in Shandong, China, where the company leverages local expertise and resources to deliver reliable and efficient solutions for material transport challenges.
The Working Principle of Soil Powder Conveying Equipment
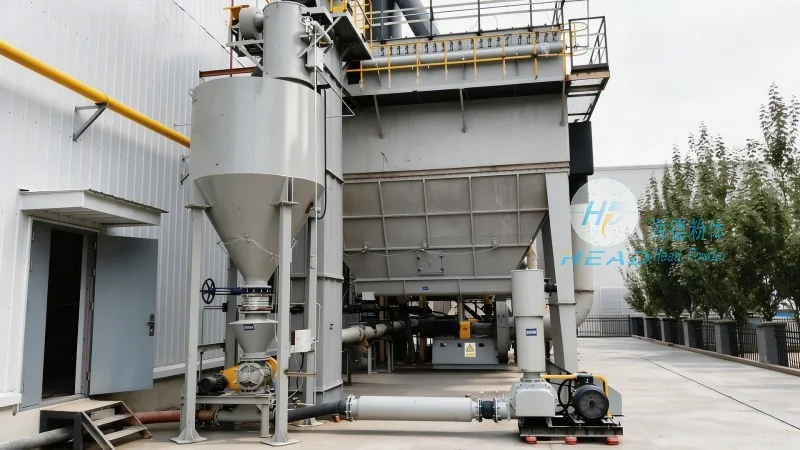
At the core of soil powder conveying equipment is a mechanism that uses air or mechanical force to move powdery materials through a pipeline. The most common type is the pneumatic conveyor, which operates by creating a pressure differential between the inlet and outlet of the system. Air is drawn into the system, carrying the soil particles along with it. The equipment typically consists of a hopper for material loading, a blower or compressor to generate airflow, and a pipeline network that directs the material to its destination. The working principle involves several key steps: material is fed into the hopper, air is introduced to create a flow, and the mixture of air and particles moves through the pipeline under controlled pressure. This process ensures that the soil powder is transported without clogging or degradation, maintaining the integrity of the material throughout the conveying process.
Key Features of Soil Powder Conveying Equipment
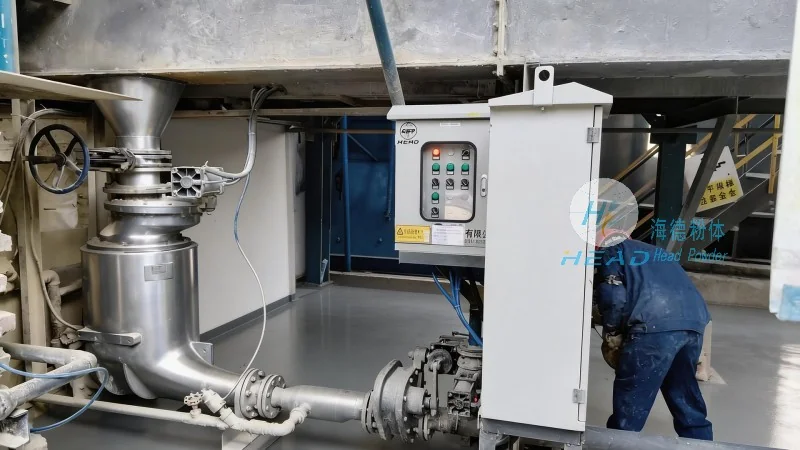
Soil powder conveying equipment from HeadPowder is characterized by several features that enhance performance and reliability. One of the primary advantages is its ability to handle fine, abrasive materials without causing wear or damage to the system components. The equipment is designed with durable materials, such as stainless steel or high-grade plastics, to withstand the corrosive and abrasive nature of soil particles. Additionally, the system offers adjustable airflow and pressure settings, allowing operators to optimize the conveying rate based on the specific characteristics of the material being transported. This flexibility ensures efficient transport even with varying particle sizes and moisture content. Another key feature is the system's low maintenance requirements, as the pneumatic design minimizes mechanical parts that could fail or require frequent replacement. The equipment also provides precise control over the material flow, enabling accurate delivery to the target location. Furthermore, HeadPowder's soil powder conveyors are equipped with safety features, such as pressure relief valves and overload protection, to prevent accidents and ensure safe operation in industrial environments.
Applications and Benefits in Industrial Settings
Soil powder conveying equipment is widely used in various industrial applications where the transport of loose, powdery materials is critical. In the construction industry, these systems are employed to move soil and sand from excavation sites to processing facilities or disposal areas. The equipment's ability to handle large volumes of material efficiently reduces labor costs and improves project timelines. In mining operations, soil powder conveyors are used to transport ore and tailings, ensuring safe and reliable material handling in hazardous environments. Environmental applications also benefit from these systems, as they help in the transport of soil for reclamation projects or waste management. The benefits of using soil powder conveying equipment include increased productivity, reduced labor costs, and improved safety due to the automated nature of the process. Additionally, the equipment minimizes material loss and contamination, as the sealed pipeline system prevents dust and particles from escaping into the environment. This not only enhances operational efficiency but also contributes to environmental sustainability.
Conclusion
In summary, soil powder conveying equipment operates on a principle of air-assisted transport, efficiently moving fine particulate materials through a pipeline system. HeadPowder, a leading manufacturer based in Shandong, China, offers advanced solutions with durable construction, adjustable settings, and safety features that address the unique challenges of soil and powder transport. The equipment's ability to handle abrasive materials, provide precise control, and reduce maintenance requirements makes it an essential tool in construction, mining, and environmental industries. By understanding the working principle and key features of these systems, businesses can select the most suitable equipment to enhance their material handling operations and achieve greater efficiency and productivity.




