Working Principle and Features of Coke Powder Conveying Equipment
Release time:2026-09-17 11:01:25
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
For industrial applications involving coke powder, efficient and reliable conveying equipment is essential to ensure smooth material handling processes. The working principle and features of coke powder conveying equipment are critical factors that determine its performance and suitability for various industrial environments. This article provides an in-depth exploration of the core mechanisms and distinctive characteristics of such equipment, highlighting how they contribute to optimal material transport in industrial settings.
Working Principle of Coke Powder Conveying Equipment
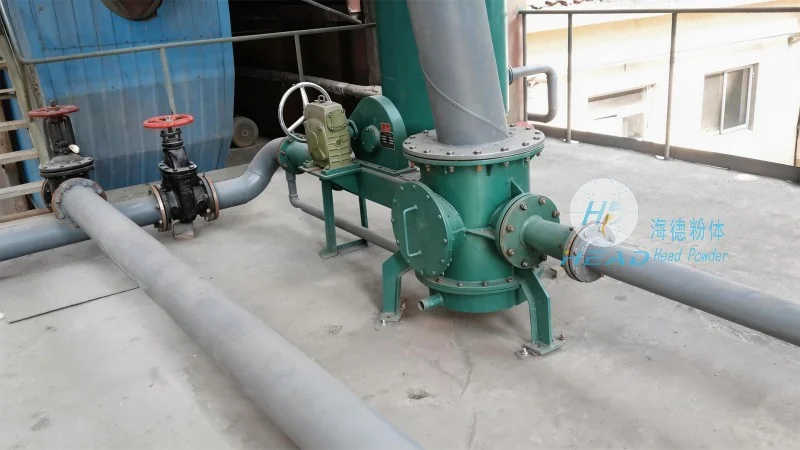
The working principle of coke powder conveying equipment typically revolves around the use of mechanical systems to transport fine coke particles from one location to another. These systems are designed to handle the unique properties of coke powder, such as its fine particle size, abrasive nature, and potential for dust generation. The primary components of a typical coke powder conveying system include a feeding mechanism, a conveying medium (like air or a fluid), and a discharge unit. The feeding mechanism ensures that the coke powder is introduced into the system in a controlled manner, preventing blockages and ensuring consistent flow. The conveying medium, often air under pressure (in pneumatic systems) or a liquid (in hydraulic systems), propels the powder through the pipeline. The discharge unit then collects the material at the destination point, completing the transport cycle. This mechanical process allows for continuous and automated material handling, reducing labor costs and improving operational efficiency.
Key Features of Coke Powder Conveying Equipment
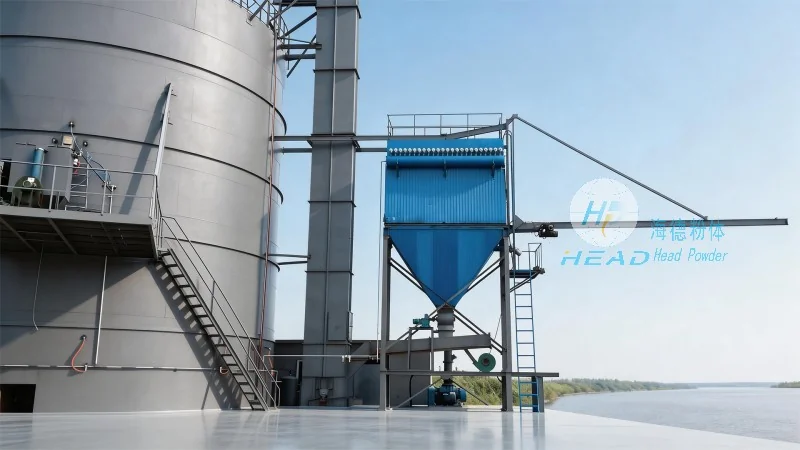
Several key features distinguish high-quality coke powder conveying equipment, making them suitable for demanding industrial applications. Firstly, these systems are designed with durability in mind, as coke powder can be abrasive and may cause wear on equipment components. Materials such as stainless steel or specialized alloys are often used for critical parts to enhance longevity and reduce maintenance requirements. Secondly, the equipment is engineered to minimize dust generation and ensure environmental compliance. Advanced sealing systems and dust collection mechanisms are integrated to prevent airborne contamination and maintain a safe working environment. Thirdly, the conveying systems are typically equipped with variable speed controls and flow regulation capabilities, allowing operators to adjust the transport rate based on production needs. This flexibility is crucial for adapting to changing material volumes or processing requirements. Additionally, modern coke powder conveying equipment often incorporates monitoring and control systems, enabling real-time tracking of material flow and system performance. These features collectively contribute to improved operational reliability, reduced downtime, and enhanced overall productivity.
Company Information: Shandong HeadPowder Engineering Co., Ltd.
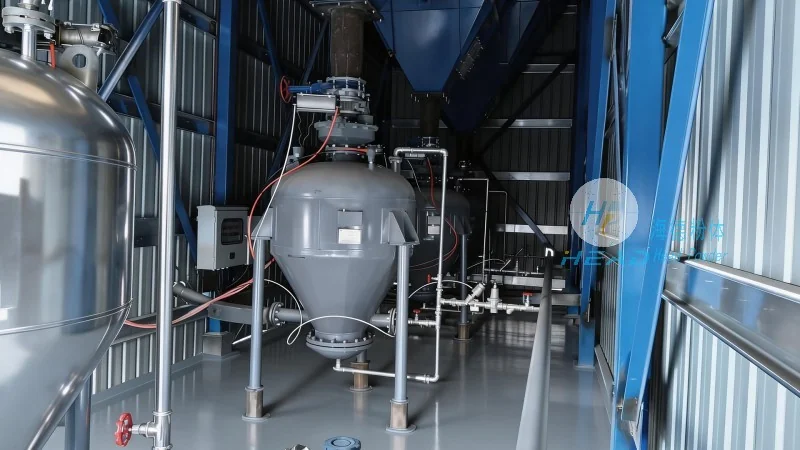
HeadPowder, a leading manufacturer of specialized conveying equipment, is dedicated to providing innovative solutions for the handling of coke powder and other fine materials. With a strong commitment to quality and customer satisfaction, the company has established itself as a trusted partner in the industrial sector. HeadPowder's products are engineered to meet the specific challenges of coke powder transport, ensuring reliable performance in demanding environments. The company's headquarters is located in Shandong, China, where it leverages advanced manufacturing technologies and experienced engineering expertise to develop cutting-edge conveying solutions. By focusing on the unique requirements of coke powder handling, HeadPowder continues to deliver equipment that enhances operational efficiency and safety for its clients.




