Phenolic resin powder conveying systems are critical components in industrial processes that handle bulk materials, particularly in sectors such as manufacturing, construction, and chemical production. These systems are designed to efficiently transport phenolic resin powders from storage to processing units, ensuring consistent flow and minimizing material loss. Understanding the working principle and key features of such systems is essential for optimizing operational efficiency and maintaining product quality.
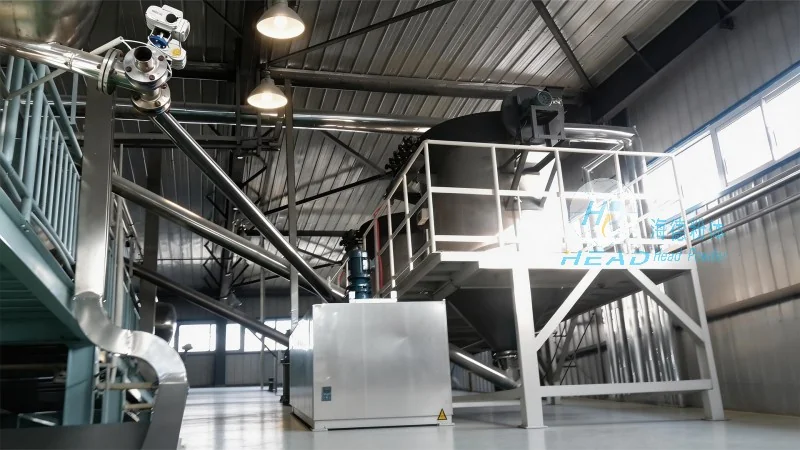
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading provider in the field, specializes in the design, manufacturing, and integration of advanced powder handling solutions. With a strong focus on innovation and customer-centric approaches, the company has established itself as a trusted partner for businesses seeking reliable phenolic resin powder conveying systems. HeadPowder’s expertise lies in tailoring solutions to meet specific operational requirements, ensuring that clients achieve optimal performance and cost-effectiveness.
The Core Working Principle of Phenolic Resin Powder Conveying Systems
The fundamental working principle of phenolic resin powder conveying systems revolves around the use of mechanical or pneumatic mechanisms to move powder materials through a network of pipes, hoppers, and control valves. Typically, these systems employ a combination of gravity, pressure, or vacuum to facilitate material transport. The process begins with the storage of phenolic resin powder in bulk containers or silos, where the system draws the material into a hopper or feeder. From there, the powder is conveyed through a series of pipes, often using positive displacement pumps or air-driven systems, to the processing equipment. The system’s control panel monitors and regulates the flow rate, pressure, and temperature to maintain consistent performance and prevent issues like clogging or material degradation.
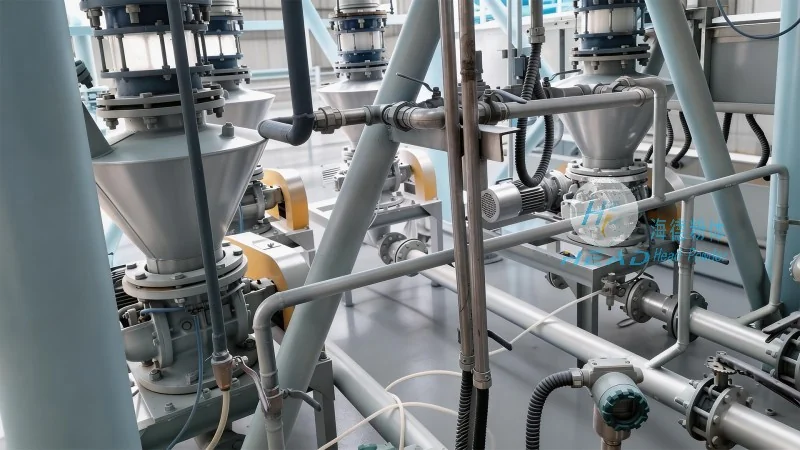
Key Features of Phenolic Resin Powder Conveying Systems
Phenolic resin powder conveying systems from HeadPowder are characterized by several key features that enhance their functionality and reliability. First, the systems are designed with robust materials to withstand the abrasive nature of phenolic resin powders, ensuring long-term durability and minimal maintenance. Advanced sealing technologies are employed to prevent dust emissions and maintain a clean working environment, which is crucial for compliance with industrial safety standards. The systems also incorporate intelligent control systems that allow for real-time monitoring and adjustment of operational parameters, enabling operators to optimize performance based on specific production needs.
Efficiency and Performance Advantages
One of the primary advantages of phenolic resin powder conveying systems is their ability to maintain consistent flow rates, which is vital for maintaining product quality and reducing downtime. The use of positive displacement pumps or air-driven mechanisms ensures that the material is transported at a steady pace, minimizing variations that could affect downstream processes. Additionally, the systems are engineered to minimize material degradation, such as agglomeration or moisture absorption, which can impact the properties of the phenolic resin. By controlling temperature and humidity within the system, HeadPowder’s solutions help preserve the integrity of the powder, ensuring that it meets the required specifications for end-use applications.
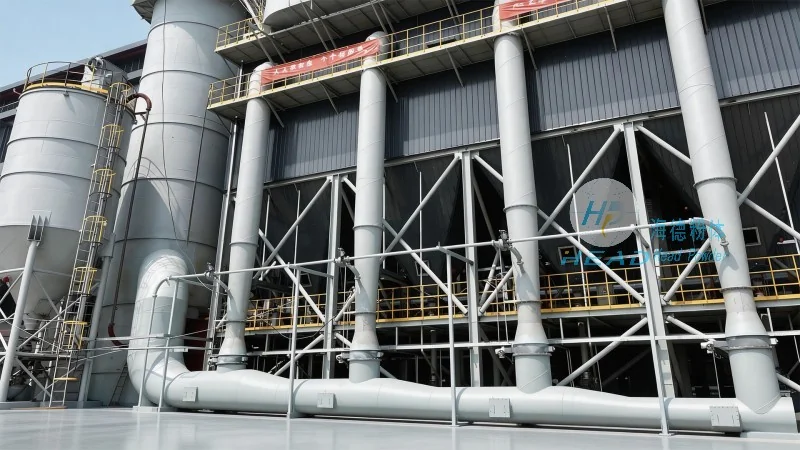
Customization and Scalability
HeadPowder understands that each industrial application has unique requirements, which is why their phenolic resin powder conveying systems are highly customizable. The company offers a range of configurations, from compact systems for small-scale operations to large-scale solutions for high-volume production. This flexibility allows clients to select a system that aligns with their current and future operational needs, ensuring long-term investment value. The systems can be integrated with existing infrastructure or designed as standalone units, providing versatility in implementation. Furthermore, HeadPowder provides comprehensive support, including installation, commissioning, and ongoing maintenance services, to ensure that clients can fully leverage the benefits of their powder conveying solutions.
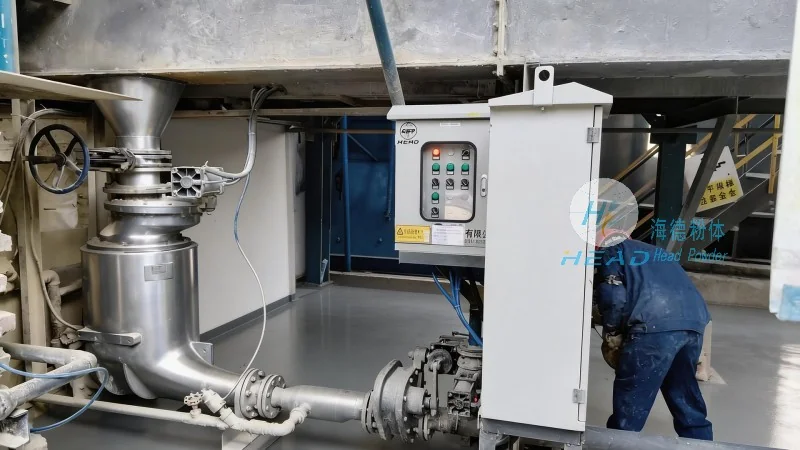
Reliability and Safety in Operation
Reliability is a cornerstone of HeadPowder’s phenolic resin powder conveying systems. The use of high-quality components and rigorous quality control processes ensures that the systems operate with minimal downtime and maximum uptime. The company adheres to international safety standards, incorporating features such as emergency stop mechanisms, pressure relief valves, and dust suppression systems to protect both personnel and equipment. These safety measures are critical in environments where phenolic resin powders are handled, as they help prevent accidents and maintain a safe working environment. By prioritizing safety and reliability, HeadPowder’s systems contribute to the overall operational efficiency and compliance of their clients’ facilities.
Conclusion and Contact Information
Phenolic resin powder conveying systems are essential for efficient material handling in various industrial applications. HeadPowder, with its expertise and commitment to quality, provides advanced solutions that combine functionality, reliability, and customization. By understanding the working principle and key features of these systems, businesses can optimize their operations, reduce costs, and maintain product quality. For more information or to explore how HeadPowder’s solutions can meet your specific needs, please contact us at Shandong HeadPowder Engineering Co., Ltd., located in China.




