Stone coal, also known as coke residue or coking byproduct, is a solid waste material generated during the coking process in the steel and chemical industries. Efficient and reliable material handling of this material is crucial for maintaining production efficiency and ensuring environmental compliance. This article explores the working principle and key features of stone coal material handling systems, providing insights into how these systems operate and their advantages in industrial applications.
Working Principle of Stone Coal Material Handling Systems
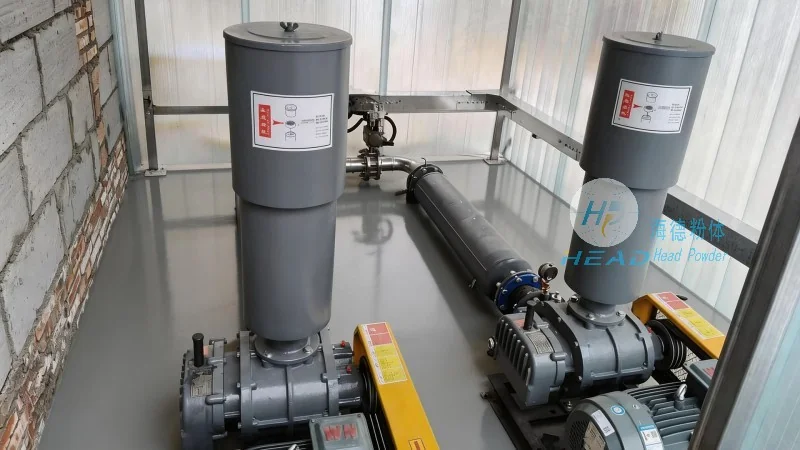
The working principle of stone coal material handling systems typically involves several integrated components designed to transport, store, and manage the material from the coking plant to disposal or further processing facilities. The process generally begins with the collection of stone coal from the coking oven or cooling system. This material is then transferred to a storage hopper or silo using conveyor belts, screw conveyors, or pneumatic systems. The primary components of the system include feeders, conveyors, and control mechanisms that work in tandem to ensure smooth material flow.
Conveyor belts are commonly used for horizontal and slight incline transport due to their high load capacity and low maintenance requirements. Screw conveyors are suitable for vertical or inclined transport, providing a compact solution for moving material through vertical shafts. Pneumatic systems, such as air slides or vacuum conveyors, are employed for fine or dusty stone coal, offering flexibility in handling different particle sizes. The control system, often integrated with sensors and automation technology, monitors the material flow rate, pressure, and temperature to maintain optimal operation and prevent blockages or overloading.
Key Features of Stone Coal Material Handling Systems
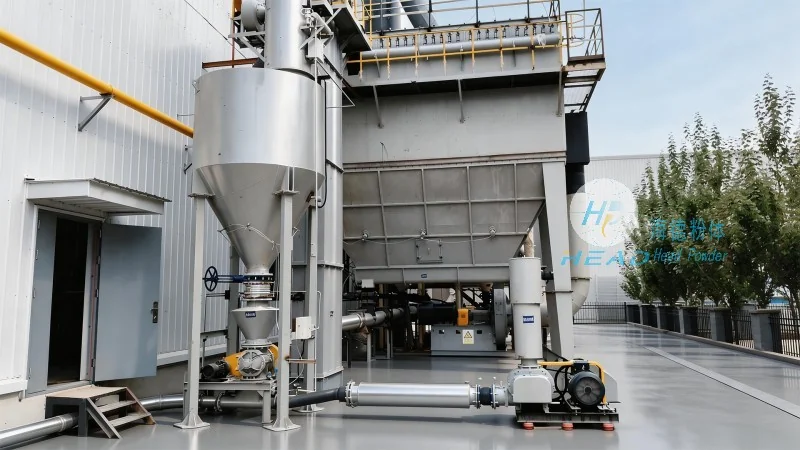
Stone coal material handling systems are designed with several key features that enhance their performance and reliability in industrial settings. One of the primary features is their high durability and resistance to wear and tear, as they are constructed from materials like stainless steel, alloy steel, or special coatings to withstand the abrasive nature of stone coal. This durability ensures long service life and reduces maintenance costs over time.
Another important feature is the system's adaptability to varying material characteristics. Modern stone coal handling systems can handle different particle sizes, moisture contents, and bulk densities, making them suitable for diverse industrial applications. The modular design allows for easy expansion or modification to accommodate changes in production capacity or material types. Additionally, these systems often incorporate safety features, such as emergency stop buttons, overload protection, and dust suppression mechanisms, to ensure safe operation and compliance with occupational health and safety regulations.
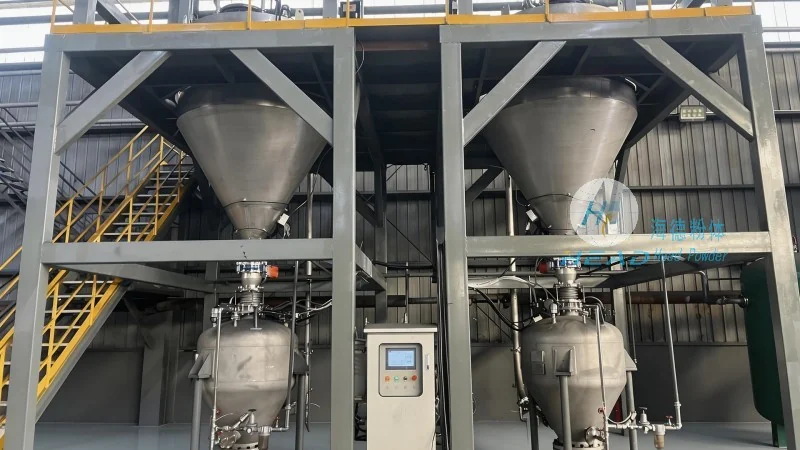
Energy efficiency is also a notable feature of contemporary stone coal material handling systems. Advanced control systems and energy-saving components, like variable frequency drives (VFDs) for conveyors, minimize energy consumption while maintaining optimal performance. This not only reduces operational costs but also aligns with environmental sustainability goals by lowering carbon emissions. Furthermore, the integration of monitoring and diagnostic tools enables predictive maintenance, allowing operators to identify and address potential issues before they lead to system failures, thereby improving overall system reliability and reducing downtime.
About Shandong HeadPowder Engineering Co., Ltd.
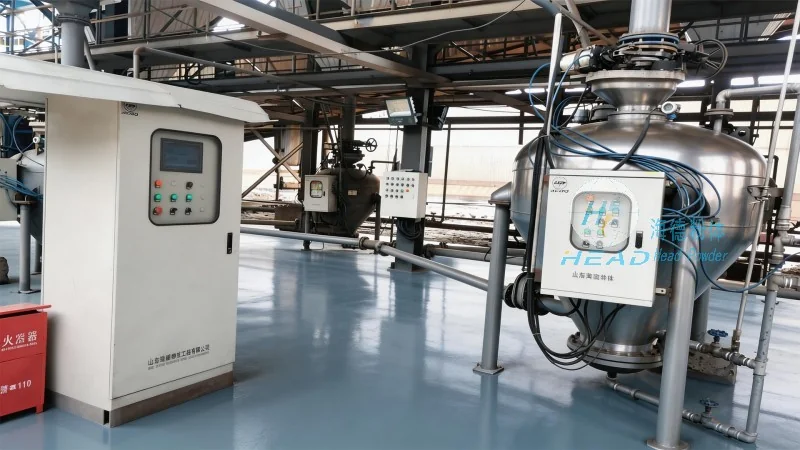
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of material handling solutions for the industrial sector. With a focus on innovation and quality, HeadPowder specializes in designing and manufacturing systems tailored to the unique needs of industries such as steel, chemical, and energy. The company's headquarters is located in Shandong, China, where it leverages local expertise and resources to develop cutting-edge technologies for material handling applications.
HeadPowder's commitment to customer satisfaction is reflected in its comprehensive product line, which includes conveyor systems, storage solutions, and automation components. The company adheres to international standards and quality certifications, ensuring that its products meet the highest industry benchmarks. By combining advanced engineering with practical application knowledge, HeadPowder provides reliable and efficient solutions that enhance operational efficiency and reduce costs for its clients. Whether for new installations or system upgrades, HeadPowder's expertise in stone coal material handling systems ensures that clients receive tailored solutions that address their specific challenges and requirements.




