Understanding the working principle and characteristics of potassium carbonate fertilizer material handling is crucial for optimizing industrial processes in agricultural and chemical sectors. This article provides a detailed overview of how such systems operate and the key attributes that define their efficiency and reliability.
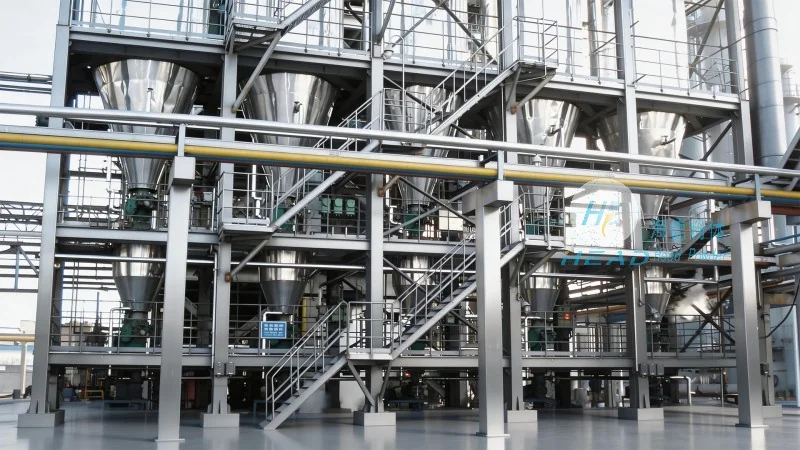
Company Introduction: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field, specializes in the design and implementation of advanced material handling solutions. With a strong presence in China, particularly in Shandong province, the company has established itself as a trusted partner for industries requiring efficient fertilizer processing and transportation. The company's expertise lies in developing customized systems that meet the specific demands of potassium carbonate fertilizer production and distribution.
The Working Principle of Potassium Carbonate Fertilizer Material Handling
Potassium carbonate fertilizer material handling systems typically operate through a series of integrated mechanisms designed to ensure safe, efficient, and continuous transport of the material. The process begins with the reception of raw materials, which are then processed through various stages including mixing, drying, and granulation if applicable. The material is then conveyed using specialized equipment such as belt conveyors, screw conveyors, or pneumatic systems, depending on the specific characteristics of the fertilizer and the operational requirements.
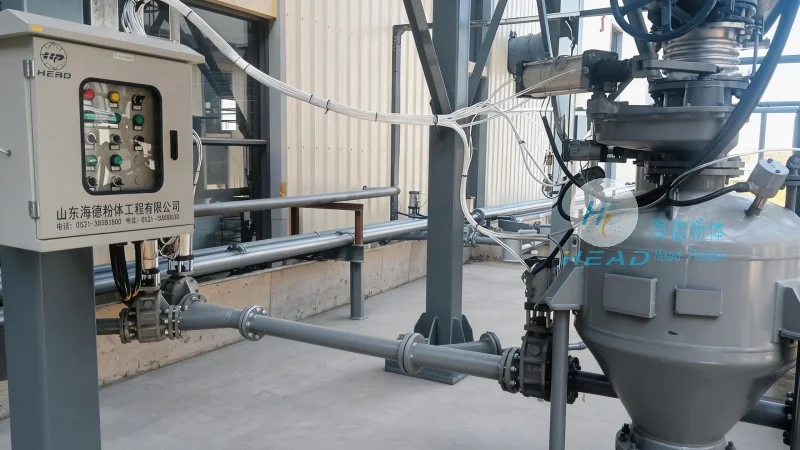
Key components of the system include feed hoppers, which regulate the flow of material into the conveyor, and control valves that adjust the speed and volume of material transport. Sensors and monitoring systems are integrated to provide real-time data on the material flow, ensuring that any deviations are immediately detected and corrected. This closed-loop control system enhances the overall efficiency and reduces the risk of material loss or blockages.
Key Characteristics of Potassium Carbonate Fertilizer Material Handling Systems
Efficiency and reliability are paramount in the design of potassium carbonate fertilizer material handling systems. These systems are engineered to handle the unique properties of potassium carbonate, such as its granular or powder form, and the potential for dust generation during transport. The use of high-quality materials and robust construction ensures that the equipment can withstand the abrasive nature of the fertilizer and operate under continuous high-load conditions.
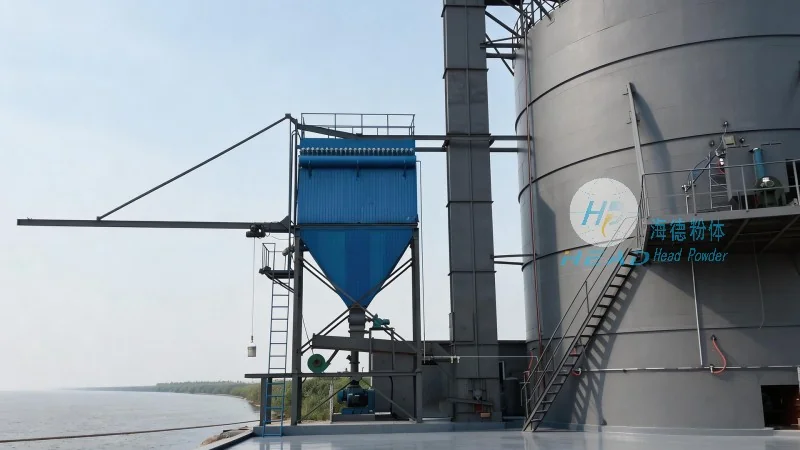
Another critical characteristic is the system's adaptability to varying production volumes and operational conditions. Modern material handling solutions from HeadPowder are designed with modular components that can be easily adjusted or expanded to meet changing production needs. This flexibility allows industries to scale their operations without significant downtime or capital investment.
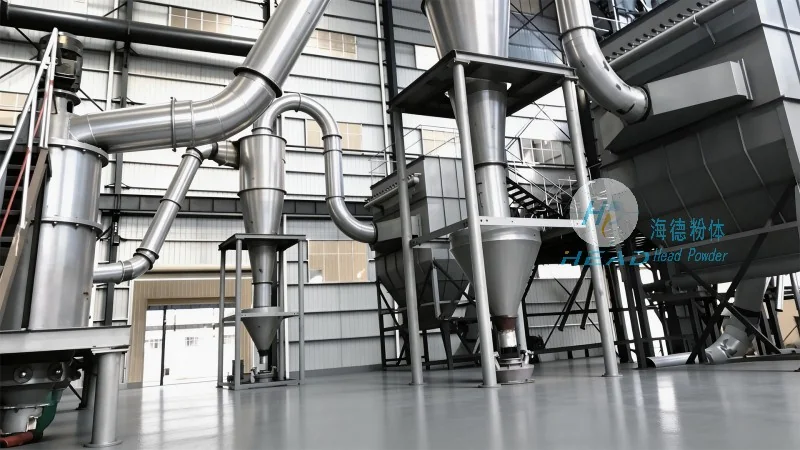
Environmental considerations also play a significant role in the design of these systems. Advanced dust control measures, such as enclosed conveyor systems and filtration units, are incorporated to minimize air pollution and comply with environmental regulations. Additionally, energy-efficient motors and optimized system designs reduce operational costs while maintaining high performance standards.
Conclusion
HeadPowder's expertise in developing and implementing potassium carbonate fertilizer material handling systems highlights the importance of understanding both the technical principles and practical characteristics of such equipment. By leveraging advanced technology and robust engineering, these systems ensure efficient material transport, enhance operational safety, and support sustainable agricultural practices. For industries seeking reliable and efficient fertilizer handling solutions, HeadPowder offers tailored systems that meet the highest standards of performance and durability.




