When it comes to efficiently transporting sodium bicarbonate, specialized systems are essential for maintaining product integrity and operational efficiency. This article explores the working principles and key features of such systems, highlighting how they contribute to smooth industrial processes. The proper handling of sodium bicarbonate is critical in industries like food processing, pharmaceuticals, and chemical manufacturing, where product purity and consistency are paramount. A well-designed material handling system ensures that the material is moved without degradation, contamination, or loss, thereby supporting overall production goals.
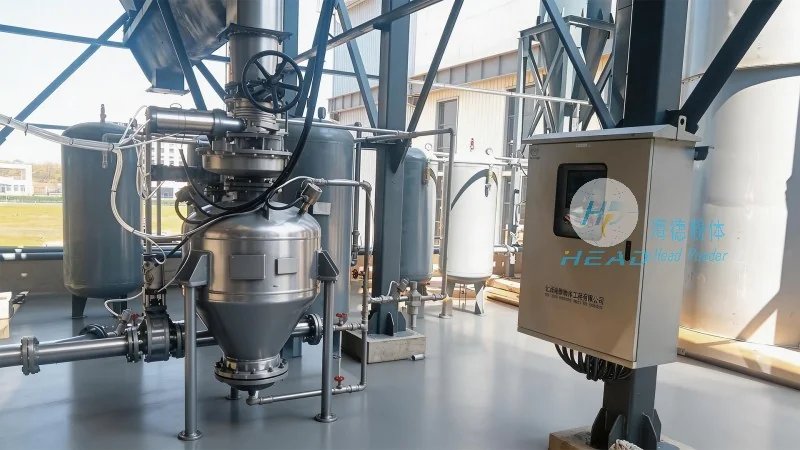
Working Principle of the Material Handling System
The core of a sodium bicarbonate material handling system lies in its ability to transport bulk material from one location to another with precision and reliability. Typically, these systems incorporate components like conveyors, hoppers, and control mechanisms to ensure seamless material flow. The process begins with material storage in a hopper, where it is then fed into the conveyor system. Through the use of gravity or mechanical power, the material is moved along the conveyor path, often with adjustable speed and direction controls to match production requirements. This systematic approach minimizes material handling errors and ensures consistent delivery to processing or packaging stages. The system may also include sensors and alarms to detect blockages or overflows, providing immediate feedback to operators and preventing potential disruptions.
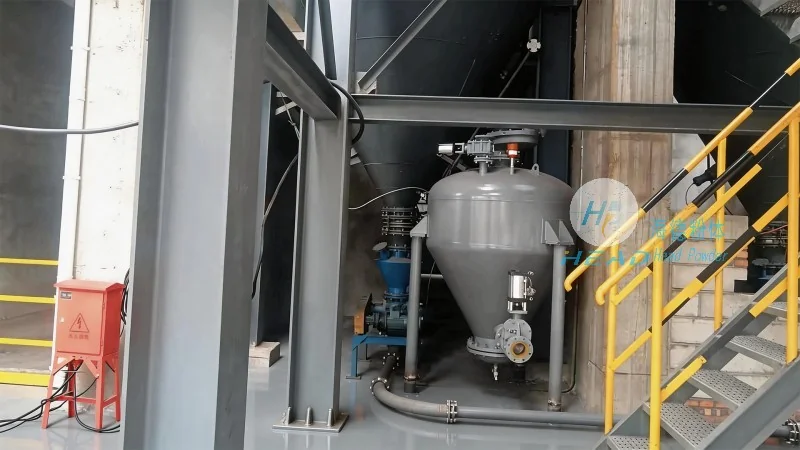
Key Features of the System
Several distinctive features define the effectiveness of sodium bicarbonate material handling systems. First, the system is designed with corrosion-resistant materials to withstand the chemical properties of sodium bicarbonate, ensuring long-term durability and safety. This is particularly important as sodium bicarbonate can be abrasive and reactive under certain conditions. Second, it incorporates dust control measures, such as sealed hoppers and enclosed conveyors, to prevent contamination and protect the environment. These features help maintain product quality and comply with environmental regulations. Third, the system offers modular design options, allowing for easy integration with existing production lines and scalability as business needs evolve. This flexibility enables companies to adapt their material handling solutions to changing production volumes or product types without significant capital investment. Additionally, advanced control systems enable real-time monitoring and adjustment, enhancing operational flexibility and reducing downtime. Operators can access data on material flow rates, system performance, and maintenance alerts through user-friendly interfaces, facilitating proactive management and troubleshooting.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field, specializes in developing and supplying high-quality material handling solutions tailored to the needs of various industries. With a strong commitment to innovation and customer satisfaction, the company has established itself as a trusted partner for businesses requiring reliable sodium bicarbonate transport systems. HeadPowder's products are engineered to meet stringent industry standards, ensuring compliance with safety and performance requirements. The company's research and development team continuously works on improving system efficiency and durability, incorporating feedback from clients to refine their offerings. This dedication to quality and customer-centric approach has earned HeadPowder a reputation for excellence in the industry.
Location and Accessibility
HeadPowder Engineering Co., Ltd. is headquartered in Shandong, China, providing a strategic base for serving both domestic and international markets. The company's location in Shandong allows for efficient logistics and supply chain management, enabling timely delivery of products to clients worldwide. This proximity to major industrial hubs also facilitates collaboration with local suppliers and partners, enhancing the overall operational efficiency of the business. The company operates a state-of-the-art manufacturing facility equipped with advanced machinery and quality control processes, ensuring that every product meets the highest standards. Additionally, HeadPowder maintains a strong presence in international markets through partnerships and distribution networks, making their systems accessible to clients across the globe.




