Cotton seed material handling equipment is a specialized system designed to efficiently transport, process, and manage cotton seed from the harvesting stage to storage or further processing. The equipment plays a crucial role in optimizing the workflow in cotton processing facilities, ensuring that cotton seeds are handled with minimal loss and maximum efficiency. This article will explore the working principle and key features of such equipment, providing insights into how these systems enhance operational performance.
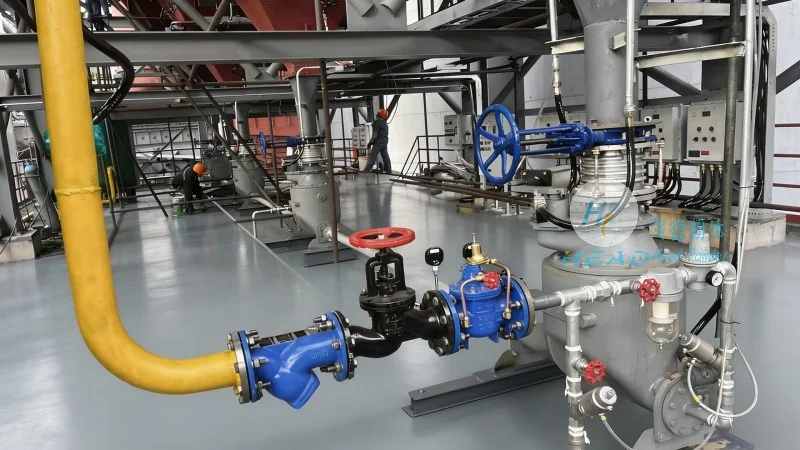
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of industrial material handling equipment. With a strong presence in China, particularly in Shandong province, the company specializes in developing customized solutions for various industries, including agriculture and food processing. HeadPowder's commitment to quality and innovation has made it a trusted partner for businesses seeking reliable and efficient equipment for cotton seed handling. The company's facilities are equipped with advanced technology and skilled professionals who ensure that each product meets the highest standards of performance and durability.
Working Principle of Cotton Seed Material Handling Equipment
The working principle of cotton seed material handling equipment typically involves a combination of mechanical components and control systems that work in tandem to move cotton seeds through different stages of processing. The core components include feed mechanisms, conveyor systems, separation units, and storage containers. The process begins with the intake of raw cotton seeds, which are then fed into the equipment via a hopper or feeding chute. The feed mechanism ensures a consistent flow of seeds into the conveyor system, which may consist of belt conveyors, screw conveyors, or pneumatic conveyors, depending on the specific design and application requirements.
Once the cotton seeds enter the conveyor system, they are transported to the next processing stage. The conveyor may be equipped with adjustable speed controls to regulate the flow rate, ensuring that the seeds move at an optimal pace for subsequent operations. In some systems, the conveyor may also include cleaning or sorting mechanisms to remove impurities or damaged seeds. After the initial transport, the cotton seeds may pass through a separation unit, such as a screen or a separator, which separates them from other materials like leaves, stems, or debris. This step is crucial for maintaining the quality of the final product and reducing waste.
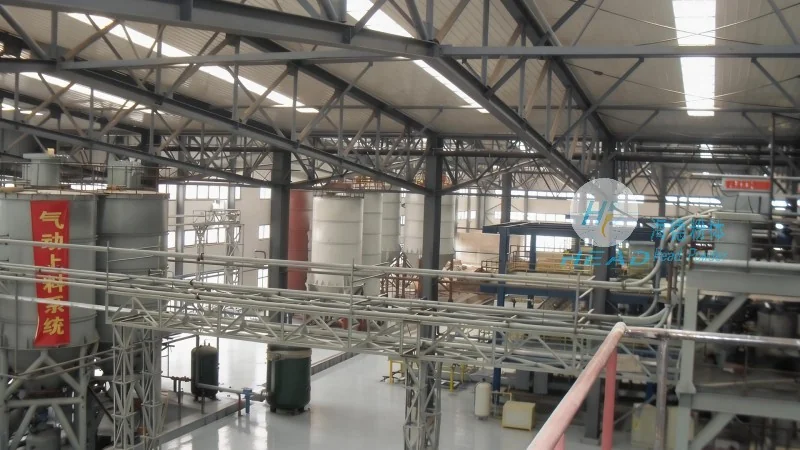
The separated cotton seeds are then directed to a storage or processing container. The equipment may include a storage silo or a hopper that holds the seeds until they are ready for further processing, such as oil extraction or packaging. The control system, often integrated with sensors and automation technology, monitors the entire process, adjusting parameters as needed to maintain efficiency and consistency. This automated approach minimizes human intervention, reduces operational errors, and enhances overall productivity.
Key Features of Cotton Seed Material Handling Equipment
HeadPowder's cotton seed material handling equipment is designed with several key features that set it apart from conventional solutions. One of the primary features is its high efficiency, which is achieved through optimized conveyor designs and precise control systems. The equipment can handle large volumes of cotton seeds with minimal energy consumption, making it cost-effective for long-term operation. Another important feature is its durability and reliability, built to withstand the harsh conditions of industrial environments and the abrasive nature of cotton seeds.
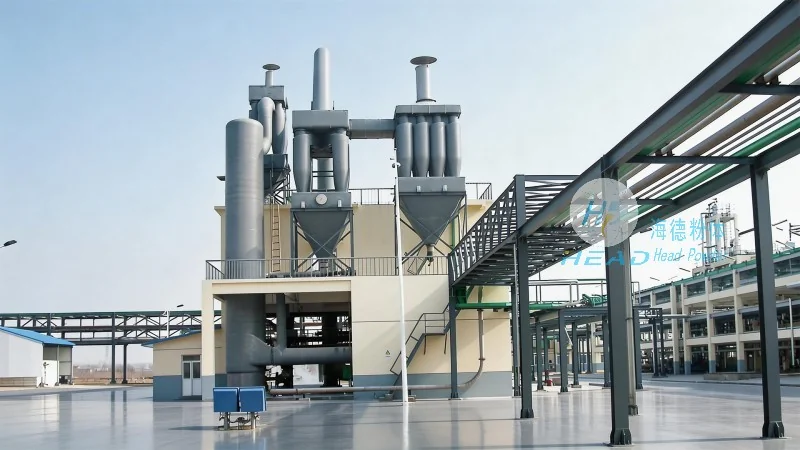
The equipment also offers versatility, allowing it to be adapted to different processing requirements. For instance, it can be customized with various conveyor types, such as belt or screw conveyors, to suit specific operational needs. Additionally, the system may include adjustable components, such as variable speed drives or adjustable hoppers, enabling operators to fine-tune the equipment for optimal performance. This adaptability makes the equipment suitable for a wide range of applications, from small-scale farms to large industrial processing plants.
Another notable feature is the integration of advanced monitoring and control technology. The equipment is equipped with sensors that track parameters like flow rate, temperature, and material level, providing real-time data to operators. This data can be used to optimize the process, detect potential issues early, and prevent downtime. The automation capabilities also enhance safety by reducing the need for manual handling of heavy or potentially hazardous materials, minimizing the risk of accidents in the workplace.
Conclusion
Cotton seed material handling equipment, as exemplified by the solutions from Shandong HeadPowder Engineering Co., Ltd., represents a critical component in modern cotton processing operations. By understanding the working principle and leveraging the key features of such equipment, businesses can enhance their operational efficiency, reduce costs, and improve the quality of their cotton seed products. The combination of advanced technology, robust design, and customization options makes these systems essential for any facility looking to streamline its cotton seed handling processes and achieve sustainable growth.




