Urea granule material handling equipment is a specialized system designed for the efficient transport and handling of urea granules, a key fertilizer product. This equipment plays a crucial role in modern agricultural and industrial applications, ensuring the safe and reliable movement of urea granules from production sites to storage facilities or distribution centers. The design and functionality of such equipment are tailored to meet the specific requirements of urea granule characteristics, including their size, density, and flow properties.
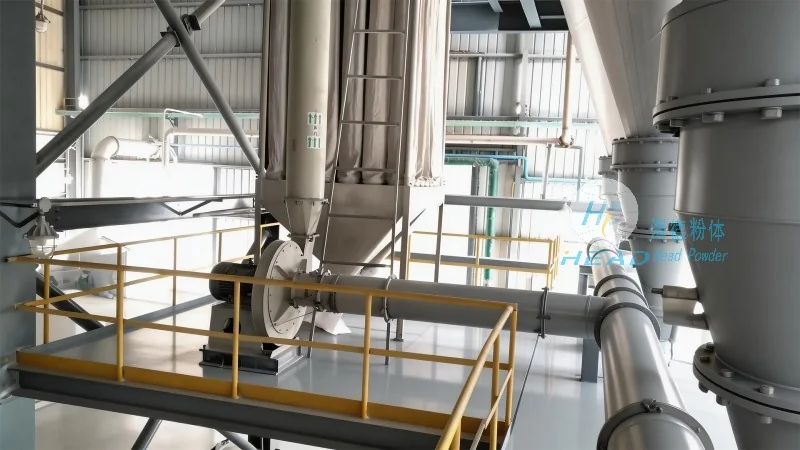
Working Principle of Urea Granule Material Handling Equipment
The working principle of urea granule material handling equipment typically involves several key components and operational steps. The system generally starts with the loading of urea granules into a hopper or storage silo. From there, the granules are conveyed through a series of mechanisms such as screw conveyors, belt conveyors, or pneumatic systems. Screw conveyors are commonly used for horizontal or slight incline transport due to their ability to handle granular materials without the need for additional power for lifting. Belt conveyors, on the other hand, are suitable for longer distances and can handle larger volumes of urea granules. Pneumatic systems, utilizing air pressure to move granules through pipes, offer flexibility in layout but require careful management of air pressure and material flow to prevent blockages or degradation of the granules.
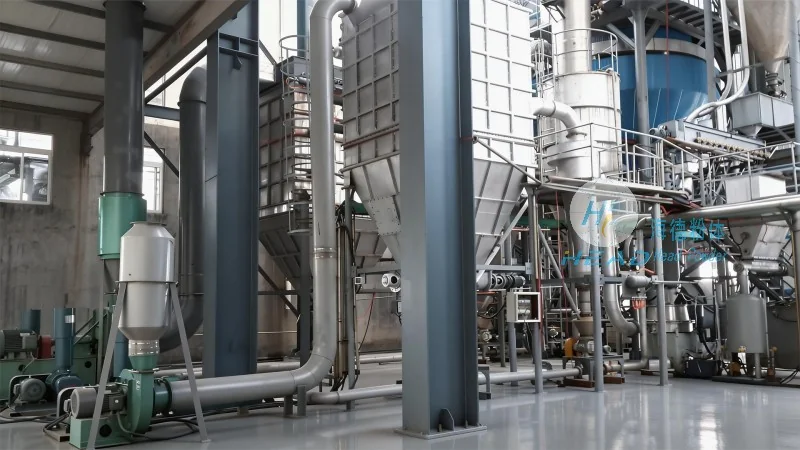
Key Features of Urea Granule Material Handling Equipment
Urea granule material handling equipment is characterized by several important features that enhance its performance and reliability. One of the primary features is its robust construction, designed to withstand the abrasive nature of urea granules and the potential for wear and tear over time. The equipment often incorporates materials such as stainless steel or high-grade alloys in critical components to ensure durability and longevity. Another key feature is the system's ability to maintain the integrity of the urea granules during transport. This includes minimizing breakage, preventing segregation, and avoiding contamination. Advanced control systems are integrated into many modern urea granule handling systems to monitor and regulate the flow rate, pressure, and temperature, ensuring optimal operation and protecting the granules from damage. Additionally, the equipment is designed for easy maintenance and cleaning, with features like removable parts and access panels that facilitate regular upkeep and prevent the buildup of urea residue, which can affect performance and safety.
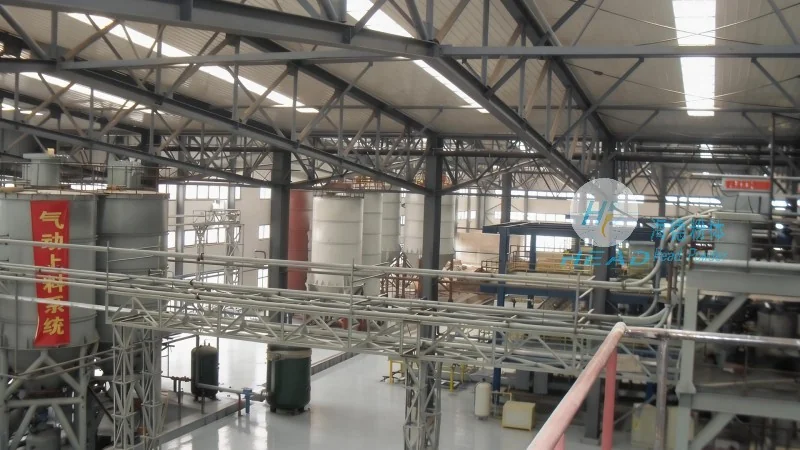
Applications and Benefits in Industrial and Agricultural Settings
Urea granule material handling equipment is widely used in both industrial and agricultural sectors. In industrial settings, it is employed in fertilizer production plants, where urea granules are processed and transported between various stages of production, such as granulation, drying, and packaging. The equipment ensures a continuous and efficient flow of materials, reducing downtime and increasing overall production efficiency. In agricultural settings, the equipment is used to transport urea granules from storage facilities to farms or distribution points, facilitating the timely application of fertilizers to crops. The benefits of using specialized urea granule handling equipment include improved safety, as the systems are designed to prevent dust emissions and minimize the risk of accidents. They also contribute to cost savings by reducing material loss and improving operational efficiency. Furthermore, the equipment helps maintain the quality of urea granules, ensuring that they remain in optimal condition for their intended use, which is critical for agricultural productivity.
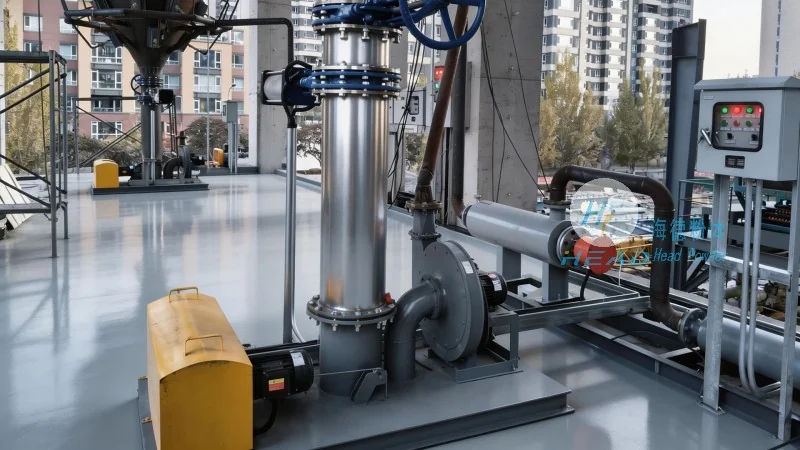
Customization and Integration with Other Systems
Shandong HeadPowder Engineering Co., Ltd. offers customized solutions for urea granule material handling equipment to meet the specific needs of different clients. The company, based in Shandong, China, specializes in designing and manufacturing equipment tailored to the unique requirements of urea granule handling, including different sizes, capacities, and operational conditions. The equipment can be integrated with other systems, such as storage silos, packaging lines, and quality control systems, to form a comprehensive material handling solution. This integration ensures seamless operation from raw material storage to final product delivery, enhancing overall system efficiency. Customization options may include adjustments to conveyor speed, hopper capacity, and control system features to optimize performance for specific applications. The company's expertise in urea granule handling technology allows for the development of equipment that meets both current and future operational needs, providing long-term value to clients.




