For manufacturers dealing with chicken essence powder, efficient and reliable material handling is crucial to maintaining production efficiency and product quality. Pneumatic conveying equipment has emerged as a preferred solution for transporting fine powders like chicken essence, offering a range of benefits that traditional methods may not provide. This article explores the working principle and key features of such systems, highlighting how they enhance operational performance in the food processing industry.
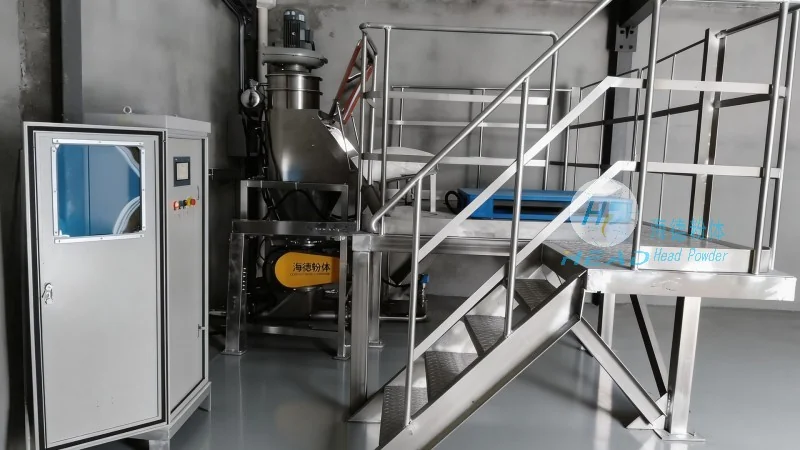
About HeadPowder: A Leader in Powder Handling Solutions
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a renowned manufacturer specializing in the design, development, and supply of advanced powder handling equipment. With a focus on precision engineering and customer-centric solutions, the company has established itself as a trusted partner for businesses in the food, pharmaceutical, and chemical sectors. HeadPowder’s expertise lies in creating customized pneumatic conveying systems that meet the unique demands of each application, ensuring optimal performance and durability. The company’s facilities are located in Shandong, China, where state-of-the-art technology and rigorous quality control processes are employed to deliver high-quality products to global markets.
The Working Principle of Pneumatic Conveying Equipment
Pneumatic conveying systems for chicken essence powder operate by using air or gas to transport the material from one location to another. The core principle involves creating a pressure differential that propels the powder through a network of pipes and components. There are two primary types of pneumatic conveying systems: positive pressure and negative pressure (or vacuum) systems. Positive pressure systems generate air pressure above atmospheric levels to push the powder forward, while negative pressure systems create a vacuum to draw the material into the system. For chicken essence powder, which is typically fine and abrasive, positive pressure systems are often preferred due to their ability to handle high volumes and maintain consistent flow rates.
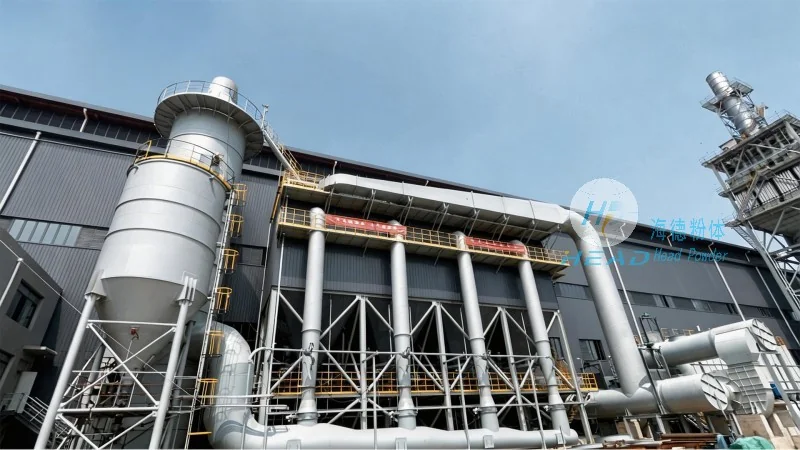
The system typically consists of several key components, including a hopper for material storage, a conveyor line (such as a pipeline), a blower or compressor to generate airflow, and a control system to regulate the conveying process. The hopper ensures a steady supply of chicken essence powder, while the conveyor line provides the path for the material to travel. The blower or compressor generates the necessary air pressure, and the control system monitors and adjusts the flow rate based on real-time conditions. This integrated approach ensures that the powder is transported efficiently and safely, minimizing the risk of product degradation or contamination.
Key Features of Chicken Essence Powder Pneumatic Conveying Equipment
When evaluating pneumatic conveying systems for chicken essence powder, several key features stand out as critical for optimal performance. First, the system must be designed to handle fine, cohesive powders without clogging or blockages. This is achieved through the use of specialized components such as rotary valves, airlocks, and flexible hoses that prevent material buildup and ensure smooth flow. Second, the equipment should offer high efficiency and low energy consumption. Modern systems utilize energy-efficient blowers and optimized pipe designs to minimize power usage while maintaining the required conveying capacity. Third, safety is a paramount concern, especially when handling food-grade materials like chicken essence. The system must be equipped with features such as explosion-proof blower motors, dust collection systems, and emergency shut-off valves to prevent accidents and protect personnel and equipment.
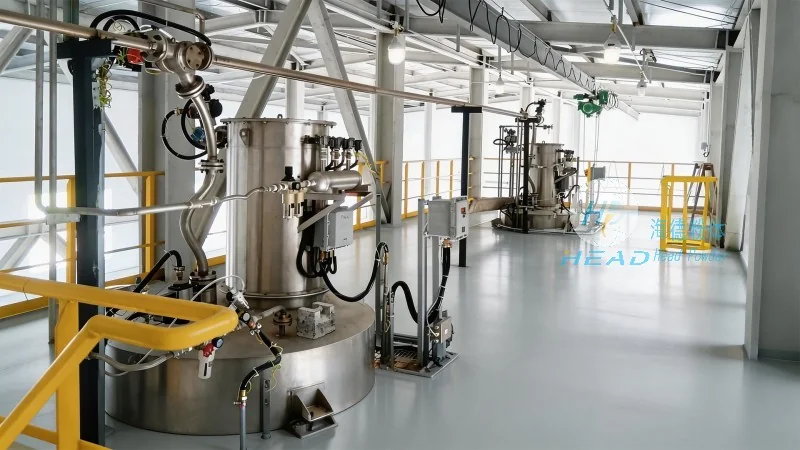
Another important feature is the system’s ability to handle varying particle sizes and moisture content. Chicken essence powder can vary in consistency, and the conveying equipment must be adaptable to these changes. This flexibility is achieved through adjustable air pressure settings and variable speed blowers, allowing operators to customize the system to the specific characteristics of the powder. Additionally, the equipment should be easy to clean and maintain, with removable components that can be sanitized to meet food safety regulations. This ensures that the system remains hygienic and compliant with industry standards, reducing the risk of cross-contamination and product recalls.
Conclusion: Enhancing Efficiency with Pneumatic Conveying Technology
Pneumatic conveying equipment for chicken essence powder represents a significant advancement in material handling technology, offering manufacturers a reliable and efficient solution for transporting fine powders. By understanding the working principle and key features of these systems, businesses can make informed decisions about implementing the right equipment for their operations. HeadPowder, with its expertise and commitment to quality, provides customized pneumatic conveying solutions that address the unique challenges of chicken essence powder handling. By investing in such technology, manufacturers can improve production efficiency, reduce labor costs, and enhance product quality, ultimately gaining a competitive edge in the market.




