Rare earth materials are critical components in modern industrial applications, including electronics, aerospace, and renewable energy technologies. The efficient handling and transportation of these materials are essential for maintaining production efficiency and product quality. Pneumatic conveying systems offer a reliable solution for moving rare earth powders and granules, providing a dust-free, closed-loop operation that minimizes material loss and contamination. This article explores the working principle and key features of rare earth material pneumatic conveying equipment, highlighting how it addresses the unique challenges associated with handling these valuable resources.
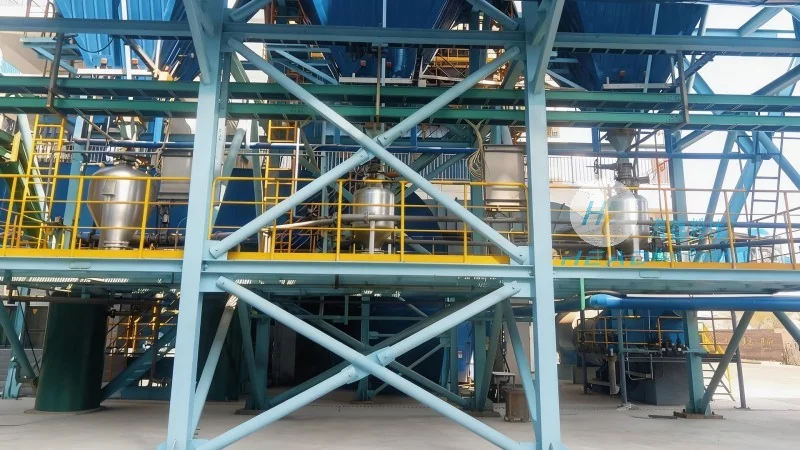
Working Principle of Rare Earth Material Pneumatic Conveying Systems
The core mechanism of a rare earth material pneumatic conveying system involves the use of air or gas to transport solid particles through a pipeline. The process typically operates under pressure, utilizing either positive or negative pressure systems. In a positive pressure system, air is forced through the conveying line, carrying the rare earth material from the source to the destination. Conversely, negative pressure systems draw air and material into the system using a vacuum. The equipment includes a hopper for material storage, a feeder to control the flow rate, a conveying line, and a receiver for the discharged material. The feeder, often a rotary valve or a screw feeder, ensures a consistent flow of rare earth material into the system. The conveying line may include components such as bends, filters, and pressure regulators to maintain optimal performance. The receiver collects the material and can be equipped with a dust collection system to prevent environmental contamination. The entire process is controlled by a system of valves, sensors, and a control panel that monitors pressure, flow rate, and material level, ensuring smooth and efficient operation.
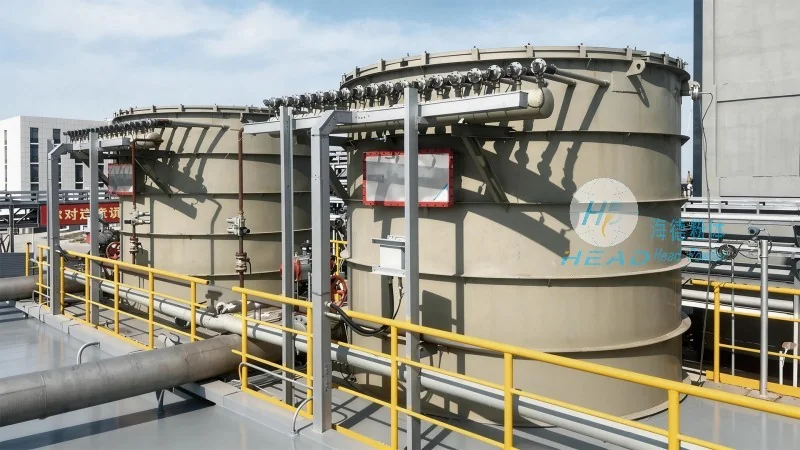
Key Features of Rare Earth Material Pneumatic Conveying Equipment
When selecting pneumatic conveying equipment for rare earth materials, several key features are crucial for optimal performance and reliability. First, the system must be designed to handle the specific physical properties of rare earth powders, such as particle size, density, and moisture content. The equipment should provide a low-pressure drop to minimize energy consumption and prevent material degradation. The use of high-quality materials, such as stainless steel or special alloys, is essential to resist corrosion and ensure durability, especially when dealing with acidic or alkaline rare earth compounds. Another important feature is the ability to maintain a closed-loop operation, which reduces dust emissions and environmental impact. The system should also include features for easy maintenance, such as quick-release fittings and accessible components. Additionally, advanced control systems allow for real-time monitoring and adjustment of the conveying process, enhancing operational efficiency and reducing downtime. The equipment should be scalable, allowing for adjustments in capacity to accommodate varying production needs. Safety features, including pressure relief valves and emergency shut-off mechanisms, are also critical to ensure safe operation in industrial settings.
Application and Benefits in Rare Earth Processing
Rare earth material pneumatic conveying equipment is widely used in various stages of rare earth processing, from raw material handling to final product packaging. In the mining and extraction phase, the equipment efficiently transports raw rare earth ores from storage to processing facilities. During the beneficiation and separation processes, it moves concentrated rare earth compounds between different processing units. In the final production stage, the system delivers finished rare earth products to packaging and shipping areas. The benefits of using pneumatic conveying systems in these applications include improved material handling efficiency, reduced labor costs, and enhanced product purity. The closed-loop design minimizes material loss and contamination, which is critical for maintaining the high purity standards required for electronic and aerospace applications. Additionally, the system's ability to handle fine powders without clogging or agglomeration ensures consistent product quality. The energy efficiency of the system, particularly in positive pressure designs, reduces operational costs and environmental impact, making it a sustainable choice for rare earth processing facilities.
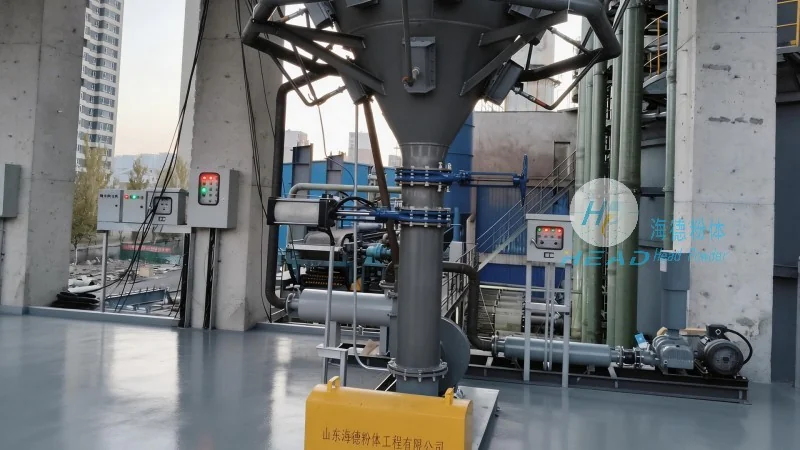
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer and supplier of advanced pneumatic conveying equipment, specializing in solutions for handling rare earth materials and other industrial powders. With a focus on innovation and quality, the company has developed state-of-the-art systems that meet the demanding requirements of modern rare earth processing industries. HeadPowder's equipment is designed to provide reliable, efficient, and safe material handling solutions, ensuring that rare earth materials are transported with minimal loss and maximum purity. The company's commitment to customer satisfaction and technical excellence has established it as a trusted partner in the rare earth processing sector. HeadPowder's facilities are located in Shandong, China, where the company leverages local expertise and resources to deliver high-quality products and services to clients worldwide.




