Cereal material pneumatic conveying equipment is a specialized system designed for the efficient and reliable transport of cereal-based products, such as flakes, granules, and other dry food ingredients. This equipment is widely used in the food processing industry, particularly in the production of breakfast cereals, where the need for gentle handling and minimal product degradation is critical. The system operates by using air as the conveying medium, which moves the cereal materials through a network of pipes and components, ensuring a smooth and controlled transfer process.
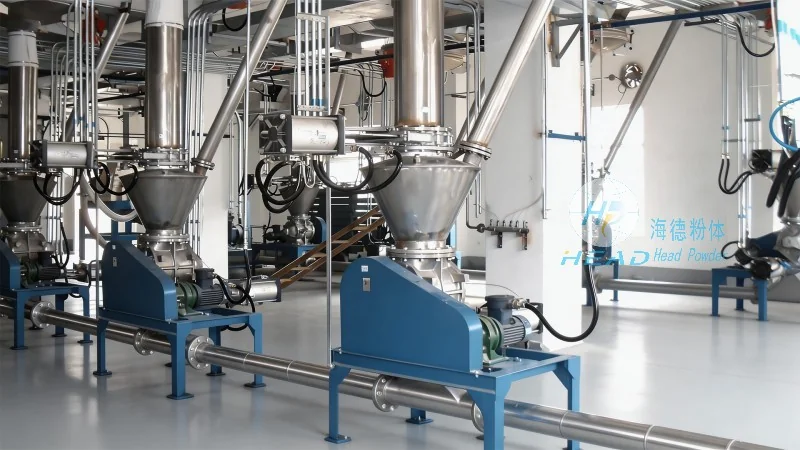
Working Principle of the Equipment
The core working principle of cereal material pneumatic conveying equipment involves the use of a positive or negative pressure system to move the material. In a positive pressure system, air is forced into the conveying line, creating a pressure differential that propels the cereal particles forward. Conversely, a negative pressure system draws air and material through the line by creating a vacuum. The equipment typically includes a hopper for material storage, a feeder to control the flow rate, a conveyor line with appropriate fittings, and a receiver for the discharged material. The process begins when the cereal material is fed into the hopper, where it is then drawn or pushed through the system by the air flow. The air velocity and pressure are carefully controlled to ensure that the material is conveyed without excessive friction or breakage, maintaining the quality of the product.
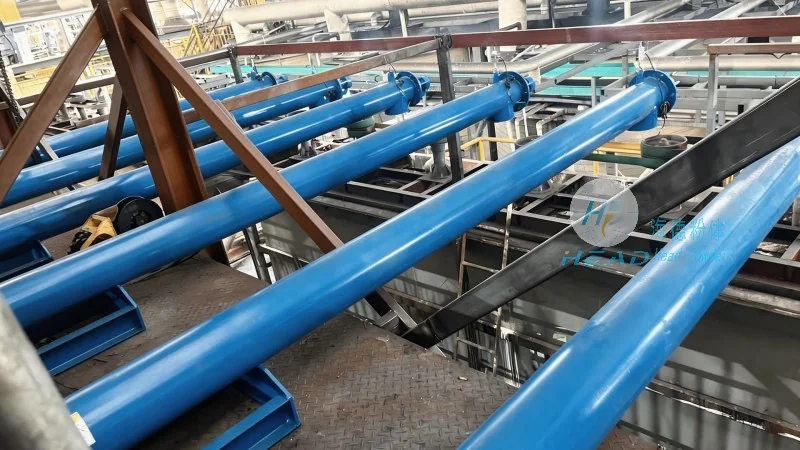
Key Features and Advantages
Several key features make cereal material pneumatic conveying equipment an ideal choice for food processing applications. Firstly, it offers a closed system, which helps to maintain product hygiene and prevent contamination from external sources. This is particularly important in the food industry, where strict quality and safety standards must be met. Secondly, the equipment provides gentle handling of the cereal materials, reducing the risk of breakage or damage to the product's texture and appearance. This is crucial for maintaining the quality of the final product, as even minor damage can affect consumer perception and product performance. Thirdly, the system is highly efficient in terms of energy consumption and operational costs. By using air as the conveying medium, the equipment minimizes the need for mechanical components, such as belts or chains, which can wear out and require frequent maintenance. Additionally, the closed system reduces the risk of dust emissions, contributing to a cleaner and safer working environment. Another advantage is the flexibility of the system, which can be easily adjusted to handle different types of cereal materials, including various sizes and shapes of flakes or granules. This adaptability makes the equipment suitable for a wide range of applications within the food processing industry.
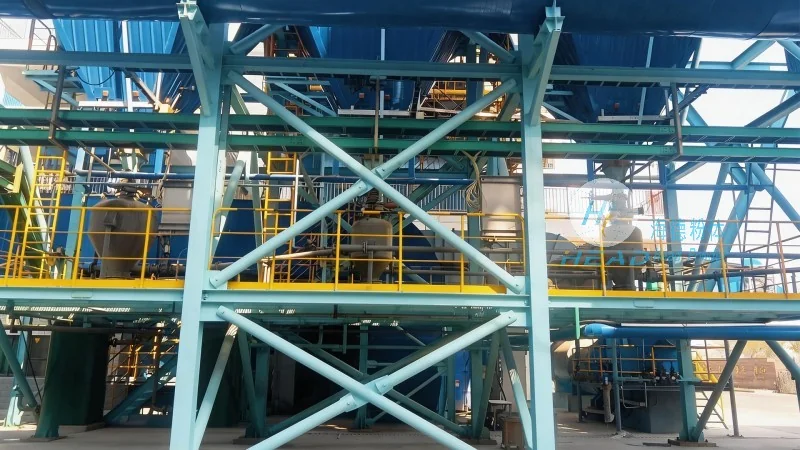
Company Information: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer and supplier of pneumatic conveying equipment, specializing in solutions tailored for the food processing sector. With a strong focus on quality and innovation, the company has established itself as a trusted partner for businesses in the cereal and food industry. The company's products are designed to meet the highest standards of hygiene and efficiency, ensuring that they comply with international food safety regulations. HeadPowder Engineering leverages advanced engineering and manufacturing techniques to produce equipment that is durable, reliable, and easy to maintain. The company's commitment to customer satisfaction is reflected in its comprehensive after-sales support, including technical assistance, maintenance services, and customized solutions to meet specific operational needs.
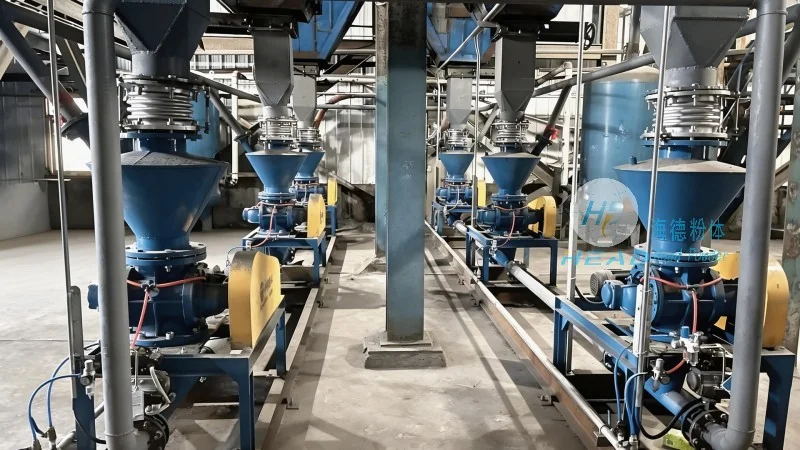
Address and Location
The company is situated in Shandong, China, providing a strategic base for serving both domestic and international markets. The address is as follows: [Address details as per the original information]




